
The customer measures the trim
A thermoformed part is formed to a shape and then trimmed to a size. The forming is often accurate to a millimetre, and the trimming is what the customer measures, because the trim is what fits into the assembly.
That makes trimming a tolerance operation rather than a finishing operation, and it means the trim method has to be chosen on tolerance and volume rather than on the machine that happens to be free.
There are four methods in common use: hand trimming with a knife or a shear, a steel rule die on a press, a CNC router on a fixture, and a matched trim punch. They span a factor of six in tolerance and a factor of two in cost per part, and the right choice changes with volume.
Tolerance by method
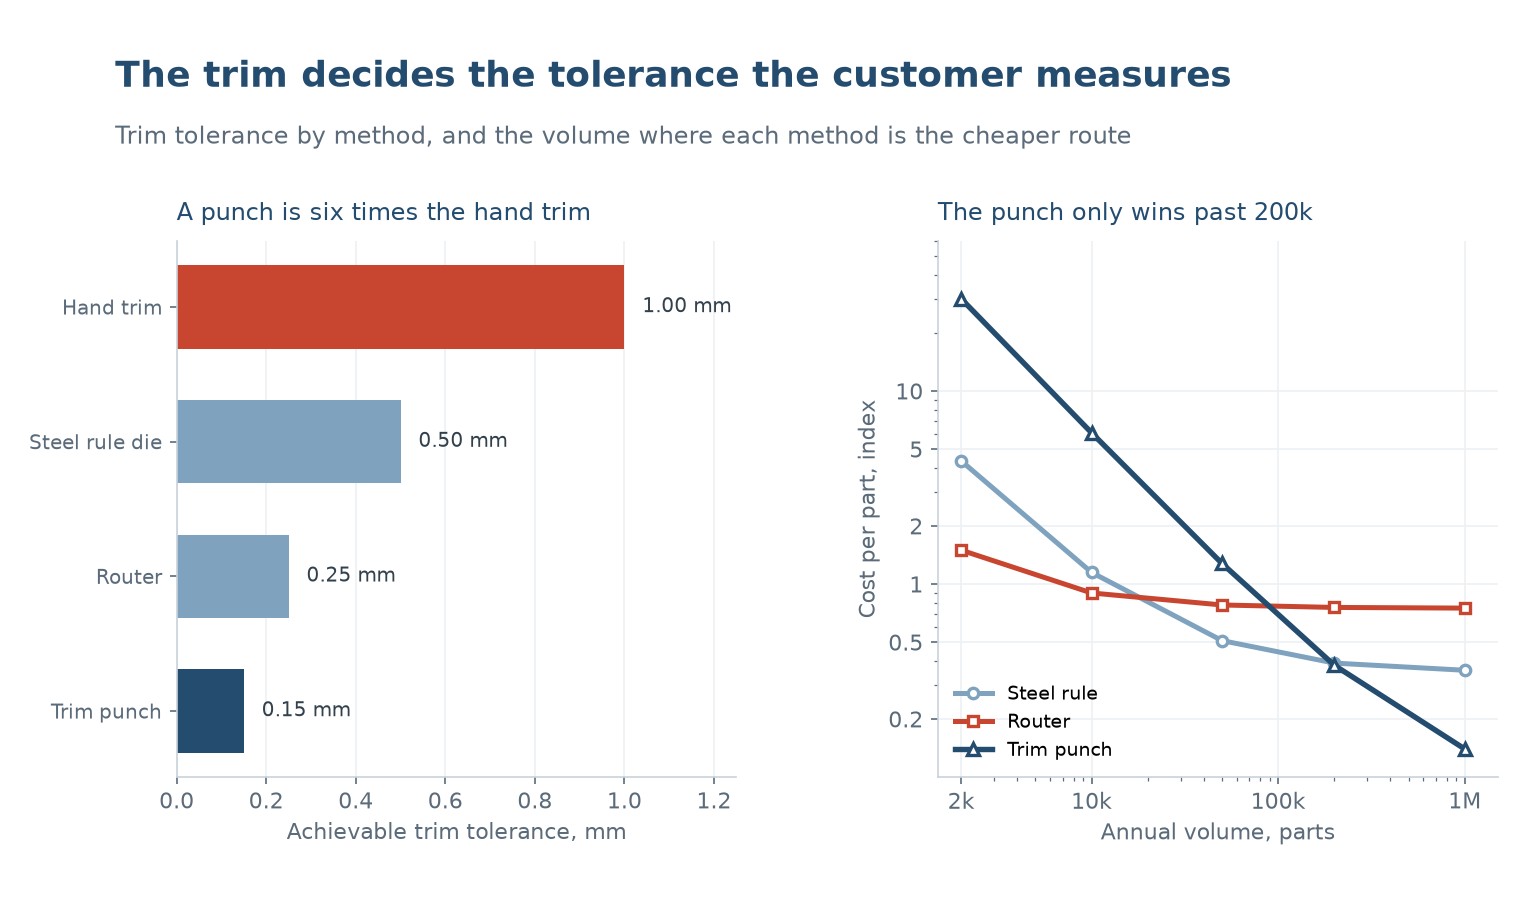
Hand trimming holds about 1.00 mm on a straight edge and rather worse on a curve. A steel rule die holds 0.50 mm, a router 0.25 and a trim punch 0.15.
The differences come from how the part is located. Hand trimming locates by eye against a line. A steel rule die locates on the part's own form, so the trim follows the forming. A router locates on a fixture, so the trim follows the fixture. A punch locates and cuts in one motion, so there is no opportunity for the part to move between location and cut.
The tolerance also depends on the part. A shallow, stiff part trims consistently by any method; a deep, flexible part deflects under the cutting force, and the trim wanders. On a deep draw, the punch is often the only method that holds 0.15 mm because it cuts before the part can move.
| 方法 | Tolerance | Setup | Best volume |
|---|---|---|---|
| Hand trim | +/- 1.00 mm | None | Under 100 parts |
| Steel rule die | +/- 0.50 mm | A die, a few days | 500 to 30,000 |
| CNC router | +/- 0.25 mm | A fixture, a day | 100 to 50,000 |
| Trim punch | +/- 0.15 mm | A matched tool, weeks | Over 200,000 |
Table 1 — Trim tolerance, setup and the volume each method suits.
Where the cost curves cross
The economics are a tool cost divided by volume plus a piece cost. A steel rule die costs a few thousand and has a moderate piece cost; a router fixture costs much less and has a higher piece cost because each part is cut individually; a trim punch costs tens of thousands and has the lowest piece cost.
On a typical part the router is the cheapest route from a few hundred parts up to about 30,000 a year, the steel rule die takes over between 30,000 and 200,000, and the punch wins above 200,000. Those crossovers move with the part size and the trim length, but the order does not.
The crossover is worth calculating rather than guessing, because the answer is often counter-intuitive. A shop that assumes a punch is always cheapest for high volume can spend 40,000 on a tool for a part that runs 50,000 a year, where a router fixture would have been cheaper for the life of the product.
Fixtures and location
Every method except hand trimming needs the part to be located, and the quality of the location sets the tolerance. A router fixture that locates on the formed surface will follow every variation in the forming; one that locates on a moulded feature will not.
The best location is a feature that is formed accurately and is not affected by the trim. A moulded step, a rib or a pair of bosses are all better than an edge, because an edge is what the previous operation produced and its tolerance accumulates.
Vacuum fixturing is common on routers because it holds a thin part flat without clamping marks. It only works if the part is stiff enough not to deflect into the vacuum holes, and on a 0.8 mm part that is often not the case.
The trimmed edge
A trimmed edge is a cut through the sheet, and its quality depends on the method. A steel rule die leaves a slightly angled edge with a small witness from the rule. A router leaves a clean vertical edge with a burr on the exit side. A punch leaves the cleanest edge, with a shear zone and a small break.
| 方法 | Edge angle | Burr | 終了 |
|---|---|---|---|
| Hand trim | 可変 | Heavy | Rough, needs deburring |
| Steel rule die | 2 to 5 degrees | Light | Slight witness from the rule |
| Router | Square | On the exit side | Clean, deburr the exit |
| Trim punch | Square with a break | Minimal | Cleanest, shear zone visible |
Table 2 — What each trim method leaves on the edge.
The edge also matters structurally. A trimmed edge on a formed part is where the wall is thinnest and where a crack will start, so a ragged edge is a fatigue site. On a part that will flex in service, the trim quality is a durability issue rather than a cosmetic one.
Deburring is often skipped and rarely acceptable. A 0.1 mm burr on a visible edge is felt before it is seen, and on a part that slides into a groove it prevents assembly. The deburring step has to be in the process, not in the hope.
What to specify
A trimmed part is specified by the trim line and its tolerance, and by the features that locate it.
- Trim line dimensions with a bilateral tolerance, referenced to a datum, not to an edge.
- The datum feature, which should be a formed feature rather than the trim itself.
- Edge quality: burr limit and whether deburring is included.
- Whether the trim is in the plane of the flange or on a curved surface.
- The annual volume, which decides the method and the tooling cost.
- Packing, because a trimmed part with a sharp edge needs protection.
The datum is the item that causes the most argument. A drawing that dimensions from the trim edge to the trim edge has no datum at all, and two suppliers will produce parts that are individually correct and will not assemble together.
What tolerance can thermoformed parts be trimmed to?
About 1.00 mm by hand, 0.50 with a steel rule die, 0.25 on a router and 0.15 with a trim punch.
Which trimming method is cheapest?
It depends on volume. A router is cheapest up to about 30,000 parts a year, a steel rule die from 30,000 to 200,000, and a punch above that.
Why does the trim tolerance matter more than the forming tolerance?
Because the trim is what fits into the assembly. The customer measures the trimmed size, so the trim is the tolerance that governs.
What should a trim fixture locate on?
A formed feature such as a step, a rib or a boss, not the edge. Locating on the edge stacks the tolerance of the previous operation onto the trim.
Does a trimmed edge need deburring?
Usually yes. A burr is felt before it is seen, it prevents assembly into a groove, and on a flexing part it is a crack initiation site.
Can a router trim a deep drawn part?
It can, but the part deflects under the cutting force and the tolerance suffers. A punch is better for deep parts because it cuts before the part can move.
Trimming a formed part to a tolerance?
Send the part, the trim line and the annual volume. We will quote the method that holds the tolerance at the lowest cost per part, tooling included.
Continue reading
- Demoulding: Draft, Ejection and the Part That Sticks at Temperature
- Cooling in Thermoforming: The Half of the Cycle That Sets the Shape
- Thermoforming Tolerances: What a Formed Part Can Hold
- Vacuum Versus Pressure Forming: Detail, Cost and the Tool Each Needs
- Custom Vacuum Forming: Tooling, Materials and Tolerances




 JA
 EN
 ES
 FR
 DE
 PT
 AR
 RU
 KO
 IT
 NL
 TR
 PL
 ID
