
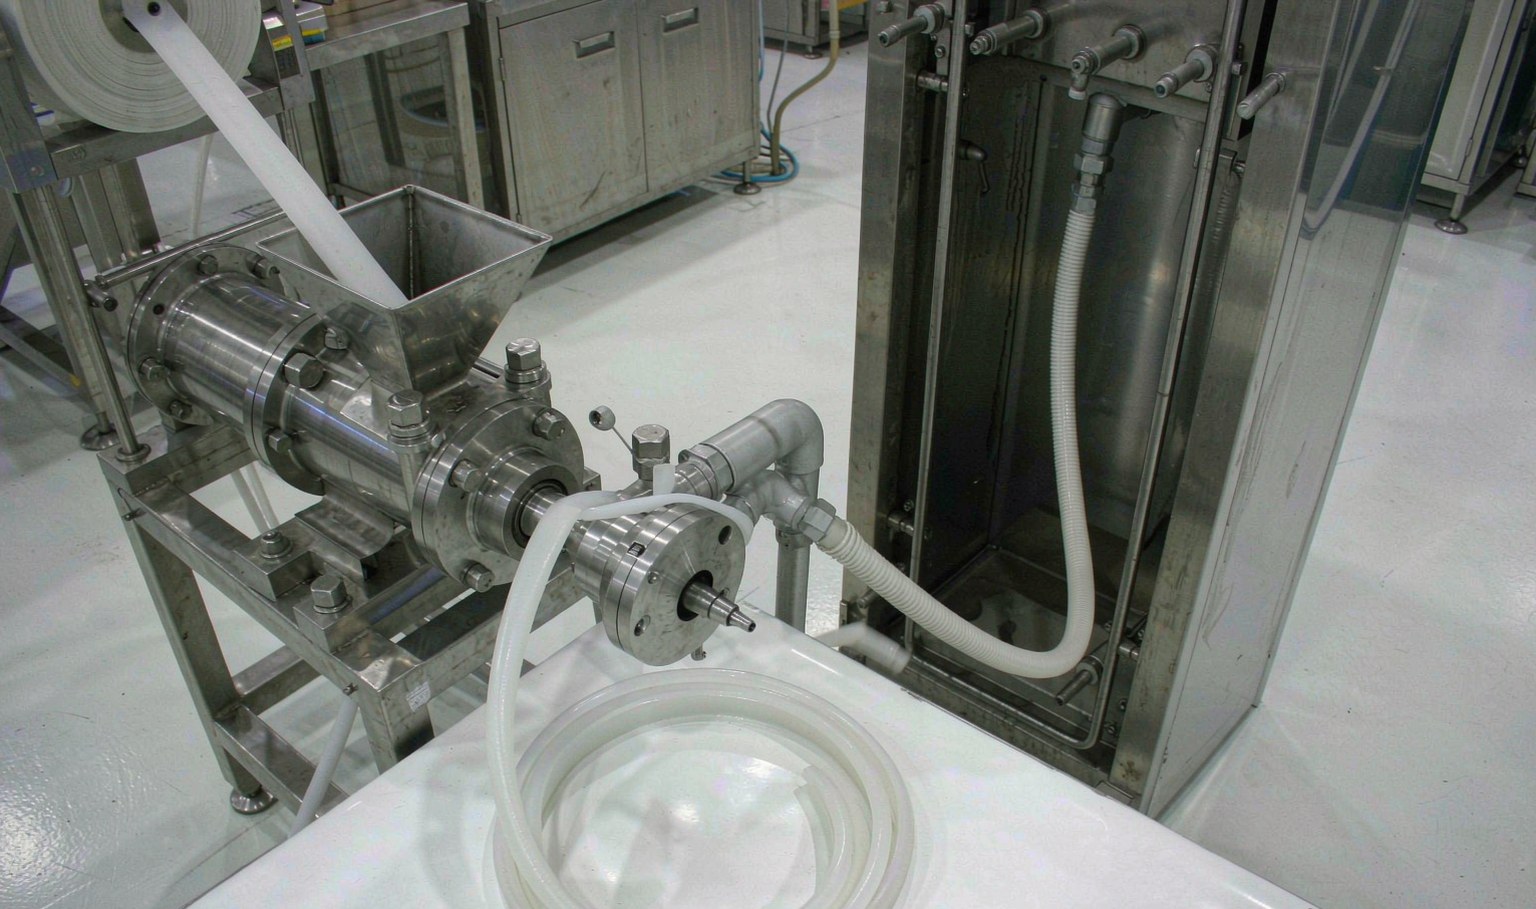
- 1. A thermoset through an extruder-shaped machine
- 2. The two material forms, and which one makes tube
- 3. The line, from strip to spool
- 4. Curing: hot air, salt bath or continuous
- 5. Tolerance, shrinkage and post-cure drift
- 6. Defects, and what causes them
- 7. Grades, certification and what to ask for
A thermoset through an extruder-shaped machine
Silicone tube is made on equipment that looks like a plastics line and is operated on completely different principles. The reason is that silicone rubber is a thermoset. It does not melt, it does not solidify by cooling, and it does not tolerate being held hot.
A thermoplastic extruder works by melting the polymer and pushing the melt through a die, then cooling it back to solid. A silicone extruder works by pushing a cold, already-compounded rubber through a die at a temperature low enough that nothing happens, and then curing it downstream in a separate oven. The barrel is water-cooled to around 20 to 30 °C. The screw is short and shallow. The compression ratio is close to 1.
Everything that follows from that inversion is what makes silicone tube a different trade from PVC or PE tube, and it is why a plastics extruder operator needs a different set of instincts to run one.
| 속성 | Silicone rubber | Thermoplastic (PVC, PE) |
|---|---|---|
| Behaviour on heating | Cures, cannot be re-melted | Melts, fully reversible |
| Barrel temperature | 20 – 30 °C, water cooled | 150 – 220 °C, heated |
| Screw L/D | 10 – 15 : 1 | 25 – 35 : 1 |
| Compression ratio | 1.1 – 1.4 : 1 | 2.5 – 4 : 1 |
| Where solidification happens | Downstream oven, 200 – 250 °C | Water tank, 10 – 20 °C |
| Scrap | Cannot be re-melted; limited regrind use | Fully recyclable |
| Dimensional control | Cure shrinkage plus post-cure drift | Cooling shrinkage only |
Table 1 — Why a silicone line is not a plastics line. The screw geometry and the temperature direction are both reversed.
The compression ratio point deserves emphasis because it is counter-intuitive. A plastics screw compresses the material 3:1 along its length to generate shear heating and to compact the melt. A silicone screw is close to 1:1, because the compound is already fully mixed and because shear generates heat that will scorch it in the barrel. The screw's job is metering, not melting.
The two material forms, and which one makes tube
| Form | What it is | How it is processed | Used for tube? |
|---|---|---|---|
| HCR — high consistency rubber | Gum-like sheet or strip, Mooney 30 – 80 | Cold feed extruder, then oven cure | Yes — the standard route |
| LSR — liquid silicone rubber | Two-part liquid, 1000 – 5000 Pa·s | Metered and mixed, injected or pumped | Rarely — thin coating and moulding |
| RTV — room temperature vulcanising | Paste in a cartridge | Hand or dispensed, cures in air | No — sealing and potting only |
| F-LSR / fluorosilicone | LSR with fluorine, oil resistant | As LSR | Specialty, small bore |
Table 2 — Silicone material forms. Extruded tube is almost always HCR, because it needs green strength to hold shape before curing.
The reason tube is made from HCR rather than LSR is green strength. An extruded tube has to hold its shape between the die and the oven, unsupported, for several seconds. HCR has enough body to do that. LSR is a liquid and would simply run, which is why LSR is used for moulded parts and coatings rather than for extrusion.
HCR arrives as a compounded strip or sheet, already containing catalyst, filler, pigment and any additives. It is fed into the extruder as a continuous strip, which is why the feed arrangement matters more than it does on a plastics line — an interruption in the strip is an interruption in the tube.
The line, from strip to spool
A silicone tube line has four stages that each have to be right, and the failure modes are different at each one.
Extrusion. A cold feed extruder with a water-cooled barrel and a short, shallow screw pushes the compound through a die. The die is where the tube's dimensions are set, and because the material is elastic rather than molten, die swell is large and predictable only by trial. A silicone die is typically cut 10 to 25% smaller than the target outside diameter to compensate.
Curing. The extrudate passes into a heated tunnel. This is where the tube becomes solid, and the tunnel type is chosen by wall thickness and production rate.
Cooling and haul-off. The cured tube is cooled and pulled by a haul-off. The haul-off speed relative to the extruder output sets the wall thickness and the diameter, so it is the main dimensional control on the line.
Post-cure. An optional but often required oven cycle that removes volatiles and completes the cure. It changes the mechanical properties and it changes the dimensions, which is why it belongs in the tolerance discussion.
| 매개변수 | Typical setting | 왜 |
|---|---|---|
| Barrel temperature | 20 – 30 °C | Keep the compound from scorching |
| Die temperature | 40 – 70 °C | Low enough to be safe, high enough for a smooth surface |
| 나사 속도 | 10 – 40 rpm | Low; shear heat is the enemy |
| 다이 스웰 | 10 – 25% of die opening | Elastic recovery on exit, material dependent |
| Haul-off draw-down | 1.0 – 1.6 : 1 | Sets wall and diameter together |
| Tube concentricity | Better than 10% of wall | Die centring, checked at start-up |
Table 3 — Extrusion settings for HCR silicone tube. The barrel being colder than the die is the inversion that catches plastics operators.
Die swell is larger and less predictable in silicone than in most thermoplastics because the compound is highly elastic and its relaxation is slow. A die that produces a 10 mm tube on one compound may produce 10.8 mm on another of the same hardness, and the only reliable approach is to cut the die slightly small and adjust, or to adjust the haul-off draw-down and accept a change in wall.
Curing: hot air, salt bath or continuous
The curing method is chosen by wall thickness. Heat has to reach the centre of the wall, and silicone is a poor conductor, so thick tube needs a medium that transfers heat better than air.
| 방법 | Medium | 온도 | 최상의 대상 |
|---|---|---|---|
| Hot air vulcanisation (HAV) | Air in a tunnel | 200 – 260 °C | Thin wall, under 3 mm; simple and clean |
| Salt bath (LCM) | Molten salt eutectic | 180 – 230 °C | Thick wall; excellent heat transfer |
| Fluidised bed | Hot glass beads | 200 – 250 °C | Thick wall, clean surface |
| Infrared | Radiant heat | High surface temperature | Thin wall, fast line speeds |
| Steam (continuous) | Pressurised steam | 150 – 180 °C | Where steam is available; needs a pressure tunnel |
Table 4 — Continuous curing methods. Salt bath is the standard for thick wall because it conducts heat into the wall far faster than air.
Hot air is the cheapest and the most common, and its limitation is exactly what you would expect: air is a poor heat transfer medium, so the cure time for a 6 mm wall in an air tunnel is long enough that the tunnel has to be very long or the line has to run very slowly. A salt bath transfers heat an order of magnitude faster, and for tube above about 4 mm wall it is usually the only economic option.
The salt has to be washed off afterwards, which is a process step in itself and a source of complaints if it is done badly. Salt residue on a medical tube is a defect; the wash water has to be controlled and the rinse verified.
Cure temperature and time are set by the catalyst system, and the two systems behave very differently.
| System | Cure temperature | By-product | Post-cure | Used for |
|---|---|---|---|---|
| Platinum addition | 120 – 150 °C to initiate | None | Optional, improves properties | Medical, food, transparent |
| Peroxide (dicumyl) | 150 – 170 °C | Acetophenone, methane | Required, 200 °C for 4 h | General industrial, thick sections |
| Peroxide (2,5-dimethyl) | 160 – 180 °C | Volatile fragments | Required | Where DCP volatility is a problem |
Table 5 — Catalyst systems. Platinum leaves no by-product, which is why medical tube is platinum cured.
Platinum addition cure is a hydrosilylation reaction between vinyl groups and Si-H groups, and it produces no by-product at all. That is why platinum-cured silicone is the default for medical, pharmaceutical and food contact: there is nothing to extract. The trade-off is cost, sensitivity to catalyst poisons (sulphur, tin, some amines) and a shorter pot life once the two parts are mixed.
Peroxide cure generates volatile fragments that stay in the rubber until they are driven out. That is why a post-cure of 4 hours at 200 °C is standard: it is not completing the cure, it is removing the by-products. Skip it and the tube smells, tastes, and fails any volatiles test — and it also drifts dimensionally as the volatiles leave in service.
Tolerance, shrinkage and post-cure drift
Silicone tube tolerances are looser than thermoplastic tube, and the reason is that the material changes dimensions twice: once on cure and again on post-cure.
| Dimension | Under 10 mm | 10 – 25 mm | 25 – 50 mm |
|---|---|---|---|
| Inside diameter | ±0.15 mm | ±0.25 mm | ±0.40 mm |
| Outside diameter | ±0.15 mm | ±0.30 mm | ±0.50 mm |
| Wall thickness | ±0.10 mm | ±0.15 mm | ±0.25 mm |
| Concentricity | 10% of wall | 10% of wall | 12% of wall |
| Cut length | ±0.5 mm | ±1.0 mm | ±1.5 mm |
Table 6 — Practical tolerances for extruded silicone tube. Concentricity is the one that decides whether the tube seals.
Cure shrinkage for silicone is 2 to 4%, which is large, but it is mostly compensated by the die and by the draw-down. The problem is not the mean shrinkage, it is the variation: the same die and the same compound can give a 0.3 mm spread in outside diameter across a shift, because cure temperature, haul-off tension and compound viscosity all move.
Post-cure adds a second, smaller shift. A tube that measures 10.00 mm off the line will measure about 9.95 mm after a 4 hour post-cure, and the change is not perfectly uniform along the length. This is why a tube measured before post-cure is not the tube the customer receives, and why the tolerance has to be applied to the finished, post-cured part.
Measure after post-cure. A dimension taken off the line is an intermediate value. If the part gets a post-cure, the tolerance applies to what comes out of the oven, not what goes in.
Defects, and what causes them
| 결함 | 원인 | Fix |
|---|---|---|
| Rough or matt surface | Die too cold, or compound too stiff | Raise die temperature 5 – 10 °C |
| Bubbles or voids in the wall | Air entrained in the compound, or moisture | Vacuum-strip the feed, re-mill the compound |
| Under-cure, tacky surface | Tunnel too short or too cool for the line speed | Slow the line, raise the temperature, or both |
| Over-cure, hard and brittle | Too much heat or too long in the tunnel | Reduce temperature or increase line speed |
| Eccentric wall | Die off-centre, or a mandrel that has drifted | Re-centre the die, check the crosshead |
| Diameter drift along the length | Haul-off tension varying, or feed interruption | Check the haul-off and the strip feed |
| White bloom on the surface | Peroxide by-products not driven off | Post-cure properly |
| Split along the length | Die line, or too much draw-down | Reduce draw, polish the die land |
| Poor tear strength | Under-cure, or wrong catalyst level | Check cure, check compound |
Table 7 — Silicone tube defects. The bloom row is a post-cure failure that looks like a material failure.
Bubbles are the defect that most often gets misattributed. Silicone compound is mixed on a two-roll mill and it entrains air; the standard fix is to vacuum-strip the compound before it is formed into strip, and to feed the extruder under a slight vacuum at the throat. If bubbles appear only in thick sections, the cause is more likely trapped air that could not escape before the skin cured, which points at cure temperature rather than at mixing.
Die lines are the other common one, and they are a tooling issue rather than a process one. A scratch or a carbon deposit on the die land leaves a continuous longitudinal mark, and no amount of temperature or speed adjustment removes it. Polish the land.
Grades, certification and what to ask for
Silicone tube is bought against a certification as often as against a dimension, and the certification is what separates a commodity tube from a medical one.
| Requirement | What it covers | Ask for |
|---|---|---|
| FDA 21 CFR 177.2600 | Rubber articles for repeated food contact | Compound statement of compliance |
| USP Class VI | Biological reactivity, implant-adjacent | Test report per batch |
| ISO 10993 | Biocompatibility, part 5 cytotoxicity and others | Full test package, not a claim |
| BfR XV | German food contact recommendation | Compound certificate |
| REACH / RoHS | Restricted substances | Declaration per batch |
| Platinum cure | No peroxide by-products | Stated on the certificate, not implied |
| Post-cured | Volatiles removed | Cycle record, temperature and time |
Table 8 — Certifications for silicone tube. The last two rows are process claims that are often asserted and rarely documented.
"Platinum cured" and "post-cured" are the two claims most often made without evidence. Both are process facts that should appear on a certificate of analysis with a temperature and a time, and both change what the tube can be used for. A tube that is platinum cured but not post-cured will pass a cytotoxicity test and fail a volatiles test, and the difference only shows up when the customer runs their own validation.
Hardness is the other specification worth pinning down. Silicone tube is normally supplied between Shore A 40 and 70, and hardness affects everything: a 40 Shore A tube is soft and seals on low force, a 70 Shore A tube resists collapse under vacuum. Specifying "silicone tube" without a hardness is leaving the most important property to the supplier.
Can silicone tube be made on a normal plastic extruder?
Not sensibly. A plastics screw has a 3:1 compression ratio and a heated barrel, both of which will scorch silicone compound in the barrel. Silicone needs a short, shallow, water-cooled screw with a compression ratio close to 1.
Why is the barrel cold and the die hot?
The compound must not cure in the barrel, so the barrel is water-cooled to 20–30 °C. The die is warmer, 40–70 °C, so the extrudate has a smooth surface and enough flow to form. All the curing happens in the tunnel downstream.
How is silicone tube cured?
Continuously, in a hot air tunnel at 200–260 °C for thin wall, or a molten salt bath at 180–230 °C for thick wall. Salt conducts heat far better, which is why it is used above about 4 mm wall.
Why does my silicone tube smell?
Peroxide cure by-products that were not driven off. A 4 hour post-cure at 200 °C removes them. Platinum-cured tube has no by-products and does not have this problem.
What tolerance can extruded silicone tube hold?
About ±0.15 mm on diameter under 10 mm, ±0.30 mm from 10 to 25 mm, and ±0.50 mm above 25 mm. Concentricity of 10% of wall is the practical limit and it matters more than diameter for sealing.
Why does the diameter change after post-curing?
Post-cure drives off volatiles and completes the cure, and the part shrinks slightly as it does — around 0.05 mm on a 10 mm tube. Tolerance has to be applied to the post-cured part, not to the dimension off the line.
What is the difference between platinum and peroxide cure?
Platinum addition cure produces no by-products and is the default for medical and food contact. Peroxide cure produces volatile fragments that require a long post-cure, but it is cheaper and more tolerant of compound contamination.
Can silicone tube be sterilised repeatedly?
Yes, which is a major reason it is used in medical and pharmaceutical tubing. It withstands autoclave cycles at 121–134 °C, gamma irradiation and ethylene oxide. Repeated autoclaving does gradually reduce tear strength.
Need silicone tube to a medical or food-contact specification?
Tell us the ID, wall, hardness, cure system and the certification you have to meet. We will confirm whether the tolerance is achievable and what the post-cure and documentation package looks like.




 KO
 EN
 ES
 FR
 DE
 PT
 AR
 RU
 JA
 IT
 NL
 TR
 PL
 ID
