Vacuum Versus Pressure Forming: Detail, Cost and the Tool Each Needs
Vacuum holds a 6 mm corner radius. Pressure at 700 kPa holds 1.2, and it evens the wall from a 0.45 ratio to 0.68 with a plug. The tool is the same; the press is not.
Accueil / Blog

Vacuum holds a 6 mm corner radius. Pressure at 700 kPa holds 1.2, and it evens the wall from a 0.45 ratio to 0.68 with a plug. The tool is the same; the press is not.

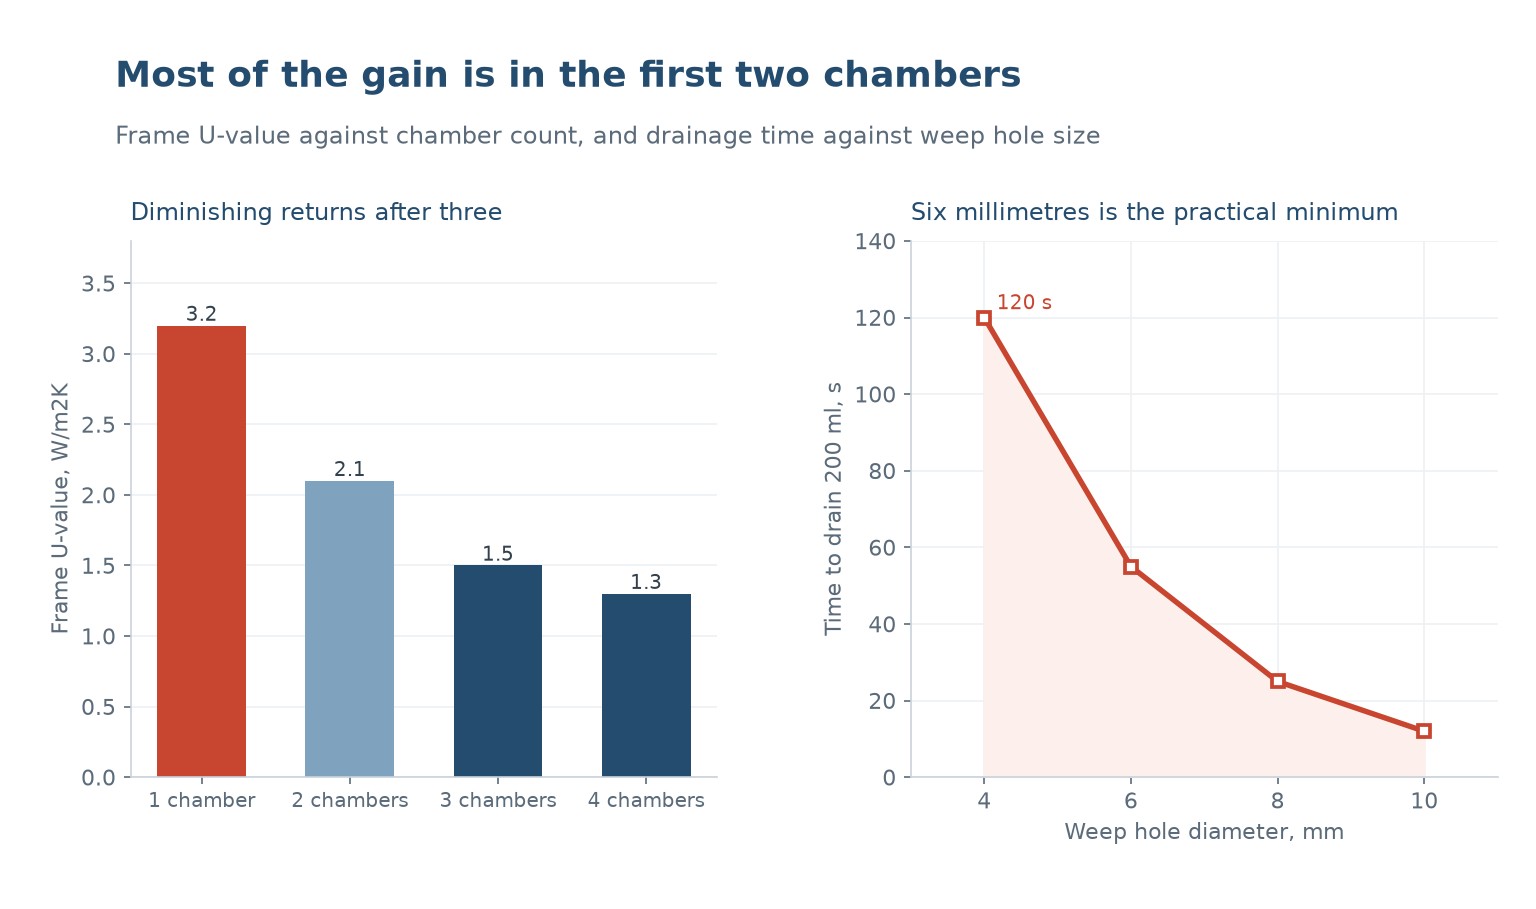
Most of the thermal gain in a door profile is in the first two chambers, and most of the water problems are in the last ten millimetres of the sill. A 6 mm weep hole drains in 55 seconds; a 4 mm one takes two minutes.

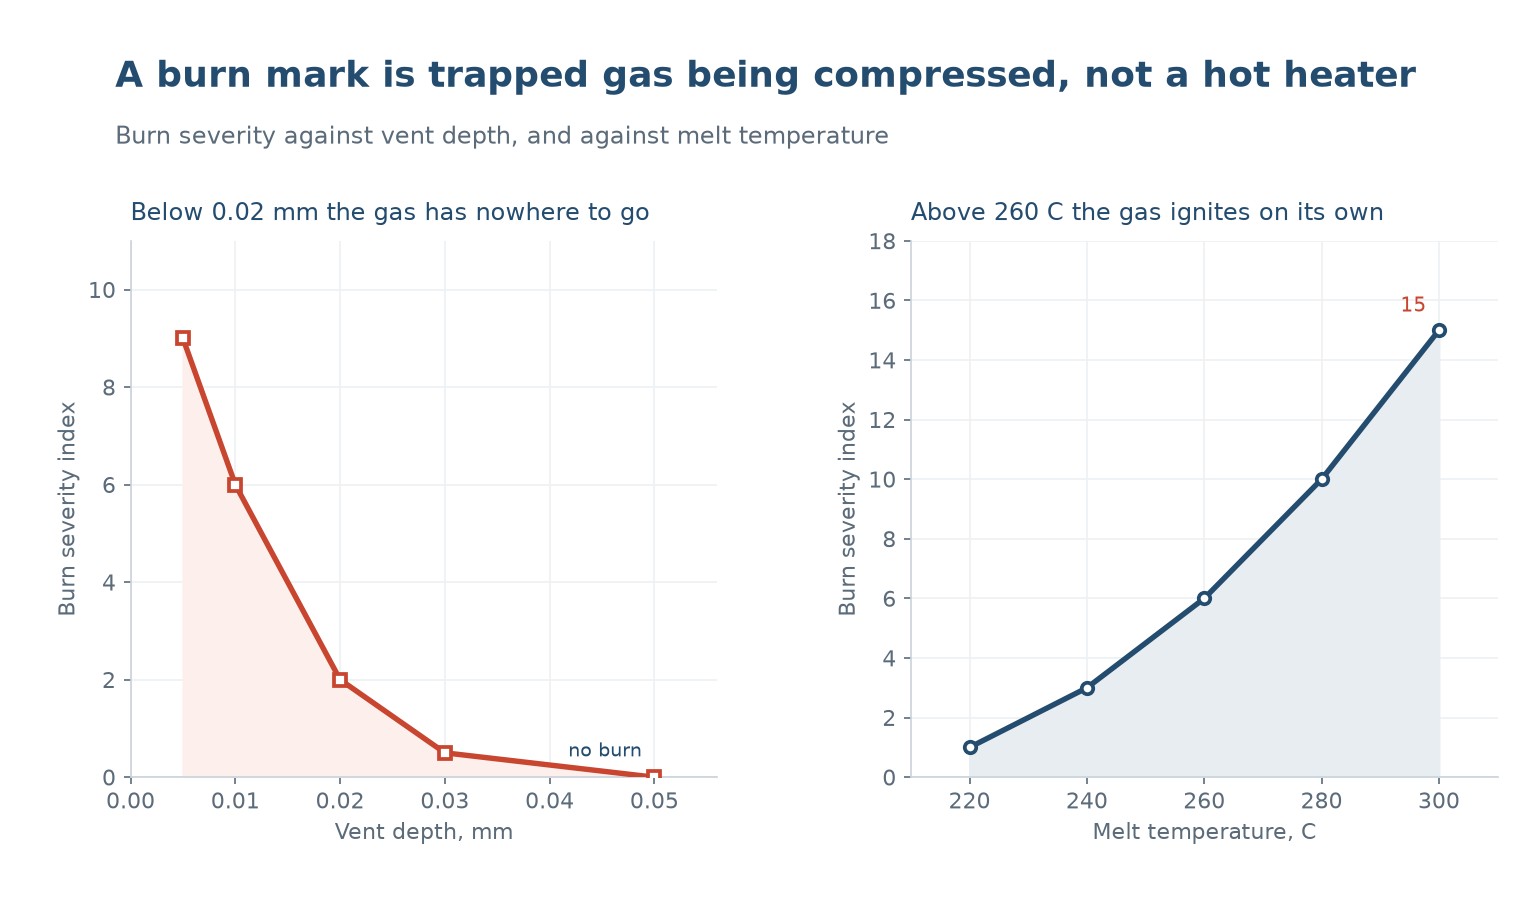
A burn mark is gas compressed to ignition temperature, not a hot barrel. Below a 0.02 mm vent the gas has nowhere to go, and above a 260 °C melt it ignites on its own.
Liquid silicone cures in 25 seconds at 120 °C and 3.2 at 200. The mould runs at 180 to 200 and the runner is kept at 20, which is why the process needs a cold-runner block and a machine that can dose two components accurately.

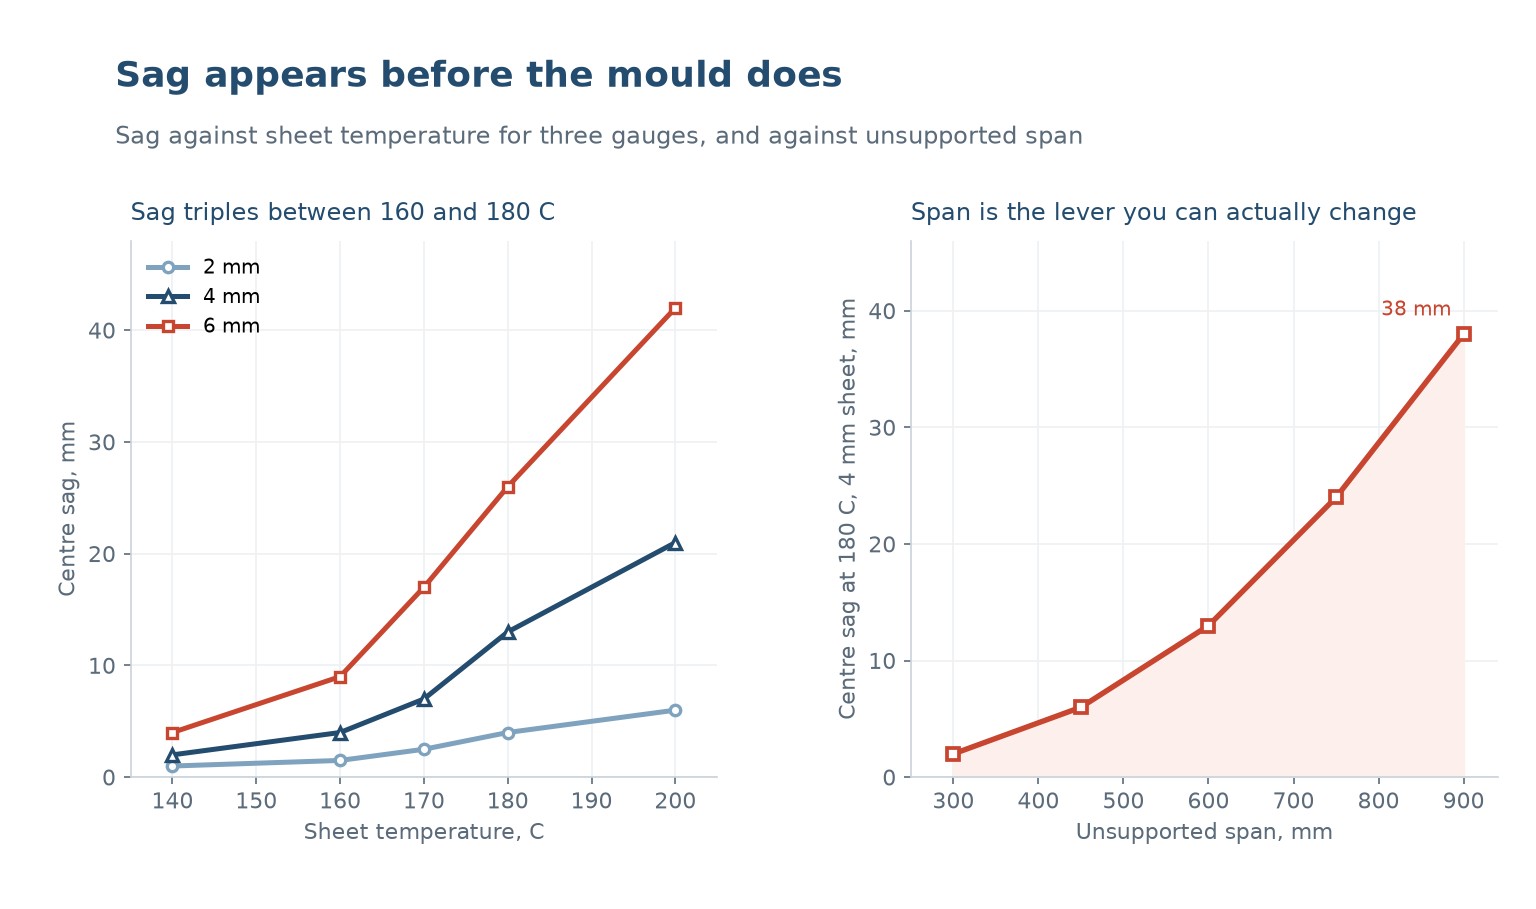
Sag triples between 160 and 180 °C, and it grows with the fourth power of the span. By the time the sheet reaches the mould it has already changed shape, and no amount of vacuum recovers it.

An unreinforced PVC window passes at 1.5 metres and fails at 2. A steel section brings the deflection back under 8 mm at 3 metres, but only if the screw that holds the frame actually reaches the steel.

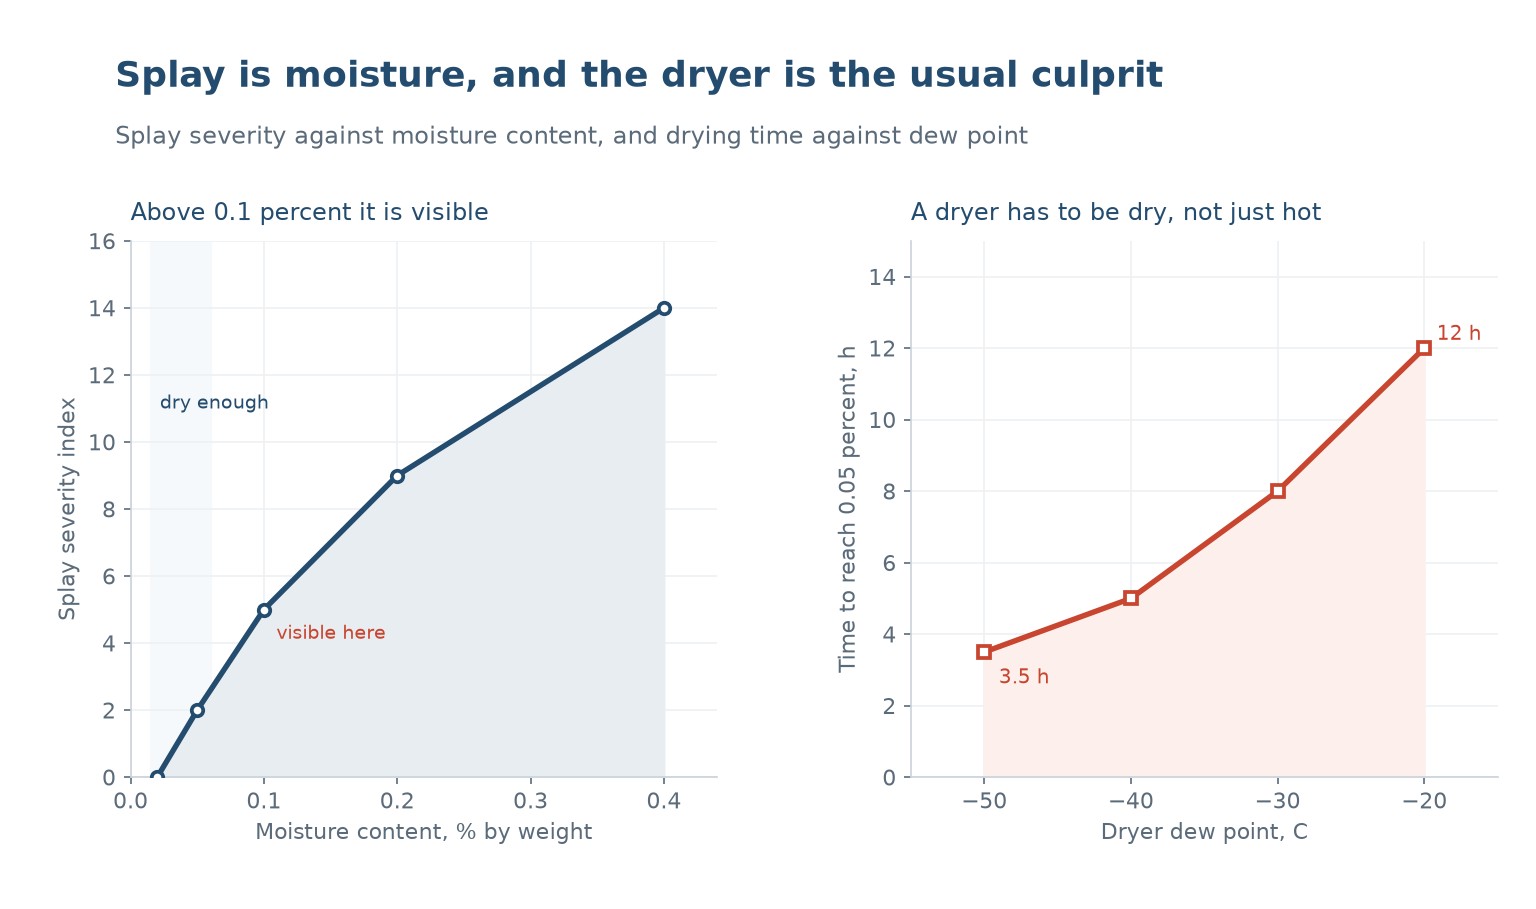
Splay appears above about 0.1 percent moisture, and the fix is a dew point below -40 °C, not a longer dwell in a dryer that is pulling wet air. Most dryer controllers report a set point, not a measurement.
Transfer moulding closes the cavity before it fills, so the compound cannot run out to flash. Waste drops from 18 percent to 6, and a preheated pot cuts the cure by about a third.

Contact heating halves the heat-up time at every gauge and then hands you a temperature spread of plus or minus 14 °C on a textured sheet. Radiant is slower and holds plus or minus 3 with the right zoning.

Trunking stiffness is cubed in the wall, so 20 percent more wall buys 70 percent more stiffness. The snap lid is the other half of the problem, and past a millimetre of undercut it will not come off again.

A weld line reaches 55 percent of bulk strength at 210 °C and 90 percent at 290. It is the weakest feature in most moulded parts, and it is usually placed by the gate, not by the material.
Compression moulding is the oldest way to make a silicone part and still the most common. Cure time runs from 12 minutes at 120 °C to 1.6 at 200, and a 10 mm section costs eleven times the cure of a 2 mm one.
Chez Uplastech, nous nous spécialisons dans la fourniture de solutions de fabrication de produits plastiques personnalisés de haute qualité, conçus pour répondre aux divers besoins des industries du monde entier.
Copyright 2023 © Tous droits réservés Design by Rometheme
Cliquer pour discuter
Je suis en ligne maintenant.
Bonjour, je suis John d'Uplastech, comment puis-je vous aider aujourd'hui ?
🟢 Online | Politique de confidentialité
WhatsApp us
Demander un devis rapide
Envoyer les dessins et les exigences détaillées via
Emial: [email protected]
Ou remplissez le formulaire de contact ci-dessous :