

Vertical walls on device housings drag on release and leave scuffed bands; review draft, tool finish and release practice before the cosmetic limit is set.
What the failure looks like on the line
Equipment housings for clinical environments are judged on cleanability, fit and surface finish, with documentation reviewed separately from the part itself.
Fine vertical scratches appear on the side walls of the housing as the part is lifted off the tool, and rejection concentrates on the visible faces.
A near-vertical wall stays in contact with the tool through most of the release stroke, so the shrinking part slides against the tool surface instead of separating cleanly. Friction at that interface polishes or scores the soft, still-warm polymer before it has fully cooled.
Buyers and suppliers usually agree on the drawing and disagree on the conditions under which the drawing was checked. On a buyer's specification this distinction matters: a part can measure inside tolerance and still fail in use, because the drawing records geometry while the complaint records behaviour. Draft angle on external walls is usually the first value both sides compare, and it is also the one most often quoted without the conditions attached to it.
The process window that decides it
Four variables move this result more than the rest. The ranges below are illustrative engineering guidance for a first discussion; confirm them on your own tool, material grade and part geometry before they become contract terms.
| Variable | Typical window | What fails outside it |
|---|---|---|
| Draft angle on external walls | 3-5 deg minimum | Below this the part drags along the tool during release |
| Tool surface finish | Polished or fine-textured, Ra 0.8-1.6 micrometre | A coarse finish increases friction and visible scoring |
| Demould part temperature | Below 60-70 C before release | Releasing too warm keeps the surface soft enough to mark |
| Release agent coverage | 0.5-1.0 g/m2 per cycle | Heavy or patchy deposits transfer to the cosmetic face |
Table 1. Starting window for a joint process trial. Values are engineering guidance, not a measured survey.
Draft angle on external walls is typically held at 3-5 deg minimum. Below this the part drags along the tool during release Record it together with the measurement point and the moment in the cycle; a single number without a location is not a process setting.
Tool surface finish is typically held at Polished or fine-textured, Ra 0.8-1.6 micrometre. A coarse finish increases friction and visible scoring When this drifts, the symptom usually appears at one cavity, one sheet position or one lane before it appears across the whole batch.
Demould part temperature is typically held at Below 60-70 C before release. Releasing too warm keeps the surface soft enough to mark A change here is cheap during a trial and expensive after tooling release, so treat it as a controlled variable with a documented re-approval.
Release agent coverage is typically held at 0.5-1.0 g/m2 per cycle. Heavy or patchy deposits transfer to the cosmetic face Put it on the change-control list, otherwise an unannounced material or setting substitution will be mistaken for ordinary process noise.
Reading the response curve
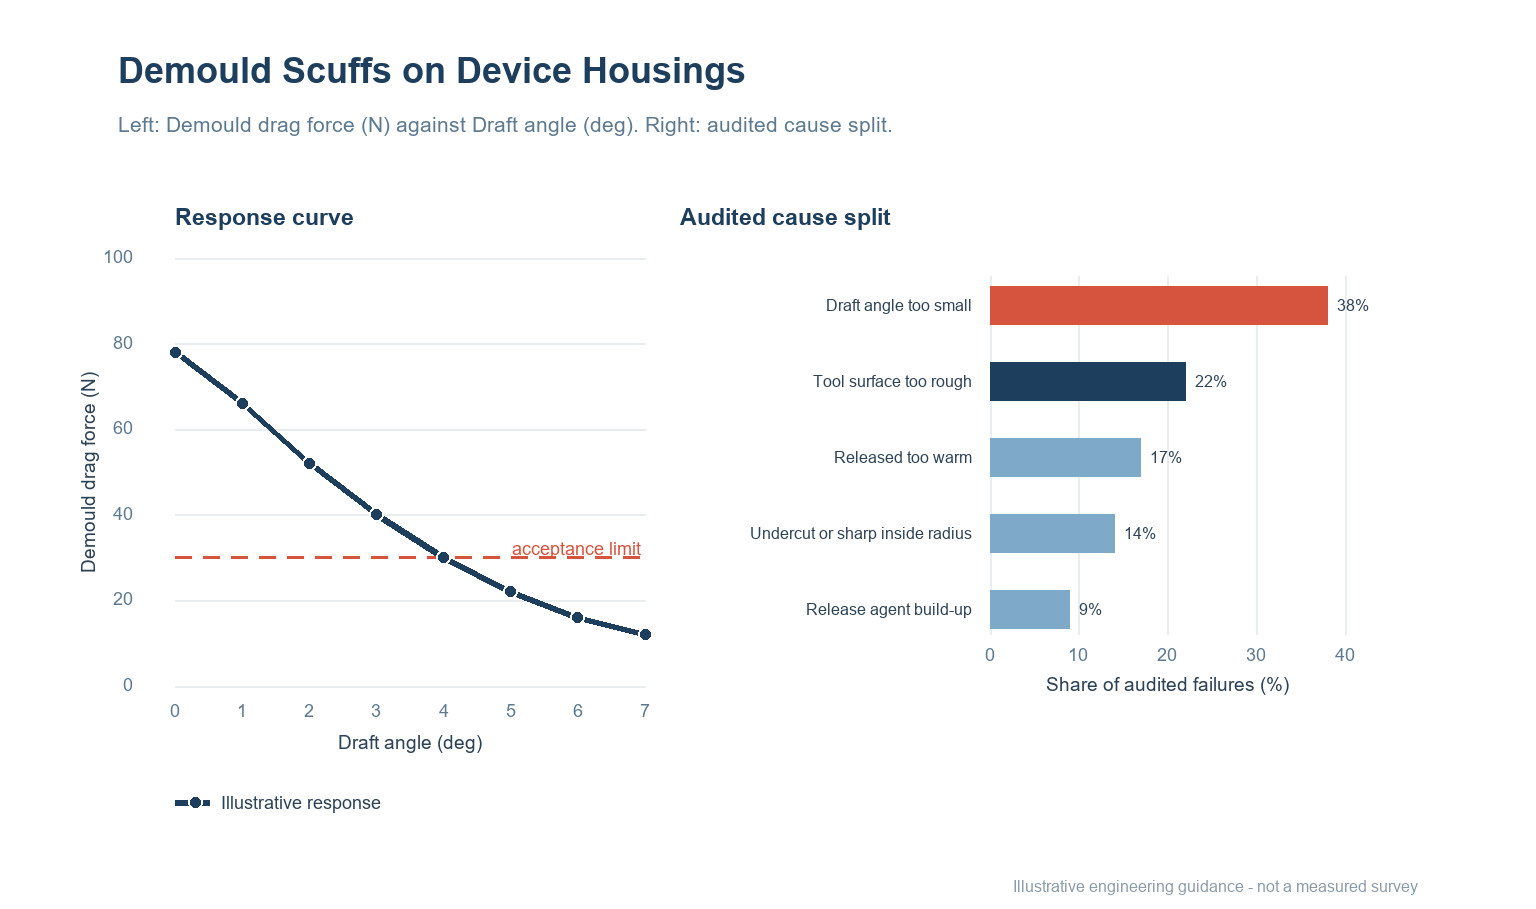
The left panel shows demould drag force (n) as draft angle (deg) increases: the response falls from 78 to 12 on the illustrative 0–100 scale. The dashed line at 30 marks a proposed acceptance limit, not a universal standard. Move that line only after the test method and the sample plan have been agreed, otherwise two suppliers can both be compliant and still deliver different parts.
Read the shape rather than a single point. A curve that changes quickly near the limit is more sensitive to ordinary process noise than one that approaches it gradually, and that difference should be reflected in how tightly the setting is controlled and how often it is checked.
Where the causes actually sit
The right panel of Figure 1 splits audited failures of this type into five groups. The percentages are illustrative engineering guidance for prioritising an investigation, not a measured survey and not a prediction for your line.
| Cause | Illustrative share | First check |
|---|---|---|
| Draft angle too small | 38% | Measure the draft angle on every external wall against the approved drawing. |
| Tool surface too rough | 22% | Inspect the tool surface for burrs and polished wear bands under raking light. |
| Released too warm | 17% | Record part temperature at the moment release begins. |
| Undercut or sharp inside radius | 14% | Compare scuff location against the tool's parting and vent features. |
| Release agent build-up | 9% | Agree a cosmetic limit sample that defines the acceptable scuff band. |
Table 2. Cause split and the corresponding first check. Shares are indicative and sum to 100.
Draft angle too small accounts for roughly 38% of the illustrative split. Measure the draft angle on every external wall against the approved drawing. Start here before authorising a material or tooling change, because it is the fastest explanation to confirm or eliminate.
Tool surface too rough accounts for roughly 22% of the illustrative split. Inspect the tool surface for burrs and polished wear bands under raking light. Start here before authorising a material or tooling change, because it is the fastest explanation to confirm or eliminate.
Released too warm accounts for roughly 17% of the illustrative split. Record part temperature at the moment release begins. Start here before authorising a material or tooling change, because it is the fastest explanation to confirm or eliminate.
Checks before sign-off
Run the same sequence on a retained good sample and on the disputed batch so the comparison means something.
- Measure the draft angle on every external wall against the approved drawing.
- Inspect the tool surface for burrs and polished wear bands under raking light.
- Record part temperature at the moment release begins.
- Compare scuff location against the tool's parting and vent features.
- Agree a cosmetic limit sample that defines the acceptable scuff band.
Keep a retained reference sample beside every result. When a batch is disputed, the comparison that settles it is almost always between the retained part and the current one under the same method, not between either part and a number on a drawing. Record the instrument, the operator, the conditioning time and the position on the part or sheet for each reading.
Writing it into the specification and the evidence pack
Visible side-wall scuffing shall not exceed the agreed limit sample when inspected under the specified lighting and viewing distance after conditioning.
Write the requirement as a behaviour at a stated condition, not as a brand of material or a machine setting. State the test method, the conditioning, the sample plan and the rule for deciding a pass. Where a document is needed, ask the supplier for documentation that covers the actual construction and check its scope against your own market before approval; a document for the base material alone does not describe the finished part you are buying.
At first-article approval, freeze the drawing revision, the material and colour identification, the process window, the tool and cavity identification, and the inspection method. Any later change to grade, site, tool, or window should trigger a new first article rather than a paper waiver. Keep retained samples from the approved lot and from each production lot so that a future comparison is possible.
| Evidence item | What it must show |
|---|---|
| Approved drawing and revision | The exact geometry and tolerances the decision applies to |
| Material and colour identification | Grade, supplier, colour reference and any declared recycled content |
| Process window and change log | The agreed settings and any deviation since approval |
| Inspection record and retained samples | Method, conditions, results and a physical reference from the same lot |
Table 3. Minimum evidence pack for a first-article decision and a later batch dispute.
None of the figures above should be read as a measured survey. They are engineering guidance for framing a joint trial; confirm them on your own tool, grade and geometry before they become contract terms.
Questions buyers ask
Is this a material problem or a process problem?
A near-vertical wall stays in contact with the tool through most of the release stroke, so the shrinking part slides against the tool surface instead of separating cleanly. Friction at that interface polishes or scores the soft, still-warm polymer before it has fully cooled. It is worth separating the two before a supplier changes a grade: hold the material constant for one controlled run, then move one setting at a time. If the symptom follows the setting, the material was never the cause.
Can draft angle on external walls be traded against cycle time?
Only within the window stated in Table 1, and only with a recorded trial. Below this the part drags along the tool during release A faster cycle that sits outside the window usually moves the failure downstream, where it costs more to find.
What should be recorded at incoming inspection?
Keep the measurement, the method, the sample identity and the conditions together. Measure the draft angle on every external wall against the approved drawing. A result without its conditions cannot be compared with a later batch.
Does a change of medical device require re-approval?
Treat any change to material grade, tool, site or process window as a change that needs a new first-article decision. For thick-gauge forming work the drawing alone is not enough; the process route is part of what was approved.
How many samples are enough for a first-article decision?
There is no universal number. Sample across cavities, lanes, sheet positions or reel lengths so that the spread is visible, not just the average. Agree the sample plan and the acceptance rule with the supplier before the trial starts.
What belongs in the evidence pack?
The approved drawing and revision, the material and colour identification, the process window, the inspection method and results, the retained reference samples, and documentation covering the actual construction. Ask the supplier to state the scope of each document and check it against your own market.
Seeing this on a current thick-gauge forming job?
Send the drawing, the material and grade, the process window you are running, and the point in the cycle or the shelf life where the fault appears. We will help you separate a material question from a process question and a specification question before anyone changes a tool.
Continue reading
- Draft Angles and Ejection Design: Releasing the Part Cleanly
- The Significance of Draft Angles in Thermoforming: A Comprehensive Guide
- Radius and Draft in Thermoforming: Two Numbers That Decide Everything
- Surface Marking: Chill Marks, Drag Lines and the Sheet That Was Too Cold
- Thermoforming Undercuts: Forming a Feature That Has to Release

 EN
 ES
 FR
 DE
 PT
 AR
 RU
 JA
 KO
 IT
 NL
 TR
 PL
 ID
