Spuitgieten
Colour Matching in Injection Molding: Masterbatch, Drift and Approval
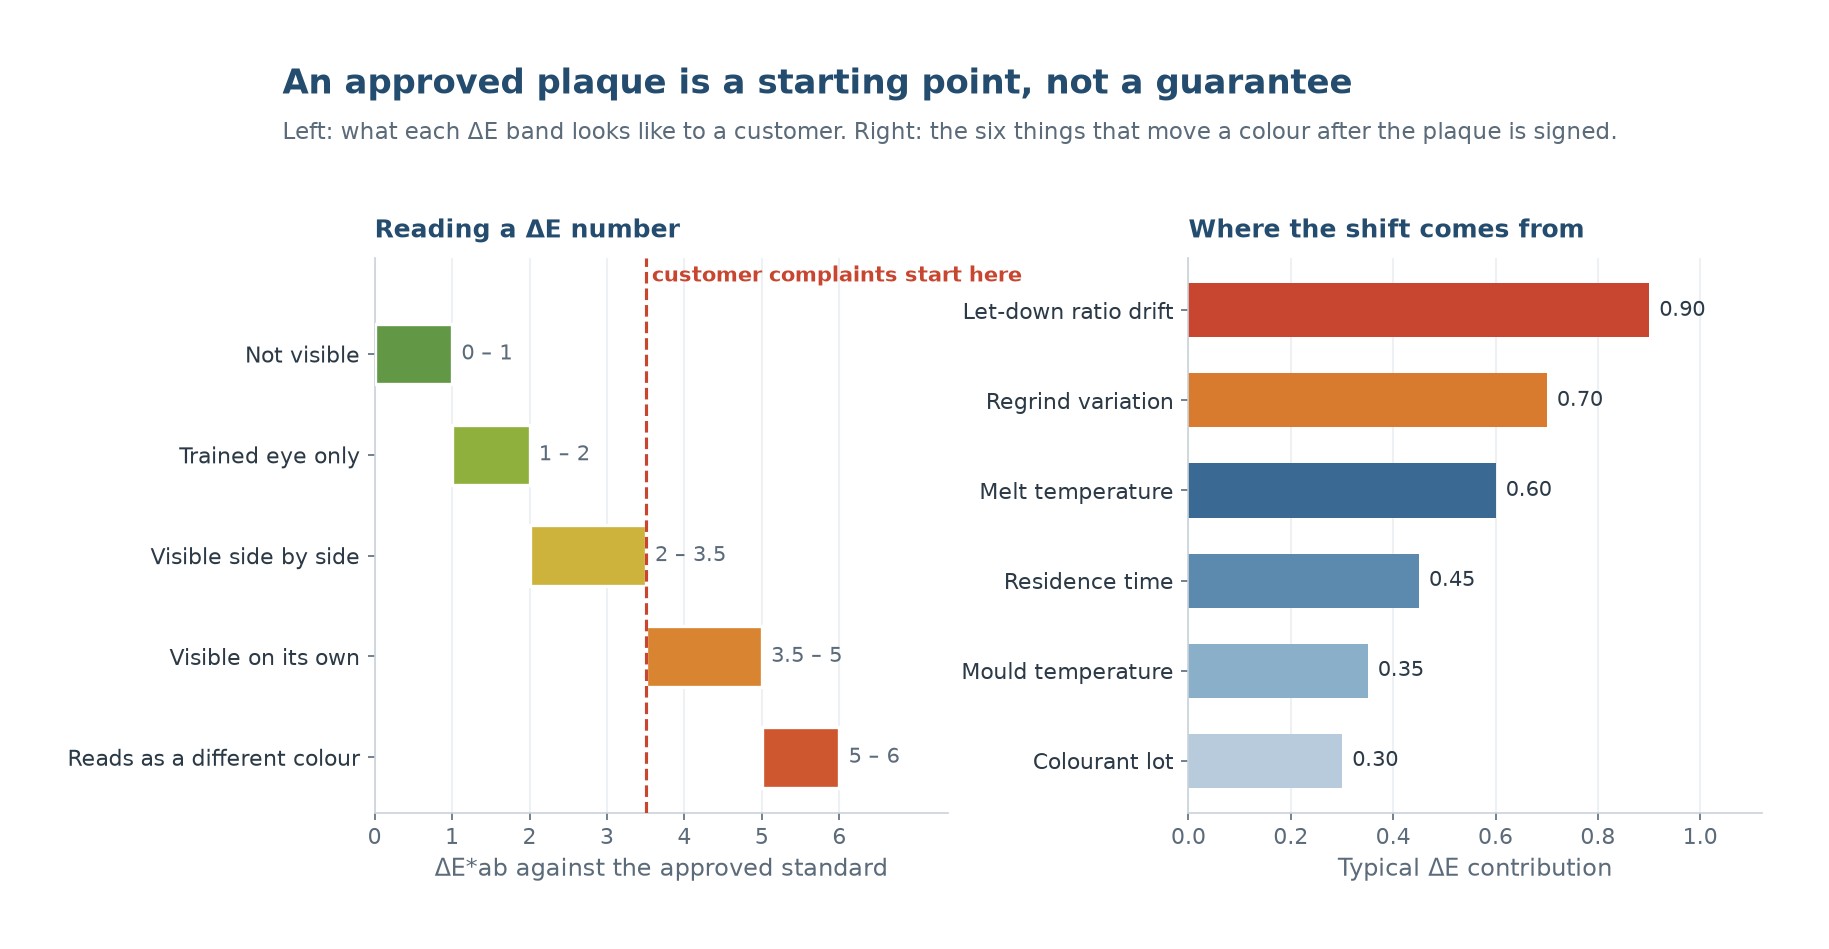
Why a colour approved on a plaque fails on the part: let-down ratio, shear history, regrind and the measurement geometry that decides pass or fail.

Why a colour approved on a plaque fails on the part: let-down ratio, shear history, regrind and the measurement geometry that decides pass or fail.

Cooling is 45-70% of the cycle. How sheet thickness, mould temperature, air assist and demould temperature set the achievable cycle — and where the shortcuts fail.

A colour change costs more in scrap than in labour. The purge sequence, the mechanical cleaning no compound replaces, and how to get from black to natural in one pass.
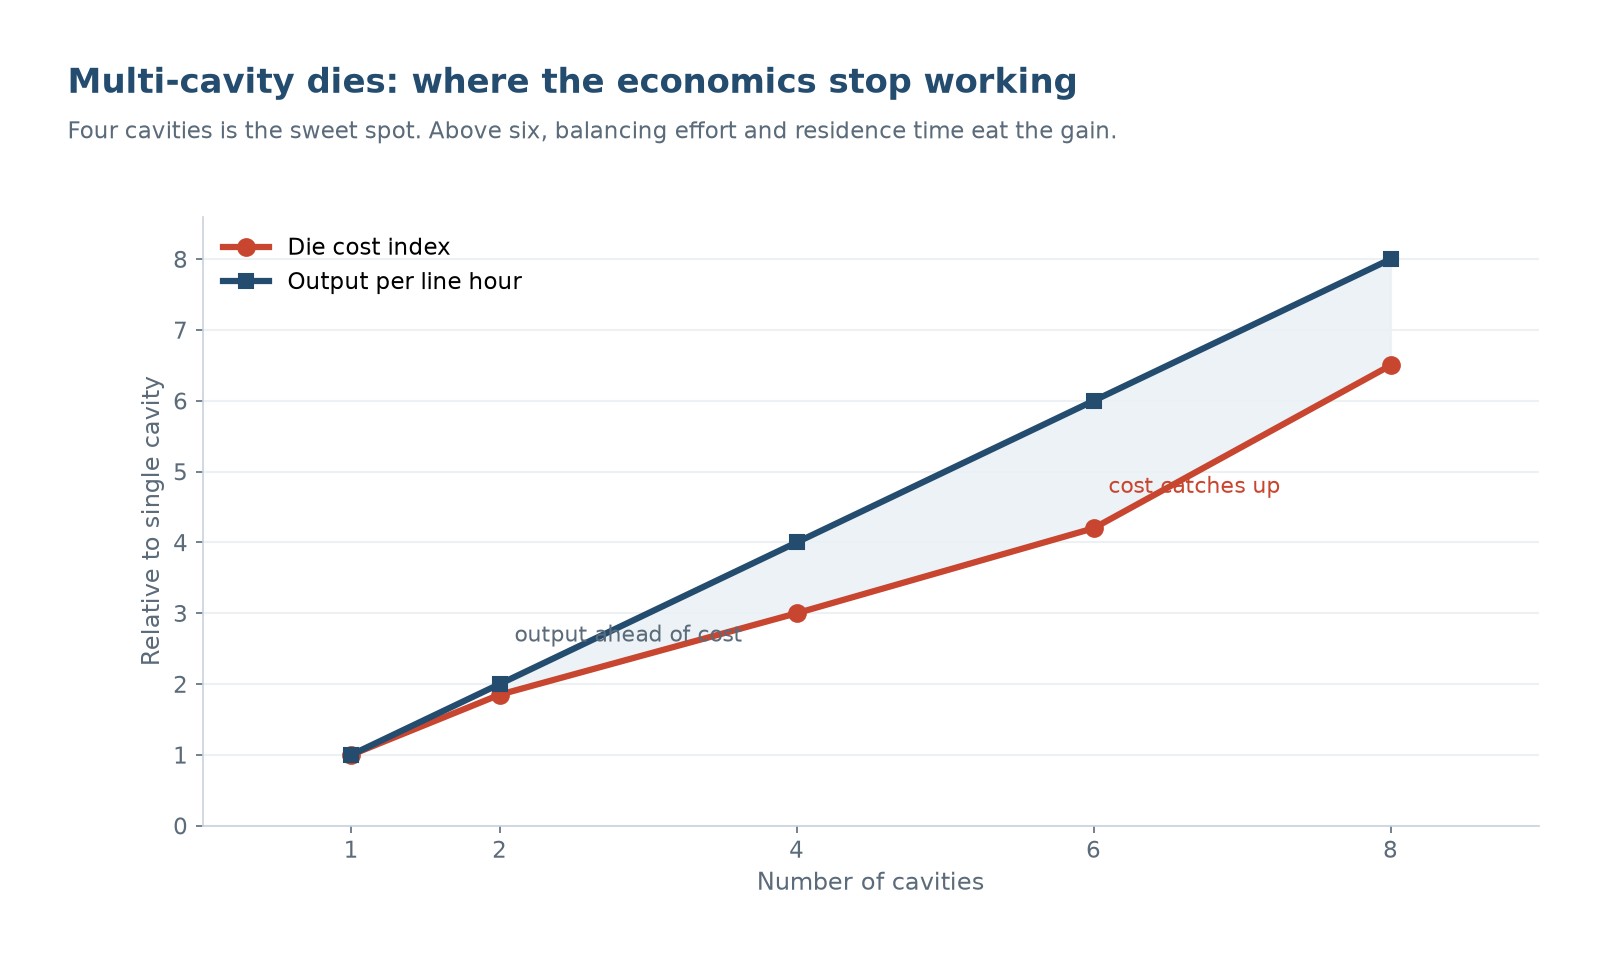
Running two or four profiles through one die doubles output only if the flow is balanced. Land length, manifold design and thermal zoning across cavities.

Undervented tools leave read-through and trapped air; overvented tools leave marks. Hole size, spacing, location and the materials that need vented tooling.

The arithmetic every quotation depends on: specific output, drag flow, puller speed and the take-up ratio that decides whether you hit dimension at the quoted rate.

Pack pressure is set by cavity pressure at gate freeze, not by a number on the controller. How to find gate freeze and what happens either side of it.

A dryer set to the wrong dew point is worse than no dryer. How to read a drying curve, what desiccant and hot air actually achieve, and which resins need it.

Heater type decides heat uniformity, warm-up time and power bill. A comparison across the three common element types and the zoning that makes them work.

Why a profile that measures perfectly on the line bows after a week, and how cooling rate, haul-off tension and a tempering oven change the residual stress field.

What actually happens to tensile strength, impact and surface finish as regrind ratio climbs, and the practical ceiling for PVC, PE, PP and engineering resins.
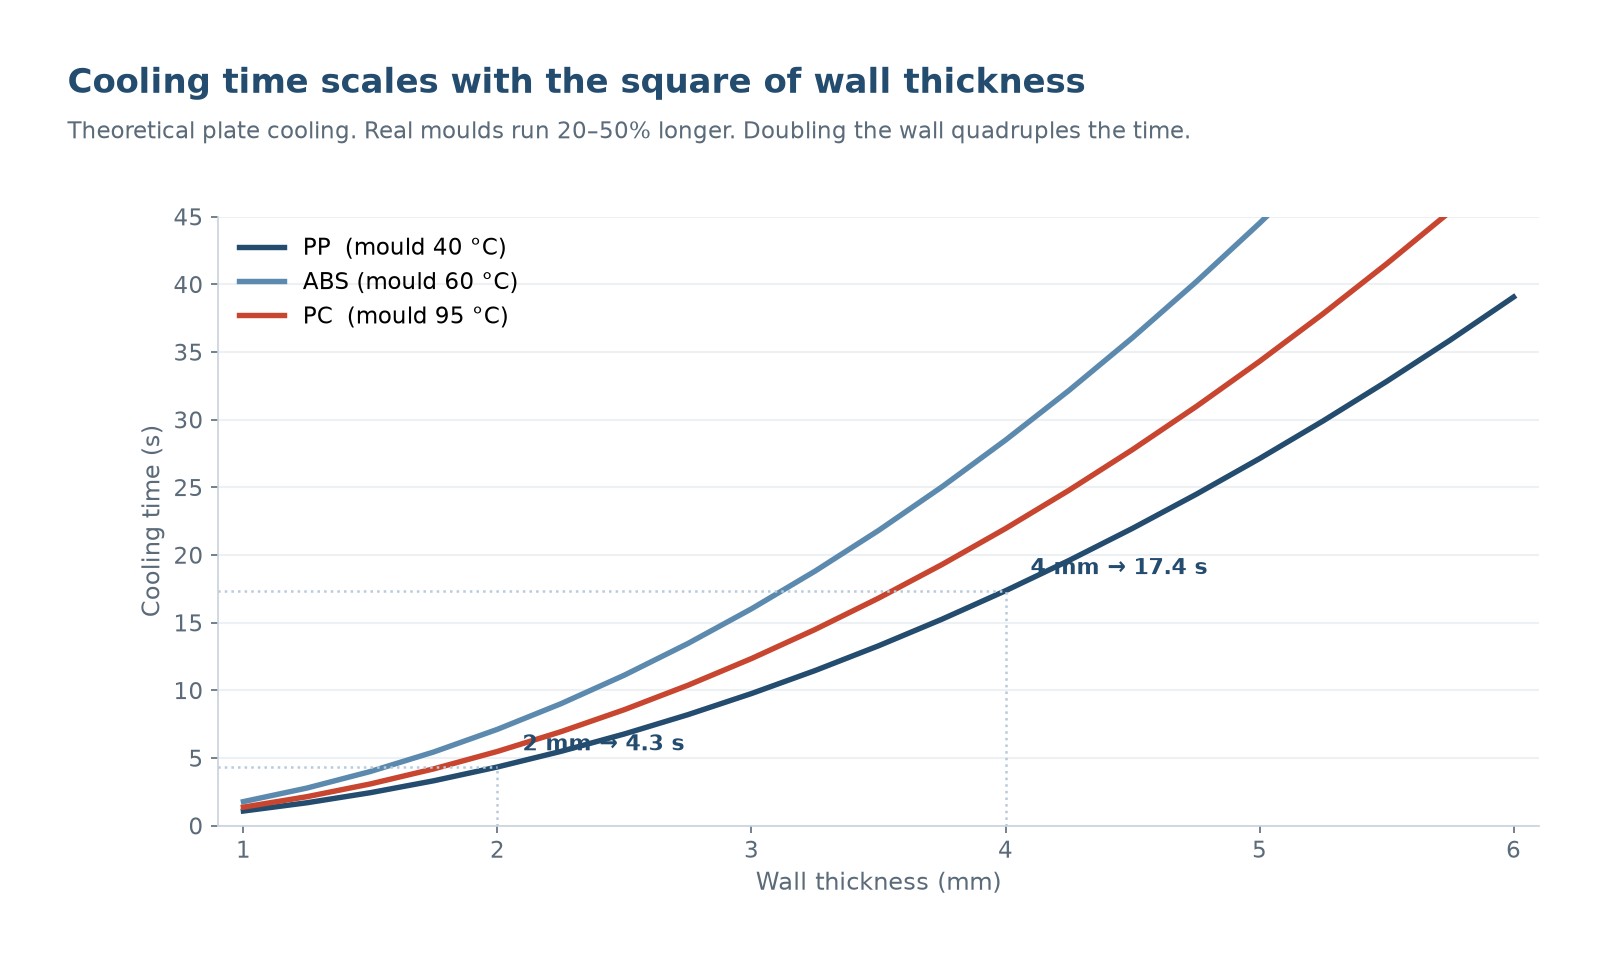
Cooling is over half the cycle and almost all of it is predictable. The thickness-squared rule, the thermal diffusivity term and what actually shortens it.
 NL
 EN
 ES
 FR
 DE
 PT
 AR
 RU
 JA
 KO
 IT
 TR
 PL
 ID
