
A density gradient through the thickness points to heat transfer and gas timing, not to a bad batch average.
What the failure looks like on the line
Silicone foam is specified by density and compression behaviour, and both are easy to quote but hard to hold across a thick section.
A foam pad feels firm at the surface but soft in the core, and a section shows larger, merged cells near the centre.
The skin cools and sets first while the core stays hot, so gas keeps expanding where the network is weakest. Cells there coalesce into larger voids and the local density and recovery diverge from the skin, which a single bulk density reading cannot show.
Buyers and suppliers usually agree on the drawing and disagree on the conditions under which the drawing was checked. On a buyer's specification this distinction matters: a part can measure inside tolerance and still fail in use, because the drawing records geometry while the complaint records behaviour. Mould temperature is usually the first value both sides compare, and it is also the one most often quoted without the conditions attached to it.
The process window that decides it
Four variables move this result more than the rest. The ranges below are illustrative engineering guidance for a first discussion; confirm them on your own tool, material grade and part geometry before they become contract terms.
| Variabile | Typical window | What fails outside it |
|---|---|---|
| Mould temperature | 120-170 C | A steep gradient sets the skin before the core cures |
| Section thickness | as agreed on drawing | Thicker sections widen the skin-to-core gap |
| Cure rate versus gas rate | matched within 10% | Late crosslinking lets core cells merge |
| Cooling dwell before demould | 2-10 min | Early demould freezes the gradient in place |
Table 1. Starting window for a joint process trial. Values are engineering guidance, not a measured survey.
Mould temperature is typically held at 120-170 C. A steep gradient sets the skin before the core cures Record it together with the measurement point and the moment in the cycle; a single number without a location is not a process setting.
Section thickness is typically held at as agreed on drawing. Thicker sections widen the skin-to-core gap When this drifts, the symptom usually appears at one cavity, one sheet position or one lane before it appears across the whole batch.
Cure rate versus gas rate is typically held at matched within 10%. Late crosslinking lets core cells merge A change here is cheap during a trial and expensive after tooling release, so treat it as a controlled variable with a documented re-approval.
Cooling dwell before demould is typically held at 2-10 min. Early demould freezes the gradient in place Put it on the change-control list, otherwise an unannounced material or setting substitution will be mistaken for ordinary process noise.
Reading the response curve

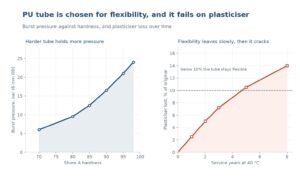
The left panel shows cell coalescence (relative, %) as distance from skin to core (relative) increases: the response rises from 8 to 86 on the illustrative 0–100 scale. The dashed line at 35 marks a proposed acceptance limit, not a universal standard. Move that line only after the test method and the sample plan have been agreed, otherwise two suppliers can both be compliant and still deliver different parts.
Read the shape rather than a single point. A curve that changes quickly near the limit is more sensitive to ordinary process noise than one that approaches it gradually, and that difference should be reflected in how tightly the setting is controlled and how often it is checked.
Where the causes actually sit
The right panel of Figure 1 splits audited failures of this type into five groups. The percentages are illustrative engineering guidance for prioritising an investigation, not a measured survey and not a prediction for your line.
| Causa | Illustrative share | First check |
|---|---|---|
| Skin sets before core | 30% | Section the pad and measure density at skin, mid and core positions. |
| Late crosslink versus gas | 24% | Photograph cell structure at the same three depths. |
| Section too thick | 18% | Compare core cell size against an approved reference sample. |
| Uneven platen temperature | 16% | Log mould temperature at both platens for each run. |
| Early demould | 12% | Check recovery at a fixed deflection separately for each layer. |
Table 2. Cause split and the corresponding first check. Shares are indicative and sum to 100.
Skin sets before core accounts for roughly 30% of the illustrative split. Section the pad and measure density at skin, mid and core positions. Start here before authorising a material or tooling change, because it is the fastest explanation to confirm or eliminate.
Late crosslink versus gas accounts for roughly 24% of the illustrative split. Photograph cell structure at the same three depths. Start here before authorising a material or tooling change, because it is the fastest explanation to confirm or eliminate.
Section too thick accounts for roughly 18% of the illustrative split. Compare core cell size against an approved reference sample. Start here before authorising a material or tooling change, because it is the fastest explanation to confirm or eliminate.
Checks before sign-off
Run the same sequence on a retained good sample and on the disputed batch so the comparison means something.
- Section the pad and measure density at skin, mid and core positions.
- Photograph cell structure at the same three depths.
- Compare core cell size against an approved reference sample.
- Log mould temperature at both platens for each run.
- Check recovery at a fixed deflection separately for each layer.
Keep a retained reference sample beside every result. When a batch is disputed, the comparison that settles it is almost always between the retained part and the current one under the same method, not between either part and a number on a drawing. Record the instrument, the operator, the conditioning time and the position on the part or sheet for each reading.
Writing it into the specification and the evidence pack
Require skin-to-core density spread and core cell-size distribution to be reported against an approved reference sample, not only the bulk density.
Write the requirement as a behaviour at a stated condition, not as a brand of material or a machine setting. State the test method, the conditioning, the sample plan and the rule for deciding a pass. Where a document is needed, ask the supplier for documentation that covers the actual construction and check its scope against your own market before approval; a document for the base material alone does not describe the finished part you are buying.
At first-article approval, freeze the drawing revision, the material and colour identification, the process window, the tool and cavity identification, and the inspection method. Any later change to grade, site, tool, or window should trigger a new first article rather than a paper waiver. Keep retained samples from the approved lot and from each production lot so that a future comparison is possible.
| Evidence item | What it must show |
|---|---|
| Approved drawing and revision | The exact geometry and tolerances the decision applies to |
| Material and colour identification | Grade, supplier, colour reference and any declared recycled content |
| Process window and change log | The agreed settings and any deviation since approval |
| Inspection record and retained samples | Method, conditions, results and a physical reference from the same lot |
Table 3. Minimum evidence pack for a first-article decision and a later batch dispute.
None of the figures above should be read as a measured survey. They are engineering guidance for framing a joint trial; confirm them on your own tool, grade and geometry before they become contract terms.
Questions buyers ask
Is this a material problem or a process problem?
The skin cools and sets first while the core stays hot, so gas keeps expanding where the network is weakest. Cells there coalesce into larger voids and the local density and recovery diverge from the skin, which a single bulk density reading cannot show. It is worth separating the two before a supplier changes a grade: hold the material constant for one controlled run, then move one setting at a time. If the symptom follows the setting, the material was never the cause.
Can mould temperature be traded against cycle time?
Only within the window stated in Table 1, and only with a recorded trial. A steep gradient sets the skin before the core cures A faster cycle that sits outside the window usually moves the failure downstream, where it costs more to find.
What should be recorded at incoming inspection?
Keep the measurement, the method, the sample identity and the conditions together. Section the pad and measure density at skin, mid and core positions. A result without its conditions cannot be compared with a later batch.
Does a change of foam require re-approval?
Treat any change to material grade, tool, site or process window as a change that needs a new first-article decision. For silicone rubber work the drawing alone is not enough; the process route is part of what was approved.
How many samples are enough for a first-article decision?
There is no universal number. Sample across cavities, lanes, sheet positions or reel lengths so that the spread is visible, not just the average. Agree the sample plan and the acceptance rule with the supplier before the trial starts.
What belongs in the evidence pack?
The approved drawing and revision, the material and colour identification, the process window, the inspection method and results, the retained reference samples, and documentation covering the actual construction. Ask the supplier to state the scope of each document and check it against your own market.
Seeing this on a current silicone rubber job?
Send the drawing, the material and grade, the process window you are running, and the point in the cycle or the shelf life where the fault appears. We will help you separate a material question from a process question and a specification question before anyone changes a tool.
Continue reading
- Silicone Sponge: Closed Cell, Open Cell and the Density That Decides
- Silicone Sheet Manufacturing: Calendered, Moulded and the Difference
- Silicone Calendering: Sheet and Coated Fabric in One Pass
- Silicone Compound Formulation: Base, Filler, Additive and Cure
- Silicone Heat Ageing: What Fails, and How Fast



 IT
 EN
 ES
 FR
 DE
 PT
 AR
 RU
 JA
 KO
 NL
 TR
 PL
 ID
