
Why metering is the whole process
In thermoplastic injection moulding the material arrives ready to use. In LSR it arrives as two reactive components that have to be combined at a precise ratio, mixed intimately, and delivered to the mould before the reaction runs away. Every one of those three steps is a place where the process can fail, and all three are upstream of the cavity.
The ratio is the most sensitive. Platinum-catalysed addition cure needs the hydride crosslinker and the vinyl polymer in a stoichiometric balance, and the catalyst to drive it. A mixture that is rich in one component cures, but the network is wrong: the crosslink density is low, the tear strength drops, and the compression set rises. A mixture that is lean in catalyst cures slowly or not at all.
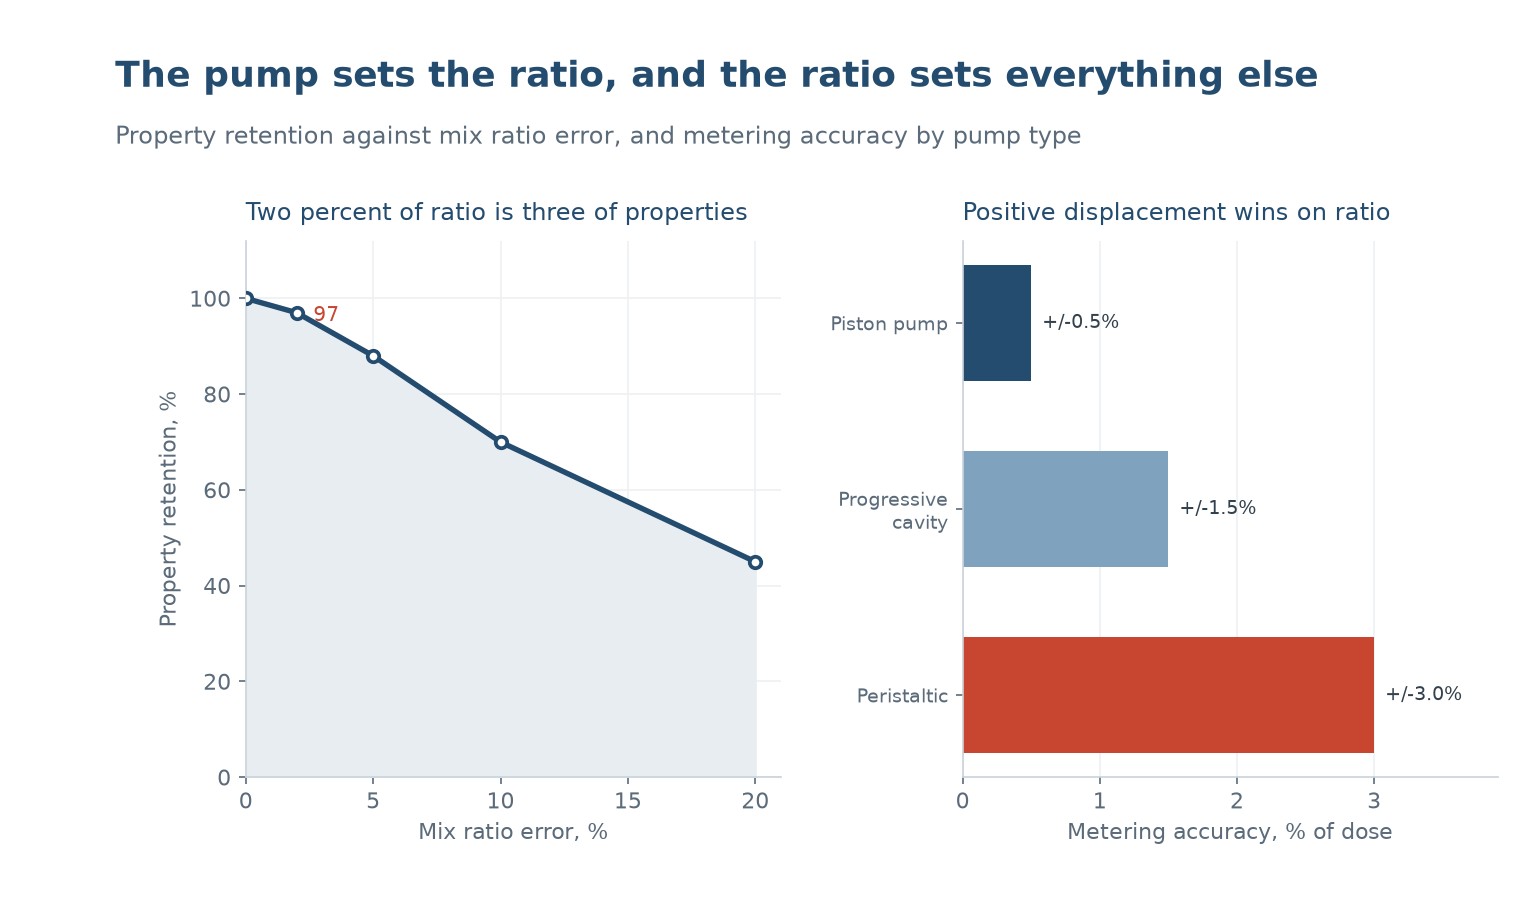
The property loss is steeper than most people expect. At a 2 percent ratio error the physical properties are about 97 percent of nominal, at 5 percent they are 88, at 10 percent they are 70 and at 20 percent they are 45. A 10 percent error is not a subtle degradation; it is a different material.
The pumps set the accuracy
Both components are pumped from drums by positive displacement pumps, and the accuracy of those pumps sets the ratio accuracy. Piston pumps hold about plus or minus 0.5 percent of dose, progressive cavity pumps about 1.5 percent, and peristaltic pumps about 3 percent.
Piston pumps are the standard for LSR because they meter a fixed volume per stroke, which is insensitive to viscosity. Their limitation is that they are cyclic: the dose arrives in pulses, and the machine has to smooth that into a continuous shot. Progressive cavity pumps deliver continuously and are simpler, but their output drifts as the stator wears, and the drift is different for part A and part B, which changes the ratio.
| Pump type | Précision | Delivers | Watch out for |
|---|---|---|---|
| Piston | +/- 0.5 percent | Discrete strokes | Pulsation; needs a smoothing accumulator |
| Progressive cavity | +/- 1.5 percent | En continu | Stator wear changes the ratio over months |
| Peristaltic | +/- 3 percent | En continu | Tube wear and creep; used mainly for pigments |
Table 1 — Metering pump types, their accuracy, and their failure mode.
The drift of a progressive cavity pump is the one that catches people out, because it is invisible. The machine holds the ratio it was set to, but the actual delivered volume changes as the stator wears, and part A and part B do not wear at the same rate. A line that ran perfectly for a year starts producing parts with a slight tackiness, and the cause is a worn stator rather than anything in the process settings.
Mixing: the static mixer is a consumable
Almost all LSR machines use a disposable static mixer: a plastic tube with a helical element that splits and recombines the flow. It has no moving parts, it costs a few euros, and it works extremely well until it does not.
The failure mode is gradual. Silicone cures slowly inside the mixer, starting at the walls where the material is oldest and warmest, and the cured layer narrows the passages. The pressure rises, the mixing quality falls, and eventually a slug of partially cured material is delivered into a cavity. The part has a soft, tacky region that may not be visible until it is flexed.
The discipline is to replace the mixer on a schedule rather than on failure. Every shift is typical for a busy line, every drum for a slow one, and always after any shutdown long enough for the material in the mixer to start curing. A mixer that has sat overnight is a mixer that should be replaced before the first shot.
The needle seal
The needle seal is the valve between the cold runner and the cavity, and it is what allows LSR to be injection moulded at all. The material in the runner is liquid at 20 °C; the material in the cavity cures at 190. The needle has to open to let the shot in and close before the heat travels back up the sprue and cures the runner.
There are two arrangements. A needle valve uses a mechanical pin that seats into the gate, giving positive shut-off and clean gate break. An open drop relies on the material's own viscosity and the thermal balance to freeze the gate, which is simpler and cheaper but only works for small gates and short cycles.
The needle valve is the reason a 32 or 64 cavity LSR tool is practical. Each drop can be opened and closed individually, so the tool can be filled sequentially and every cavity sees the same pressure. With open drops, a large tool will not balance, and the outer cavities will be short or flash depending on where the thermal balance lands.
| Fonctionnalité | Needle valve | Open drop |
|---|---|---|
| Shut-off | Positive, mechanical | Relies on the gate freezing |
| Gate quality | Clean, small witness mark | A tear-off that needs trimming |
| Cavity count | Up to 64 or more | Small tools only |
| Coût | Higher; each drop has a needle and an actuator | Plus bas |
| Failure mode | Needle wear or a stuck actuator | Gate freeze inconsistent, so short shots or flash |
Table 2 — Needle valve against open drop, and what each one costs you.
Needle wear is the maintenance item. The needle seats against a hardened gate insert, and after a few hundred thousand cycles the seat wears and the gate starts to flash. A worn needle is not repairable in place; the insert is replaced, and it is worth keeping a spare set for a production tool.
The metering faults that cause scrap
| Symptom | Likely cause | Check |
|---|---|---|
| Soft, tacky patches | Ratio error or an exhausted mixer | Shot into a cup and inspect for homogeneity |
| Bubbles in the part | Air entrained in dosing, or degassing off | Vacuum level on both components, drum level, pump seals |
| Short shots on outer cavities | Needle not opening fully, or a cold drop | Needle stroke, and the temperature of the cold runner |
| Flash on one cavity only | Worn needle seat at that drop | Inspect the gate insert under magnification |
| Cure drifting over a shift | Progressive cavity stator wear, or component temperature drift | Component temperatures, and a ratio check with a scale |
Table 3 — LSR metering faults, their causes and the first thing to check.
The ratio check with a scale is the simplest diagnostic and the most under-used. Dispense a fixed number of shots into two cups with the needle closed, weigh them, and compare the masses against the expected ratio. It takes five minutes and it separates a metering problem from a moulding problem definitively.
Maintenance that keeps the ratio honest
An LSR line rewards a maintenance schedule more than almost any other process, because most of its failure modes are gradual and invisible. The following four items cover most of the risk.
- Replace the static mixer on a fixed schedule and after every shutdown.
- Check the ratio by weight weekly, and log it, so that drift is visible as a trend rather than as a defect.
- Inspect the needle seats at a fixed interval, and replace the gate inserts as a set rather than one at a time.
- Verify the component temperatures, because viscosity changes with temperature and a dose that is volumetric will deliver a different mass if the component is cold.
The fourth item is the subtle one. A volumetric pump delivers a fixed volume, and if the component is 5 °C cooler its density is higher, so the mass delivered is higher and the ratio shifts. That is why the drums are usually temperature controlled and why a line that runs cold first thing in the morning can produce different parts from the same settings in the afternoon.
How accurate does the LSR mix ratio need to be?
Within about 2 percent to keep the physical properties within 3 percent of nominal. At 10 percent error the properties are down about 30 percent, which is a different material.
Which pump is best for LSR?
Piston pumps, at about plus or minus 0.5 percent of dose. Progressive cavity pumps are simpler but drift as the stator wears, and peristaltic pumps are used mainly for pigments.
How often should the static mixer be replaced?
Every shift on a busy line, every drum on a slow one, and always after a shutdown long enough for material to start curing inside it.
What is a needle seal for?
It shuts off the gate between the cold runner and the hot cavity, so the shot goes in and the runner stays liquid. Without it, heat travels back up the sprue and cures the runner.
Why do outer cavities go short?
Usually a needle that is not opening fully, or a cold drop. With open drops instead of needle valves, a large tool simply will not balance.
Why do parts get tacky over a shift?
Either an exhausted mixer or a ratio drift. Progressive cavity stators wear, and component temperature changes alter the delivered mass even when the volume is correct.
Setting up an LSR line or chasing scrap?
Send the part, the volume and the current scrap rate. We will tell you whether the metering, the mixing or the needle seal is the constraint, and what the tool needs.
Continue reading
- Liquid Silicone Rubber: Two Components, One Second, No Waste
- Silicone Injection Moulding: Cold Runner, Hot Mould, Fast Cure
- Silicone Transfer Moulding: Better for Complex Parts and Inserts
- Silicone Compound Formulation: Base, Filler, Additive and Cure
- Medical-Grade Silicone: USP Class VI and ISO 10993




 FR
 EN
 ES
 DE
 PT
 AR
 RU
 JA
 KO
 IT
 NL
 TR
 PL
 ID
