
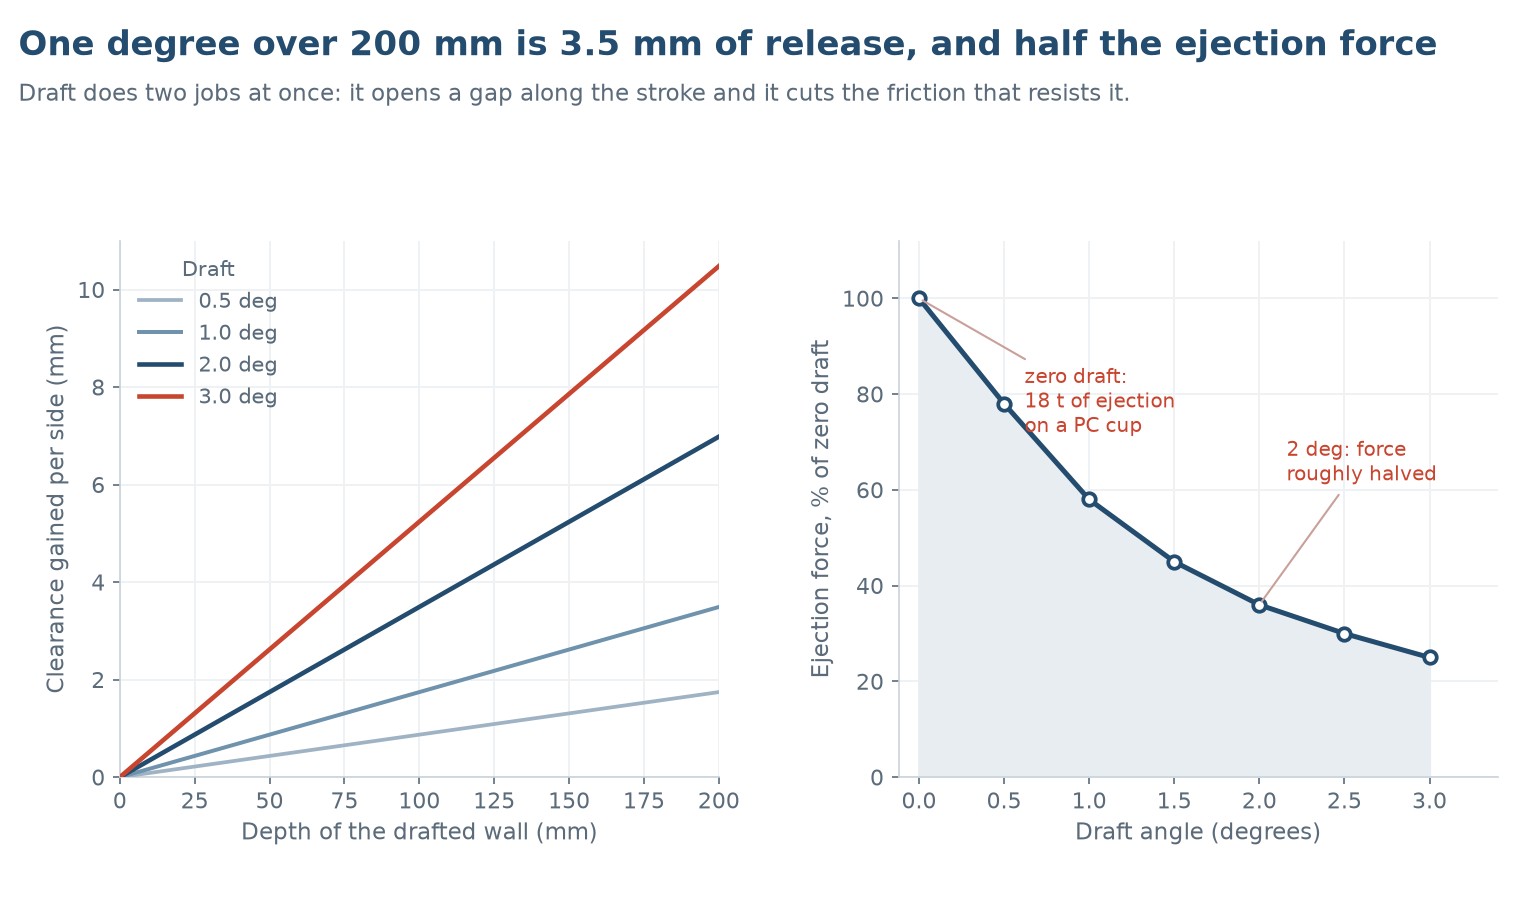
Draft Angles and Ejection Design: Releasing the Part Cleanly
Draft is not a tolerance allowance, it is what makes ejection force achievable. Minimum angles by material and depth, texture multipliers, and the ejector layout that stops pin marks.
الصفحة الرئيسية / المدونة

Draft is not a tolerance allowance, it is what makes ejection force achievable. Minimum angles by material and depth, texture multipliers, and the ejector layout that stops pin marks.

Five independent errors, and the largest one is the sheet you started with. Practical tolerance bands by dimension type, and how to write a drawing that can be inspected.

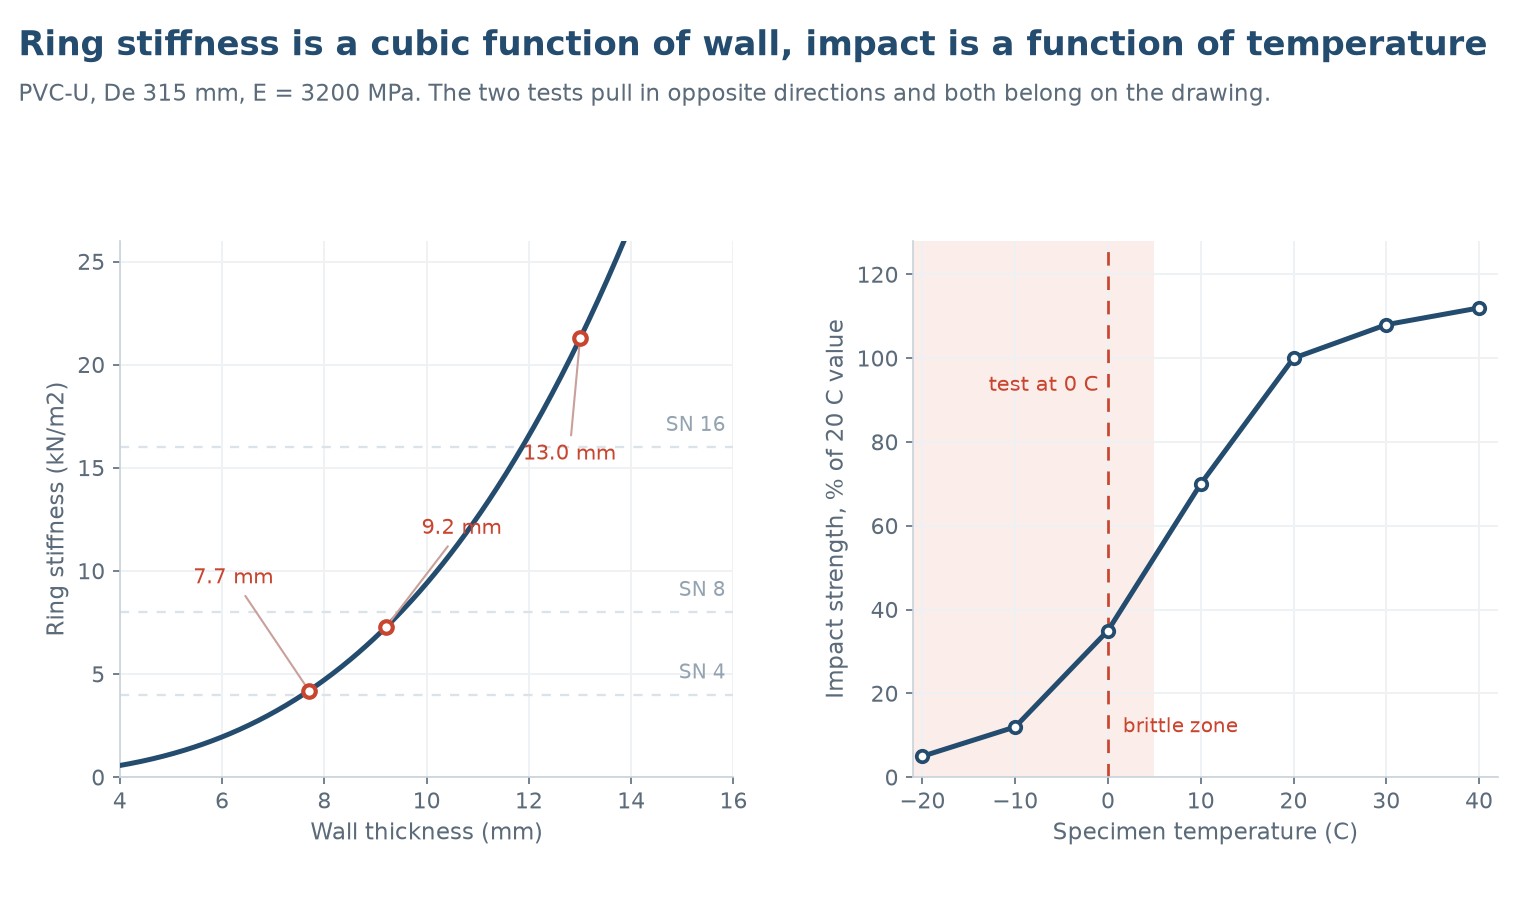
Ring stiffness goes with the cube of wall thickness and impact goes down as temperature falls. Why a pipe can pass one test and fail the other, and how to specify both.

A burn mark is compression ignition, not a hot barrel. Where cavity air gets trapped, how deep a vent land should be, and how to read the burn to find the trap.

A CO2 laser is the only common process that leaves acrylic polished straight off the machine. What the beam does, why cast and extruded differ, and the design rules.

Two clear tubes that fail in completely different ways. The choice is usually made by one number, notched impact, and it is rarely light transmission.
Liquid silicone and high-consistency rubber are different materials with different tooling. Five processes, what each is for, and where platinum cure beats peroxide.

Most start-up scrap is made in the first hour, and most of it is avoidable. Heat soak, purge, string-up, steady state, and why shutdown matters just as much.

Surface energy decides whether anything will stick. Choosing between adhesive, solvent, welding and fasteners, and the joint designs that stop a formed part from cracking.

Clamping force is projected area times cavity pressure, plus a safety factor. Where each number comes from, and what both too little and too much tonnage cost you.

Packing is where a profile that passed inspection arrives bent or scuffed. Bundle design, container length utilisation and the specification that prevents claims.

Acrylic fails in the store and at the machine far more often than in service. Two variables decide it: moisture content and thermal gradient.
في Uplastech، نحن متخصصون في تقديم حلول تصنيع المنتجات البلاستيكية عالية الجودة والمخصصة والمصممة لتلبية الاحتياجات المتنوعة للصناعات في جميع أنحاء العالم.
جميع الحقوق محفوظة © 2023 © جميع الحقوق محفوظة تصميم رميمة
انقر للدردشة
أنا متصل بالإنترنت الآن.
مرحبًا، أنا جون من Uplastech، كيف يمكنني مساعدتك اليوم؟
واتساب لنا
🟢 سياسة الخصوصية على الإنترنت
WhatsApp us
اطلب عرض أسعار سريع
