
Transfer needs the sheet soft and the roll hard
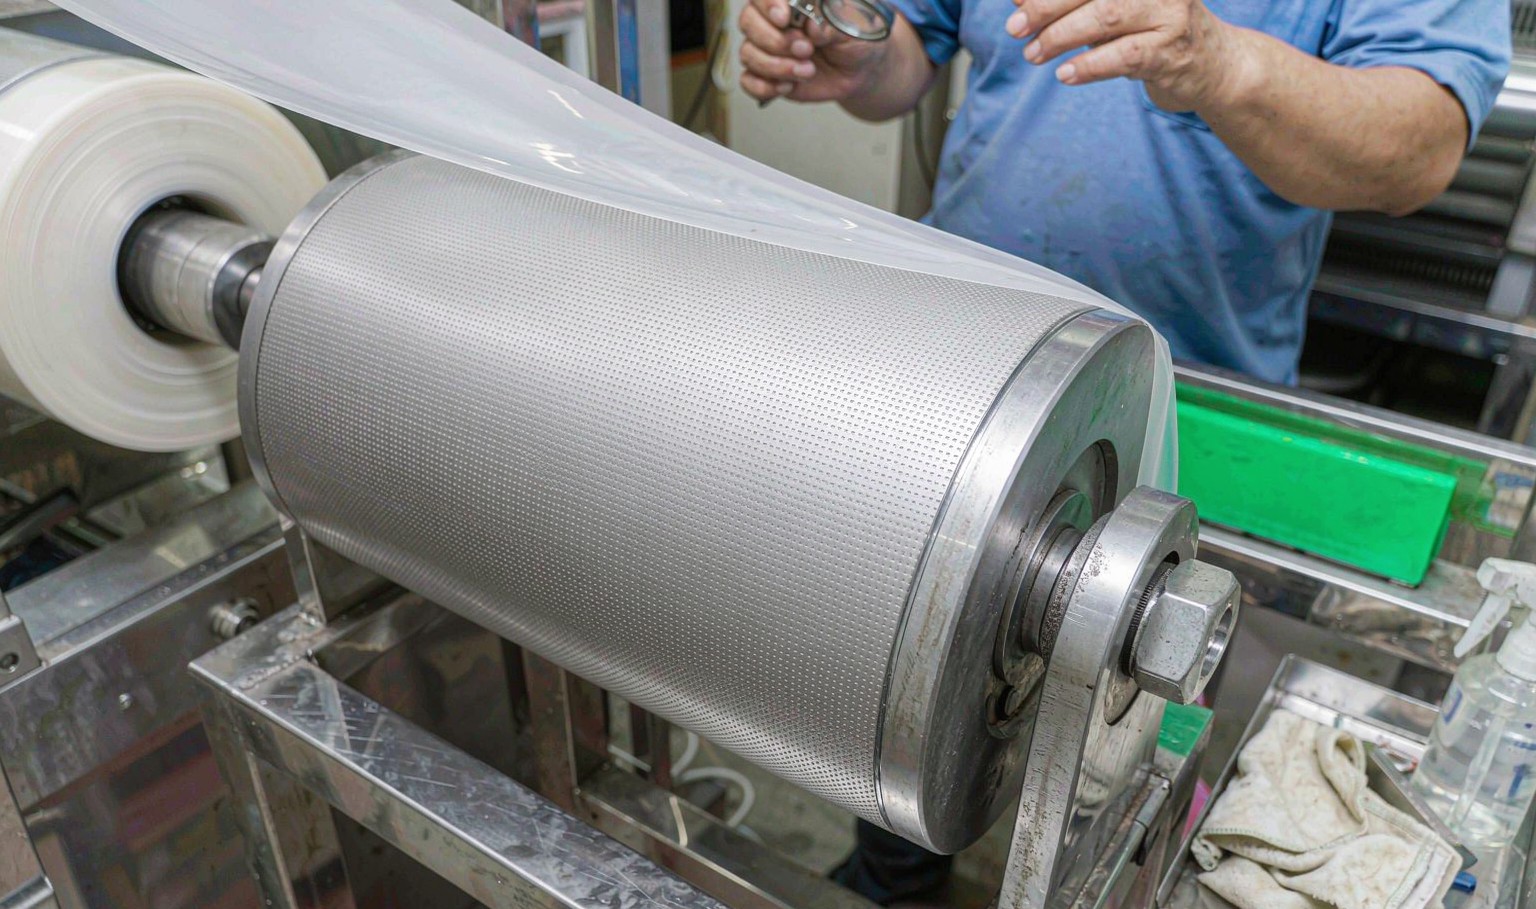
Embossing is a transfer of a surface pattern from a roll into a sheet that is still hot enough to take it. The sheet has to be soft enough to flow into the pattern and cool enough to hold it once it leaves the nip. Those two requirements pull in opposite directions and that is why the process has a window rather than a setting.
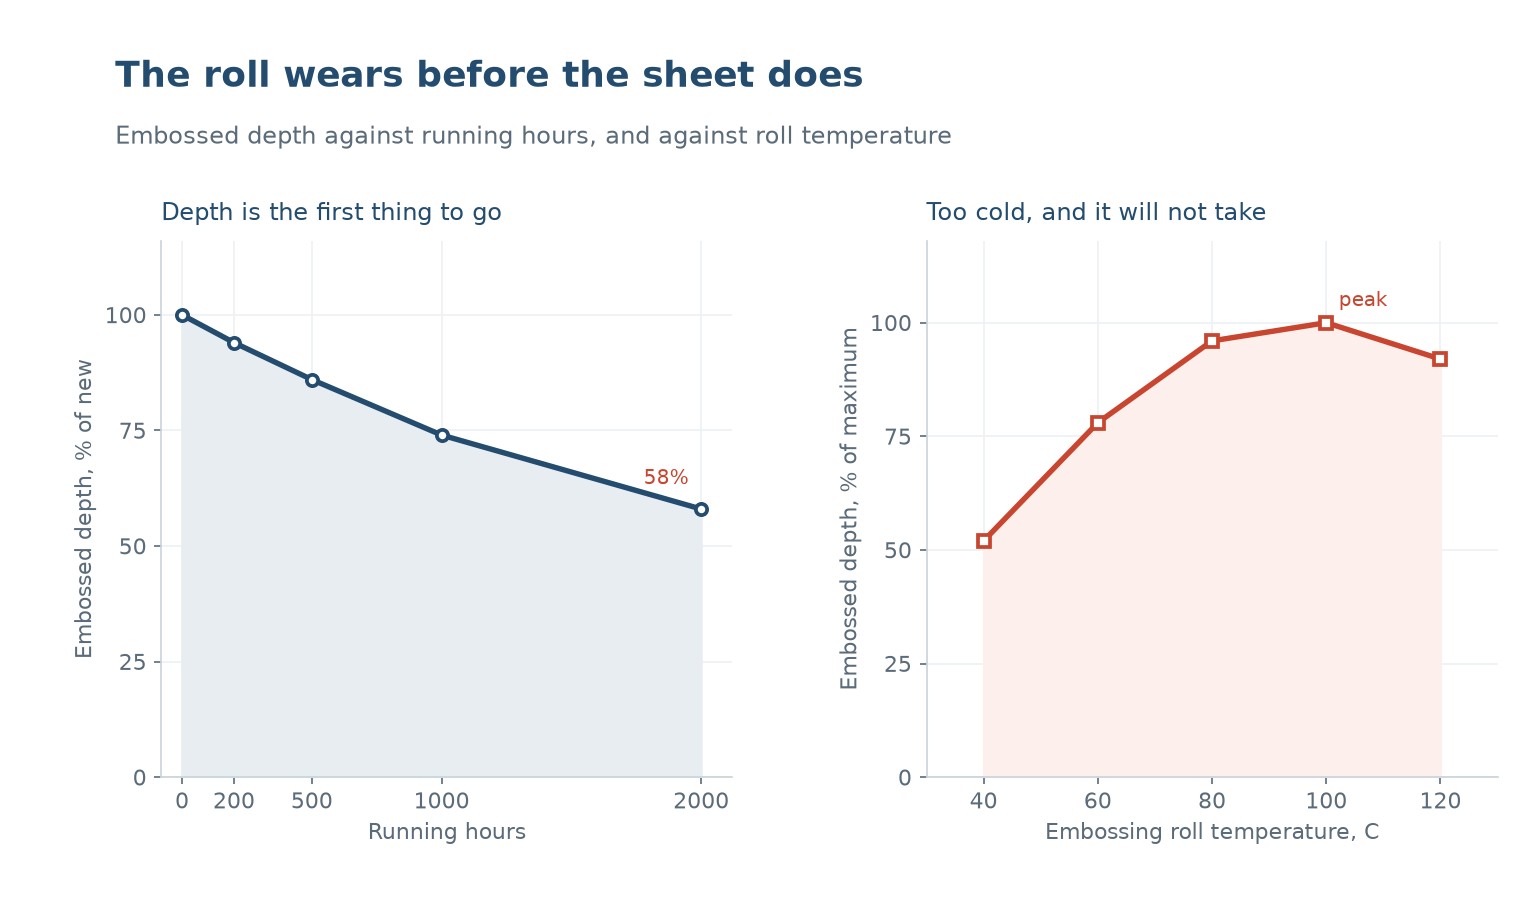
The window is narrow. Running the roll at 40 C gives 52 percent of full depth, because the sheet freezes before it has flowed into the pattern. At 60 C it is 78 percent, at 80 C it is 96, at 100 C it is 100 and at 120 C it is 92, because the sheet is now soft enough that it relaxes back out of the pattern before it sets.
The peak is broad enough to run in but not broad enough to ignore. A roll controlled to plus or minus 3 C around 100 C holds the depth; a roll that drifts 20 C loses 8 percent of the depth on one side of the window and more on the other.
The roll wears before the sheet does
The pattern is a set of fine features on a hard surface being pressed into a soft one at temperature. The soft one is replaced continuously; the hard one is not, and it slowly loses the sharpness of its features. At 200 hours the depth is 94 percent of new, at 500 hours 86, at 1,000 hours 74 and at 2,000 hours 58.
The loss is not uniform. The peaks of the pattern wear first, so the texture does not just get shallower, it gets rounder. A grain that starts as a sharp matte becomes a soft satin, and the change is visible on the part long before the depth number moves much.
This is why a texture specification needs a lower limit as well as a target. A customer who accepts a sample at 100 percent depth and then receives 58 percent at the end of a run has a legitimate complaint, and the fix is either a re-textured roll or a replacement schedule that is planned rather than reactive.
What controls the depth on the line
Nip pressure is the first control, and it is the one most often set by feel. More pressure pushes the sheet further into the pattern, up to the point where the sheet is thinned or the pattern bottoms out. Past that point more pressure does nothing except wear the roll.
Sheet temperature at the nip is the second and it is more important than roll temperature, because the sheet is what has to flow. A line running a hot sheet into a cool roll and a line running a cooler sheet into a hot roll can produce the same depth with very different downstream behaviour.
The third is the rubber backing roll. It has to be compliant enough to let the sheet follow the pattern and hard enough not to deform itself. A backing roll that has gone hard with age stops conforming and the texture becomes patchy across the width.
| Controle | Effect on depth | Typical failure |
|---|---|---|
| Roll temperature | Peaks near 100 C | Drift, uneven across face |
| Nip pressure | Rises then saturates | Set by feel, over-pressed |
| Sheet temperature | Dominant | Line speed changes it |
| Backing roll hardness | Conformity | Hardened with age |
| Roll wear | Falls with hours | Peaks round off first |
Table 1 — The five controls that decide texture depth
Measuring texture so it can be specified
Depth alone is not a specification, because a pattern can keep its depth and lose its sharpness. The useful measurements are depth, gloss and a visual comparison against a retained master sample, and all three should be taken on the same part at the same location.
Gloss is the fastest of the three and the most sensitive to wear, because it responds to the rounding of the peaks rather than to the average depth. A 60 degree gloss reading on a matte texture will move before the depth measurement does, which makes it a good early warning.
The master sample is the one that settles arguments. A physical sample kept in a drawer, dated, and compared under the same light is worth more than any number, because the customer's complaint is usually visual and the number is usually arguable.
Where embossing runs into trouble
Thin sheet is the first limit. Below about 0.3 mm the pattern is deeper than the sheet can carry, and the back face shows the pattern or the sheet is perforated at the peaks. The practical rule is that the pattern depth should be under a fifth of the sheet thickness.
The second is the pattern itself. A deep pattern with sharp edges wears fast and releases badly; a shallow pattern wears slowly and disappears gradually. The design of the pattern is a trade between how it looks on day one and how long it lasts.
The third is downstream. A textured sheet does not print the same as a smooth one, and it does not laminate the same either. A texture chosen for appearance can make the printing operation impossible, and that is discovered after the roll is made.
Keeping a texture consistent over a long run
The first thing is to record the settings that produced the approved sample: roll temperature, nip pressure, sheet temperature at the nip, line speed and backing roll hardness. Those five numbers are the recipe, and without them the sample cannot be reproduced.
The second is to check the roll at intervals, not when a complaint arrives. A gloss reading on a produced part every shift gives a trend, and a trend tells you when to schedule a re-texture instead of discovering it.
The third is to keep a spare roll or to accept a planned stoppage. A roll that is re-textured is out of production for a week or more, and a line that cannot plan for that will run a worn roll until the customer notices.
| Interval | Check | Actie |
|---|---|---|
| Every shift | Gloss on a produced part | Log the trend |
| Weekly | Roll temperature across the face | Balance the zones |
| Monthly | Depth against the master sample | Adjust nip or temperature |
| Yearly | Roll surface inspection | Plan re-texture |
| At 60% depth | Customer notification | Replace or re-texture |
Table 2 — A texture maintenance schedule
Can a worn embossing roll be re-textured?
Usually yes, by stripping the chrome, re-cutting or re-etching the pattern and re-plating. It costs a fraction of a new roll and takes one to three weeks, during which the line needs another roll.
Why does the texture get shallower at the end of a run?
Either the roll is warming up past its window, or the sheet temperature is drifting with line speed. Both look like wear but are settings, and both are cheaper to fix.
Does texture affect the sheet's mechanical properties?
Very little in the plane of the sheet. It does affect the surface energy and therefore printing and laminating, and it can affect the notch sensitivity of a thin sheet at the pattern peaks.
What is the right nip pressure?
The lowest pressure that gives full depth at the set temperature. More pressure wears the roll faster and does not deepen the pattern once the sheet has filled it.
Can the same roll produce different depths?
Yes, within a range, by changing temperature and pressure. That is useful for making a family of textures from one roll, and it is a risk if the settings are not recorded.
How thick must the sheet be for a given pattern?
As a rule, the pattern depth should be less than a fifth of the sheet thickness. Beyond that the back face shows the pattern and the peaks become a perforation risk.
Need a textured sheet that stays consistent?
Send the pattern sample and the sheet specification. We will tell you which depth is achievable, how the roll should be maintained, and what the texture does to printing and laminating.




 NL
 EN
 ES
 FR
 DE
 PT
 AR
 RU
 JA
 KO
 IT
 TR
 PL
 ID
