
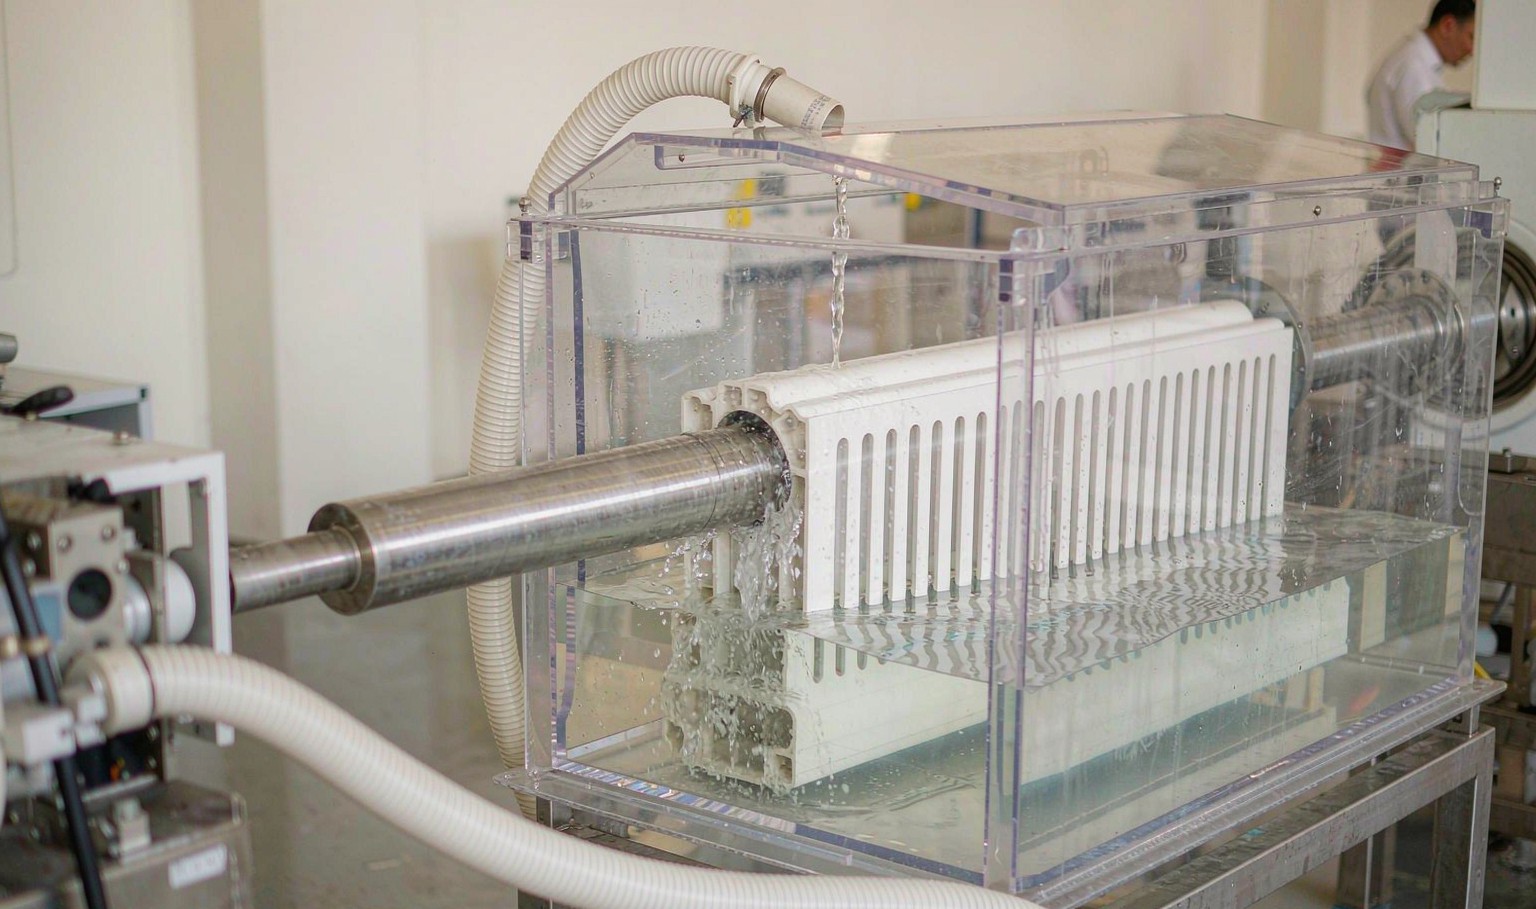
Bow is measured, not eyeballed
A profile that looks straight on a two metre bench can be well outside a straightness specification, because bow is a slow deviation and the eye corrects for it. The measurement is defined: the profile is laid on a flat surface, a straight edge or a tensioned wire is placed along the face being checked, and the maximum gap between the profile and the reference is measured with a feeler gauge or a dial indicator.
The result is expressed as a sagitta over a stated length, then normalised to millimetres per metre. A 3 mm gap over a 3 m length is 1 mm per metre. Specifying straightness without stating the length is meaningless, because the same profile measured over 1 m and over 6 m gives two different numbers and neither is wrong.
Two other defects are often called bow and are not. Twist is a rotation about the longitudinal axis, measured by holding one end and comparing the angle of a face at the other end; it comes from asymmetric flow or from a haul-off that is gripping unevenly. Camber is a lateral bow in the plane of the section rather than perpendicular to it. Both have different causes and neither responds to the fix for bow.
| Measurement | How it is taken | Typical limit |
|---|---|---|
| Bow, vertical | Gap under a straight edge on the face | 1 to 2 mm per metre |
| Bow, lateral | Gap against a wire along the edge | 1 to 2 mm per metre |
| Twist | Angle of a face at 1 m against the same face at the other end | 1 to 3 degrees per metre |
| Total bend over a delivered length | Sagitta over the full length | Stated as an absolute, not a rate |
| Straightness after packing | Re-measured after unpacking | Often one grade looser |
Table 1 — Straightness measurements and the numbers usually quoted for them.
Cooling imbalance does most of it
Polymer shrinks as it cools, and it shrinks in proportion to how much heat it loses. If one face of a profile cools faster than the opposite face, that face contracts first, while the rest of the section is still soft enough to be pulled towards it. The result is a curve, and the curve is set as soon as the section is rigid.
The chart on the left plots bow against the difference between the water temperature at the top of the calibration tank and at the bottom, for a typical rigid PVC window profile. With the tank alone the bow runs 0.3 mm per metre at zero difference, 1.1 at one degree, 2.2 at two, 3.6 at three, 5.2 at four and 7.0 at five. The dashed line is a 2 mm per metre limit, and it is crossed at about 1.8 degrees.
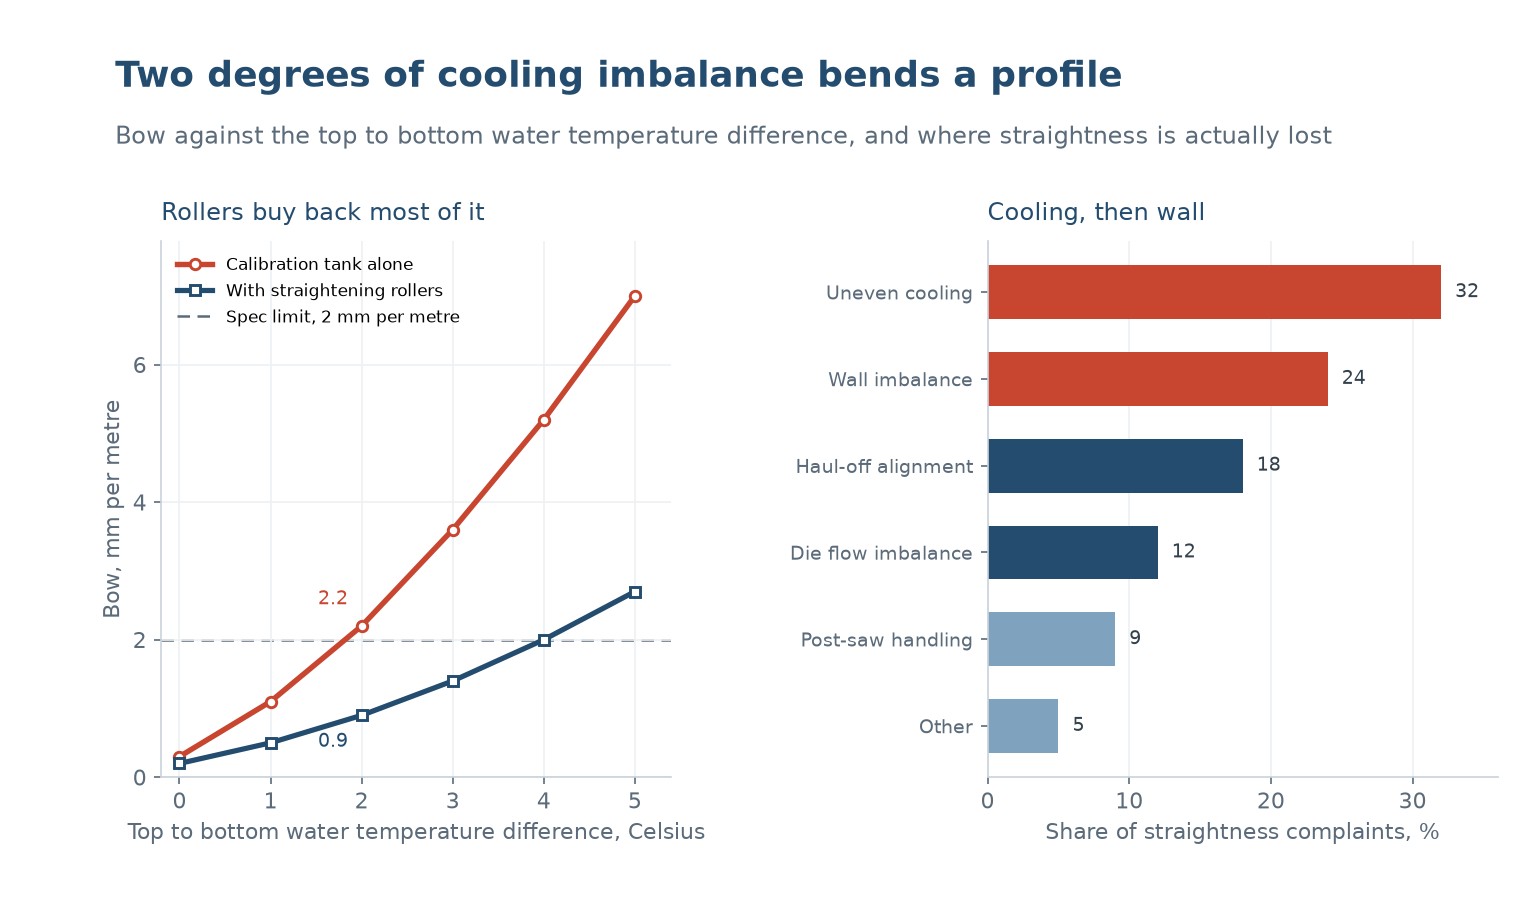
The second curve is the same line with a set of straightening rollers after the tank. At two degrees the bow falls from 2.2 to 0.9 mm per metre, and at five degrees from 7.0 to 2.7. The rollers do not remove the cause; they apply a bending moment while the profile is still warm enough to yield, and they hold it straight until it is fully cool.
That is the reason a straightener is worth having even on a well-controlled line. It buys tolerance that would otherwise have to come from tighter water control, and it absorbs the day-to-day variation in tank temperature that a controller cannot hold perfectly.
The temperature difference itself usually comes from stratification rather than from a controller fault. Warm water rises, the top of the tank runs a degree or two hotter than the bottom, and the profile sits in the middle of that gradient. A circulation pump or a sparge pipe along the tank floor closes the gradient to a few tenths of a degree, which is cheaper than any other fix on this list.
Wall thickness sets the rest
The second cause on the right hand panel is wall thickness imbalance at 24 percent, and it acts through the same mechanism. A wall that is 20 percent thicker on one side holds more heat, cools more slowly, and therefore shrinks later and less. The thin side contracts first and pulls the profile towards it.
The consequence is that a die that is dimensionally correct but flows unevenly will produce a straight profile only by accident. The usual sign is a profile that bows consistently in one direction and cannot be corrected by water temperature, because the imbalance is in the section rather than in the tank.
The check is to cut a section, measure the wall at eight points around the profile, and compare the two sides. A difference above 5 percent of the nominal wall is enough to produce visible bow on a long length, and the fix is die balancing rather than process adjustment.
There is a third effect that is easy to miss: the calibration sleeve itself can introduce asymmetry. A sleeve with a heavier wall on one side, or with cooling channels on one side only, removes heat unevenly and produces bow on a profile whose die is perfectly balanced. The symptom is a bow that reverses when the profile is run in a different sleeve.
Alignment from the die to the saw
Haul-off misalignment accounts for 18 percent of complaints and it produces a distinctive pattern. If the haul-off is not on the extrusion axis, the profile is pulled sideways while it is still soft, and the bow appears in the plane of the misalignment rather than in the plane of the cooling gradient.
The measurement is a string line from the die face to the haul-off centre, checked with a plumb or a laser. A few millimetres over five metres is enough to matter on a thin-walled profile. The tank, the spray cooling section and the haul-off all have to be on that line, and the line has to be checked after any maintenance that moved a unit.
Die flow imbalance at 12 percent is the tooling version of the same problem: the die delivers more material to one side, the melt front is asymmetric, and the resulting section cools asymmetrically even when the tank is perfect. It shows up as a wall thickness difference in the same direction as the bow.
Handling after the saw at 9 percent is the one that is not a process problem at all. A profile stacked while warm, or supported at two points with a long span between them, will bow under its own weight in the packing area. On a warm day a stack that was straight at the saw can be out of tolerance when it is unpacked at the customer.
What to change, in order
The order matters because the cheap fixes are also the effective ones. Start with circulation in the tank, because a stratified tank is common, cheap to fix and responsible for the largest share. Then measure the wall thickness at eight points, because a die imbalance cannot be fixed downstream. Then check alignment. Then consider a straightener.
Only after those four should the specification be questioned. A 1 mm per metre limit on a 6 m length is a 6 mm total deviation, which is achievable on a heavy profile with a straightener and difficult on a thin one at speed. A specification written without reference to what the process can hold becomes a permanent source of rejects.
| Oorzaak | Quick check | Fix |
|---|---|---|
| Stratified tank water | Thermometer at top and bottom of the tank | Circulation pump or sparge pipe |
| Wall thickness imbalance | Section the profile, measure eight points | Balance the die |
| Haul-off off axis | String line from die face to haul-off | Re-align tank and haul-off |
| Asymmetric sleeve cooling | Run the same die in a second sleeve | Replace or rework the sleeve |
| Warm stacking | Measure before and after packing | Cooling conveyor, longer support spacing |
Table 2 — Matching the symptom to the check and the correction.
Straightness has to survive the lorry
A profile that is in tolerance at the end of the line can be out of tolerance at the customer, and the cause is support. A 6 m length of window profile weighs a few kilograms and is stiff enough to hold itself, but a length that is supported at both ends and nothing in between will sag measurably under its own weight over a warm afternoon.
The practical rule is a support every 1.2 m or so for long lengths, with the supports aligned so the profile does not sit on a high point in the middle of a span. Bundles are better than single lengths, because a bundle shares the load, and bundles strapped tightly and stacked flat behave far better than lengths stacked loosely on a stillage.
Temperature matters as much as support. A profile at 40 degrees in a closed container is softer than the same profile at 20 degrees in a warehouse, and the sag over a week of transit can exceed the sag over a month of storage. Shipping in a container that is loaded in the cool part of the day and not left standing on a quay is not a detail.
The final check is to measure a sample after unpacking rather than before packing. It is the only measurement that reflects what the customer receives, and on a profile that is marginal at the saw it is the one that finds the problem before the claim does.
How is bow measured on an extruded profile?
Lay the profile on a flat surface, hold a straight edge or a tensioned wire along the face, and measure the largest gap with a feeler gauge. Divide by the length to get millimetres per metre, and always state the length the measurement was taken over.
What causes an extruded profile to bow?
Uneven cooling across the section is the largest cause, followed by wall thickness imbalance, haul-off misalignment, die flow imbalance and warm stacking. Cooling accounts for roughly a third of complaints in most shops.
How much temperature difference across a calibration tank is acceptable?
About one degree Celsius. A 2 mm per metre limit on a rigid PVC profile is crossed at roughly 1.8 degrees of top to bottom difference, which is why a circulation pump or a sparge pipe along the tank floor is the cheapest fix available.
Do straightening rollers fix bow?
They reduce it substantially rather than eliminating it. At two degrees of tank imbalance, rollers take bow from 2.2 to 0.9 mm per metre. They work by bending the profile while it is still warm enough to yield, so they need the profile to be at the right temperature to be effective.
Why does the bow direction change between production runs?
Usually because the profile was run in a different calibration sleeve, or because the tank water stratification has changed with the season. A bow that reverses with the sleeve points to asymmetric cooling in the sleeve rather than in the tank.
Can bow appear after the profile is packed?
Yes. A long length supported only at its ends will sag under its own weight, especially when warm. Support every 1.2 m or so, bundle rather than stack single lengths, and measure a sample after unpacking rather than at the saw.
A profile that arrives straight
Send the section drawing and the straightness you need, with the length it is measured over. We will tell you what the tank, the sleeve and the haul-off have to do to hold it, and whether a straightener is needed on that shape.




 NL
 EN
 ES
 FR
 DE
 PT
 AR
 RU
 JA
 KO
 IT
 TR
 PL
 ID
