

The problem
Symptom. Goods-in measures the 180 mm flange of a 0.6 mm APET tray at -0.5 mm from nominal, while the supplier's press-side record shows +0.3 mm, both against a +/-0.4 mm tolerance.
What it costs. A 40 000-tray order is held because both sides quote their own measurement, and the contract states no conditioning time, so the batch cannot be accepted or invoiced.
This guide shows how to separate thermal contraction from stress relaxation, then writes a 24 h conditioning period at 23 °C / 50 % RH into the tray drawing's inspection method.
- 1. Why the same tray measures differently at 1 h and 24 h
- 2. Measure the flange at a declared conditioning time and temperature
- 3. Thermal expansion, relaxation and the numbers to specify
- 4. Variables that move the dimension after despatch
- 5. A conditioning clause for the tray drawing and inspection method
- 6. Costing a 2 h anneal against a held tray order
Why the same tray measures differently at 1 h and 24 h
A formed PET tray is not stable at the press. A 180 mm flange still at 32 °C contracts by 0.00007 × 180 × 9 ≈ 0.11 mm cooling to 23 °C; frozen-in orientation stress adds more shrinkage over 24 h.
| What goods-in sees | What is physically happening | First measurement |
|---|---|---|
| In tolerance at press, out at goods-in | Tray still warm and carrying frozen-in stress at 1 h | Flange width at 1 h and 24 h, 23 °C / 50 % RH |
| Reading drifts between two operators | Each side measured at a different conditioning time | Logged measurement time and temperature per reading |
| Good in a dry store, bad in a humid one | Moisture uptake and stress relaxation shift the dimension | Width at 20 % and 50 % RH on the same tray |
| Drift worst on the bottom pallet layer | Sustained stack load adds creep over 24 h | Width by pallet layer after 24 h under 5 kg |
Table 1 - Classifying a conditioning fault before changing the tool
Need a fixed price for this formed tray?
Send the tray drawing, sheet gauge and annual volume. We will review draft, trim and material, then quote a production tool with a written line-acceptance test.
Measure the flange at a declared conditioning time and temperature
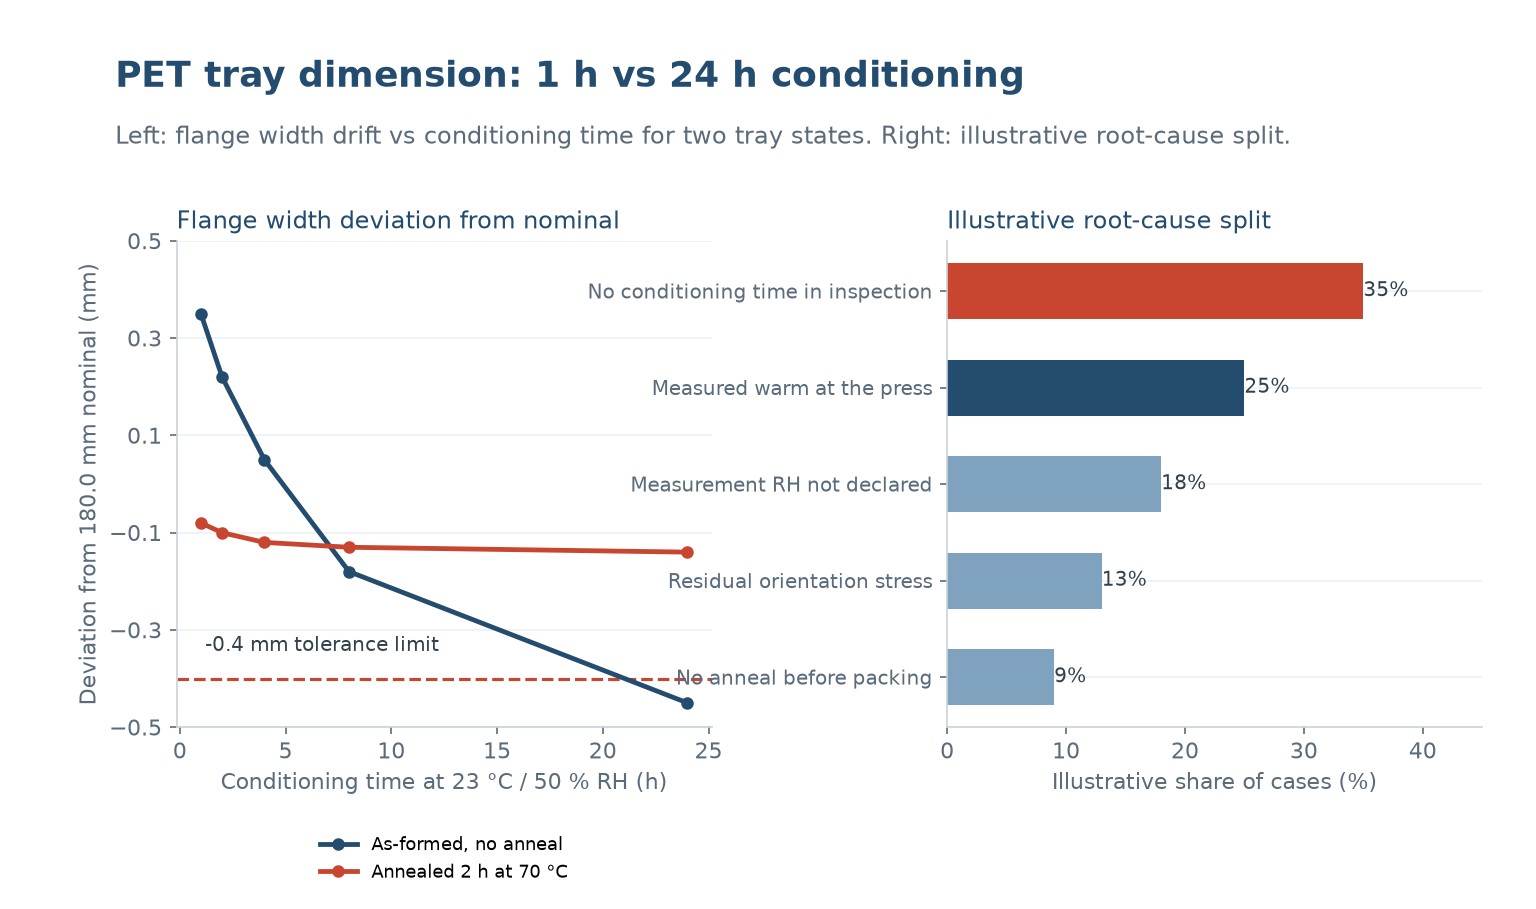
Log the flange width at 1 h and 24 h on the same 30 trays, held at 23 °C / 50 % RH. A representative production tray moves from +0.35 mm to -0.45 mm, a 0.80 mm swing that straddles the +/-0.4 mm band.
A five-step diagnostic sequence
- Mark the sample.
Select 30 trays from one lot and label each with its forming time. - Measure at 1 h.
Record flange width at 23 °C / 50 % RH one hour after forming. - Condition for 24 h.
Hold the trays at 23 °C / 50 % RH for 24 h under a 5 kg top load. - Re-measure.
Repeat the flange reading on the same 30 trays and log the drift in mm. - Qualify the lots.
Repeat across three lots and attach the record to the first-off approval.
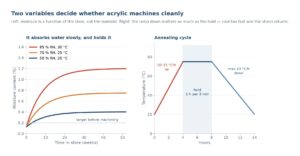
The chart below is a typical result from that measurement step. Use it to separate a design limit from a setting that can still be recovered.
Thermal expansion, relaxation and the numbers to specify
Three numbers belong on the drawing: a nominal 180.0 mm flange with +/-0.4 mm tolerance, a measurement temperature of 23 °C / 50 % RH, and a 24 h conditioning period. An anneal of 2 h at 70 °C holds it to -0.14 mm.
| المعلمة | Typical target | What goes wrong outside it |
|---|---|---|
| Nominal flange width and tolerance | 180.0 mm +/- 0.4 mm | A 0.45 mm drift reads out of tolerance at goods-in |
| Measurement temperature | 23 °C / 50 % RH | A warm 32 °C tray reads 0.11 mm longer |
| Conditioning period before inspection | 24 h at 23 °C / 50 % RH | A 1 h reading cannot be compared with goods-in |
| Anneal to stabilise the tray | 2 h at 70 °C | No anneal leaves -0.45 mm of drift |
Table 2 - Conditioning parameters to write on the tray drawing
Variables that move the dimension after despatch
The dimension moves again after despatch. A carton stored at 30 °C speeds stress relaxation, a pallet under 5 kg loads the lower trays, and a dry warehouse at 20 % RH changes moisture uptake, so re-measure after any storage change.
| Process variable | Effect on the dimension | Practical control |
|---|---|---|
| Tray measured within 1 h of forming | Residual heat and unrelaxed stress inflate the reading | Hold 24 h at 23 °C / 50 % RH before inspection |
| Warehouse at 30 °C | Stress relaxation accelerates and the flange shrinks | Cap storage temperature and log the shipment |
| Store at 20 % RH | Moisture uptake differs from the qualified 50 % RH | Condition and measure at the declared RH |
| Pallet under 5 kg for 24 h | Lower trays creep and lose flange width | Limit layers and re-measure after storage |
Table 3 - Variables that move the dimension after sign-off
A conditioning clause for the tray drawing and inspection method
A gauge reading at the press cannot settle a goods-in argument. Add a clause: flange width judged only after 24 h at 23 °C / 50 % RH, +/-0.4 mm on 180.0 mm, verified on 30 trays from three lots.
Want the tray checked against your line?
Send us the tray drawing and the line conditions. We will flag the geometry and material choices that cause jams, and quote a tool with an acceptance test.
What to send us
- Tray drawing with draft and radii
- Sheet grade and gauge
- Stack depth and line speed
- Drawings of the magazine or denester
Costing a 2 h anneal against a held tray order
A 2 h anneal and a written conditioning method add roughly 1-2 p per tray but remove a held 40 000-tray order. One blocked batch costs more than that allowance across the whole contract, and fixes the inspection method for later lots.
Before you sign off this thermoformed tool
- A 24 h conditioning period at 23 °C / 50 % RH is written into the inspection method
- The nominal 180.0 mm dimension carries an explicit +/-0.4 mm tolerance on the drawing
- The measurement temperature and humidity are stated, not assumed
- The acceptance test covers 30 trays from three lots, not a single press-side part
- An anneal or stress-relief step is specified before the trays are packed
A tray that looks right in the carton can still stop a filling line. Test the stack, not a single part.
Why does the tray pass at the press and fail at goods-in?
Because the part is still warm and stressed at 1 h. A 180 mm flange at 32 °C contracts about 0.11 mm cooling to 23 °C, and stress relaxation adds up to 0.45 mm over 24 h, crossing the +/-0.4 mm band.
Is the tool or the sheet at fault?
Neither, usually. The mechanism is post-forming conditioning, not a forming defect. Section a tray and log flange width at 1 h and 24 h; a steady 0.8 mm drift points to measurement timing.
Can we simply tighten the tolerance?
No. A +/-0.2 mm band would reject good trays too, because the drift is real shrinkage, not scatter. Fix the conditioning time in the inspection method and anneal the tray instead.
Does a 2 h anneal remove the drift?
It holds the flange near -0.14 mm from nominal, inside +/-0.4 mm, by relaxing frozen-in stress before packing. A representative unannealed tray reached -0.45 mm, so the anneal is what makes the clause achievable.
What humidity should goods-in use?
Measure at 23 °C / 50 % RH. A dry 20 % RH store changes moisture uptake and can shift the reading; conditioning at a declared RH makes the buyer and supplier numbers comparable.
What should the inspection clause say?
Flange width of 180.0 mm +/- 0.4 mm judged only after 24 h at 23 °C / 50 % RH, measured on 30 trays from three lots, with the measurement temperature and conditioning time attached to the drawing.
Get a tray that runs on your filling line
Send us the tray drawing or a sample stack. We will review draft, trim and material, then quote a production tool with a measurable line-acceptance test written into it.
To get an accurate quote, send:
- Tray drawing or sample stack
- Sheet material and gauge
- Line speed and denesting method
- Annual volume and target unit price
Request a tool and tray quotation
Why buyers work with Uplastech
ISO 9001, ISO 14001 and ISO 45001 certified. Founded in 2016, with injection moulding lines in Shanghai and an extrusion plant in Jiangsu. Moulding machines from 90T to 1100T and a maximum shot weight of 5100 g. Samples and a written quotation are available on request.

 AR
 EN
 ES
 FR
 DE
 PT
 RU
 JA
 KO
 IT
 NL
 TR
 PL
 ID
