
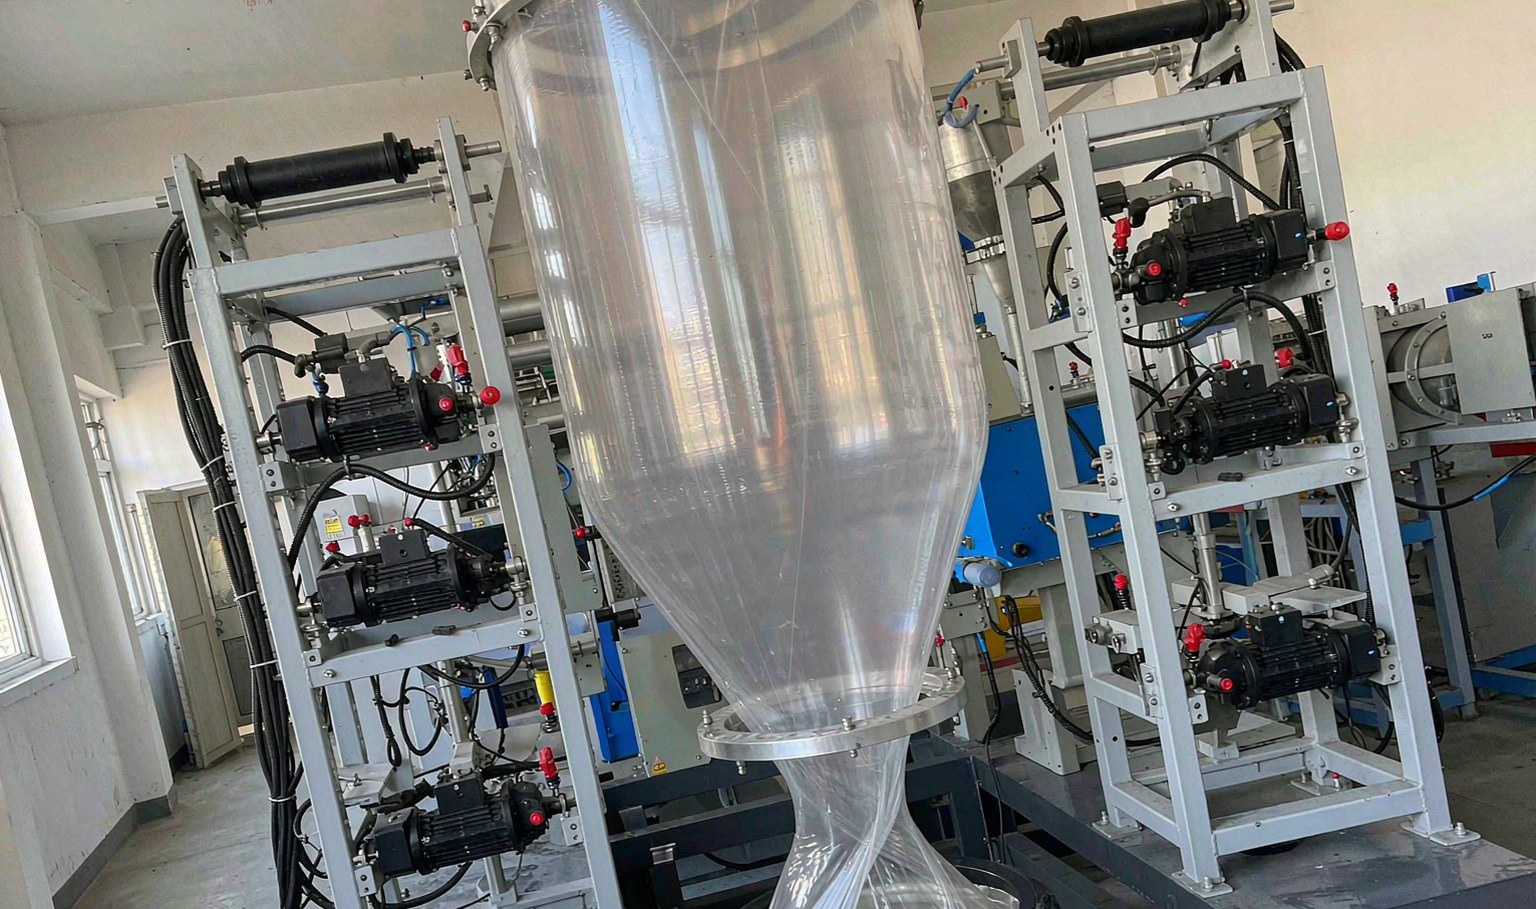
- 1. The bubble is a tension structure, not a balloon
- 2. Bubble instability: the four failure modes
- 3. Frost line height: what it actually controls
- 4. Cooling: the capacity constraint on the whole line
- 5. Gauge variation: where it comes from
- 6. Resins and what each one wants
- 7. Troubleshooting the common faults
- 8. What to specify when buying film
The bubble is a tension structure, not a balloon
Most descriptions of blown film treat the bubble as something inflated. It is more useful to think of it as a tension structure. The film leaving the die is pulled upward by the nip rolls at a fixed speed, and the air trapped inside sets how far the film can move outward as it travels. The bubble shape is the equilibrium between those two forces.
Three numbers define the process:
Blow-up ratio (BUR) — bubble diameter divided by die diameter. Typically 2:1 to 4:1. Higher BUR gives more transverse orientation and better transverse tear strength.
Draw-down ratio (DDR) — die gap divided by finished film thickness, adjusted for BUR. Typically 20:1 to 60:1 for thin film. Higher DDR gives more machine-direction orientation.
Frost line height (FLH) — the distance from the die to the point where the film crystallises and turns hazy. This is where the film stops deforming and its properties are locked in.
The one thing to understand: frost line height is a result, not a setting. You cannot dial it in directly. You change it by changing cooling air volume, melt temperature, or line speed — and then you read where it landed. Operators who talk about "setting the frost line" are really talking about setting the cooling.
Bubble instability: the four failure modes
A blown film bubble that will not stay put is the defining problem of the process, and it has four distinct forms. Diagnosing which one you have is most of the work.
| Instability | What it looks like | Root cause | First fix |
|---|---|---|---|
| Draw resonance | Regular, periodic oscillation in bubble diameter and gauge, like a heartbeat | Draw-down ratio too high for the melt strength; the system is in a limit cycle | Reduce DDR (thicker film or larger die gap) or lower melt temperature |
| Helical instability | Bubble rotates slowly around its axis, leaving a spiral gauge pattern | Non-uniform cooling air around the circumference, or a die temperature gradient | Check air ring balance and die zone temperatures |
| Bubble flutter | High-frequency wobble, usually near the frost line | Turbulent cooling air or a draft in the plant | Reduce air velocity, shield the bubble from air movement |
| Bubble burst | Sudden rupture, usually at the frost line | Contamination, gel, or a local thin spot; sometimes over-pressure | Check resin for contamination, check die lip for damage |
Table 1 — The four bubble instabilities. Draw resonance and helical instability are process problems; flutter and burst are usually environmental or material problems.
Draw resonance is the one that defeats people because it looks like a machine fault. It is a genuine hydrodynamic instability: above a critical draw ratio the extensional flow becomes unstable and the bubble oscillates between two diameters. It is more likely with high melt strength resins and less likely with LLDPE, which is one reason LLDPE dominates the market.
Frost line height: what it actually controls
Everything about film properties passes through the frost line. Below it the film is molten and being stretched; above it the film is solid and its structure is fixed. Where the line sits determines how much orientation you get, how the crystal structure forms, and how the film behaves on the roll.
| Frost line | Effect on film | When to use it |
|---|---|---|
| Low (short) | Rapid quench, fine crystals, high clarity, high gloss, lower tear strength | Clarity films, thin film, high output |
| Médio | Balanced clarity and toughness | General purpose packaging |
| High (long) | Slow cooling, coarse crystals, hazy, tougher, better bubble stability | Heavy duty bags, shrink film, high-strength applications |
Table 2 — Frost line height as a property lever. The same resin can produce a clear film or a hazy tough film depending only on where the frost line sits.
On a typical LDPE or LLDPE line running 40 µm film, the frost line sits at 150–300 mm above the die. On a high-output line with internal bubble cooling it can be pushed to 600 mm or more, because the extra cooling allows a longer molten zone without the bubble becoming unstable.
The frost line is not flat. On a poorly balanced air ring it is higher on one side than the other, which produces a gauge band that runs helically up the bubble. This is the most common cause of the "spiral gauge" defect and it is nearly always an air ring or die temperature problem, not a resin problem.
Cooling: the capacity constraint on the whole line
Blown film output is limited by cooling, not by the extruder. The extruder can melt far more resin than the air ring can cool, so the line runs at whatever rate the cooling allows.
| Método de arrefecimento | Heat transfer | Output gain | Complexidade |
|---|---|---|---|
| Single-lip air ring | Baseline | — | Baixa |
| Dual-lip air ring | Higher, better velocity profile | +15 – 25% | Baixa |
| Dual-lip + chilled air | Higher still | +20 – 30% | Médio |
| Internal bubble cooling (IBC) | Cooling from inside and outside | +40 – 70% | High; needs bubble diameter control |
| IBC + chilled air + high stack | Maximum | +80 – 100% | Very high |
Table 3 — Cooling options and the output they unlock. IBC is the single biggest output upgrade available on a blown film line, and also the one most likely to be badly installed.
Air ring design matters more than air volume. A poorly designed ring can deliver a lot of air at the wrong velocity profile and actually destabilise the bubble. The good rings deliver a high-velocity stream at the base of the bubble and a lower-velocity stream further up, so the film is cooled fast where it is hottest and gently where it is already setting.
Gauge variation: where it comes from
Blown film gauge varies in two directions — around the circumference and along the length — and the causes are different.
| Variation | Pattern | Causa |
|---|---|---|
| Circumferential, random | Thick and thin bands at fixed angular positions | Die lip eccentricity, die temperature gradient, air ring imbalance |
| Circumferential, helical | Bands that spiral up the bubble | Rotating air ring imbalance or oscillating die |
| Longitudinal, periodic | Gauge cycles along the roll | Screw pulsation, haul-off variation, draw resonance |
| Longitudinal, drift | Slow change over hours | Screen pack loading, temperature drift, resin lot change |
Table 4 — Gauge variation patterns and their causes. Helical variation is the signature of a rotating element that is out of balance.
Automatic gauge control on a blown film line works by rotating the die or the air ring so that the thick and thin bands are distributed around the roll rather than lining up. This does not reduce the variation at any single point — it averages it out across the wound roll, which is what the converter downstream actually cares about.
Resins and what each one wants
| Resin | Melt temp (°C) | Typical BUR | Characteristic behaviour |
|---|---|---|---|
| PEBD | 160 – 190 | 2.0 – 2.5 | Very stable bubble, low strength, good clarity |
| PEBDL | 190 – 220 | 2.5 – 3.5 | Tougher, needs higher melt temp, less draw resonance |
| PEAD | 190 – 220 | 3.5 – 5.0 | High stiffness, narrow stable window, needs high BUR |
| mLLDPE | 190 – 215 | 2.5 – 3.5 | Excellent toughness, narrow processing window, prone to flutter |
| PP | 210 – 240 | 1.5 – 2.5 | Low melt strength, difficult bubble, usually water quenched |
| PA (nylon) | 240 – 270 | 2.0 – 3.0 | Needs drying, high melt strength, used in multilayer |
| EVOH | 210 – 230 | 2.5 – 3.5 | Barrier layer, very moisture sensitive, always buried in multilayer |
Table 5 — Resins used in blown film. HDPE is the one that most often defeats a line set up for LDPE, because its stable BUR window barely overlaps.
Most commercial blown film is not a single resin. A three-layer coex line running LDPE / tie / EVOH / tie / LDPE is standard for barrier packaging, and the layer ratio matters as much as the total thickness. A 5% EVOH layer at 40 µm total gives a 2 µm barrier layer, which is enough for most food packaging but not for retort.
Troubleshooting the common faults
| Fault | Likely cause | Check |
|---|---|---|
| Bubble will not start | Melt too cold, or air escaping at the die | Melt temperature; die face cleanliness; air seal |
| Bubble collapses at the nip | Too much air, or film too hot at the nip | Internal air volume; frost line too high |
| Film blocks on the roll | Too hot at winding, or no anti-block | Nip temperature; slip and anti-block additives |
| Gels and fisheyes | Contamination, degraded resin, die build-up | Screen pack; die lip; purge history |
| Wrinkles at the collapse frame | Collapse geometry wrong for the BUR | Collapse frame angle and width; bubble diameter |
| Thin spots at the seam | Die lip damage or a cold slug | Die lip inspection |
| Poor clarity | Frost line too high, or wrong resin | Cooling air; consider a nucleating agent |
| Low tear strength in MD | Excessive draw-down | DDR; consider reducing line speed or increasing die gap |
Table 6 — Common blown film faults. The blocking fault is a chemistry problem disguised as a mechanical one; check the slip additive before you touch the winder.
The collapse frame deserves a mention because it is where most wrinkles originate. The bubble has to go from a cylinder to a flat lay-flat tube without creasing, and the geometry that achieves this depends on the blow-up ratio. A frame set up for 2.5:1 will wrinkle a 4:1 bubble. Most modern lines have adjustable collapse frames for exactly this reason.
What to specify when buying film
If you are sourcing blown film rather than making it, the specification should cover: resin type and density, total thickness with tolerance (typically ±8% for blown film, wider than sheet), BUR used if it affects properties, treatment level if the film will be printed (38–42 dyne/cm is standard for PE), slip and anti-block levels, and the intended conversion process.
The treatment level is the one that gets omitted and then causes problems. A PE film that measures 32 dyne/cm will not hold ink, and no amount of printing pressure fixes it. Ask for the dyne value and ask how long after treatment it was measured, because corona treatment decays.
What is the difference between blown film and cast film?
Blown film extrudes a tube upward and inflates it, then collapses it into a lay-flat tube. Cast film extrudes through a flat die onto a chilled roll. Blown film gives balanced properties in both directions and is more economical at moderate volumes; cast film gives better clarity, higher output and much higher machine-direction orientation, and is used for stretch film and high-clarity packaging.
Why does my bubble keep bursting?
Usually contamination — a gel or a piece of unmelted resin creates a local thin spot that fails under the draw. Check the screen pack and the resin source first. If the resin is clean, look at the die lip for damage and at the air ring for a localised cold spot that is creating a thin band.
What is draw resonance and how do I stop it?
It is a periodic oscillation in bubble diameter caused by the extensional flow becoming unstable above a critical draw-down ratio. The fix is to reduce the draw ratio — thicker film, larger die gap, or lower line speed — or to use a resin with higher melt strength. It is much more common on HDPE and PP than on LLDPE.
How high should the frost line be?
As high as the cooling allows without destabilising the bubble. For clarity you want it low; for toughness and bubble stability you want it high. On a standard LDPE line running 40 µm it usually lands at 150–300 mm; with internal bubble cooling it can be 600 mm or more.
What is internal bubble cooling and is it worth it?
IBC circulates cooled air through the inside of the bubble, roughly doubling the cooling capacity and allowing 40–70% more output from the same extruder. It is the single biggest output upgrade available. It is also the upgrade most often installed badly, because the bubble diameter control that IBC requires is a control problem, not a plumbing problem.
Why is my film hazy?
Frost line too high, which lets large crystals form, or the wrong resin grade. Clarity grades of LDPE and LLDPE exist for exactly this. Adding a nucleating agent and dropping the frost line will usually get you most of the way there.
Can blown film be made from recycled resin?
Yes, up to 30–50% depending on the application and the quality of the recyclate. The limits are gel content, colour and odour. Recycled LDPE from post-consumer film is commonly used in refuse bags and construction film, where clarity and gel count are not critical.
What BUR should I use?
It depends on the resin and the property balance you need. LDPE runs at 2.0–2.5, LLDPE at 2.5–3.5, HDPE at 3.5–5.0. Higher BUR improves transverse tear strength and impact; lower BUR improves machine-direction strength and output. Most lines are set for the resin, not optimised per job.
Sourcing blown film or multilayer barrier film?
Tell us the resin structure, total thickness, width, treatment level and the conversion process it is going into. We will come back with a film construction and a tolerance band that matches how it will actually be used.
Continue reading
- Plastic Sheet Extrusion: Roll Stack, Polishing and Thickness Control
- Melt Pump and Screen Changer: Why Pressure Stability Beats Temperature
- Co-Extrusion Profiles: Dual Durometer, Tri-Extrusion and Bonding
- Plastic Packaging Tube Extrusion: From Die to Finished Tube
- Plastic Drying Before Extrusion: Hygroscopic vs Non-Hygroscopic Resins




 PT
 EN
 ES
 FR
 DE
 AR
 RU
 JA
 KO
 IT
 NL
 TR
 PL
 ID
