

Why two polymers will not bond
Adhesion between two polymer layers comes from chain entanglement across the interface. For that to happen, the two materials have to be mutually soluble at the interface, which means they need similar polarity and similar solubility parameters. Polyethylene and polyamide do not, so they slide apart.
A tie layer, also called a bonding or adhesive resin, is a polymer that is compatible with both. It is usually a polyolefin grafted with maleic anhydride, which reacts with the amine groups in a polyamide or the hydroxyl groups in EVOH while its polyolefin backbone entangles with the polyethylene.
That means the tie layer is not glue. It is a third material that has to be coextruded at the right temperature, in the right thickness, and in contact with both surfaces while they are still molten enough to entangle. All three conditions have to hold at once.
The consequence is that delamination is almost never a single cause. It is a combination of a thin tie layer, a temperature mismatch and a line speed that does not allow time for the interface to develop. Changing one without the others rarely fixes it.
The tie layer has a window, not a minimum
The chart on the left plots peel strength against tie layer thickness for three material pairs. For PE to PA, the peel strength rises from 1.8 N per 15 mm at 10 micrometres to 6.2 at 40, then flattens and begins to fall slightly at 80.
The rise is easy to explain: more tie layer means more interfacial area and more chance of a continuous bond. The plateau is less obvious but just as real. Once the tie layer is thick enough to be continuous, adding more does not increase the number of bonds, and the extra material becomes a weak layer in its own right.
The fall at high thickness is a mechanical effect. A thick, soft tie layer deforms under peel load, and the failure moves from the interface into the tie layer itself, which has a lower cohesive strength than the bond it was making. The measured peel strength therefore drops even though the bond is intact.
In practice the target is 20 to 40 micrometres for most structures, and the tolerance matters more than the target. A tie layer specified at 30 micrometres but running at 12 because of a feed screw error is the most common cause of delamination in an otherwise correct structure.
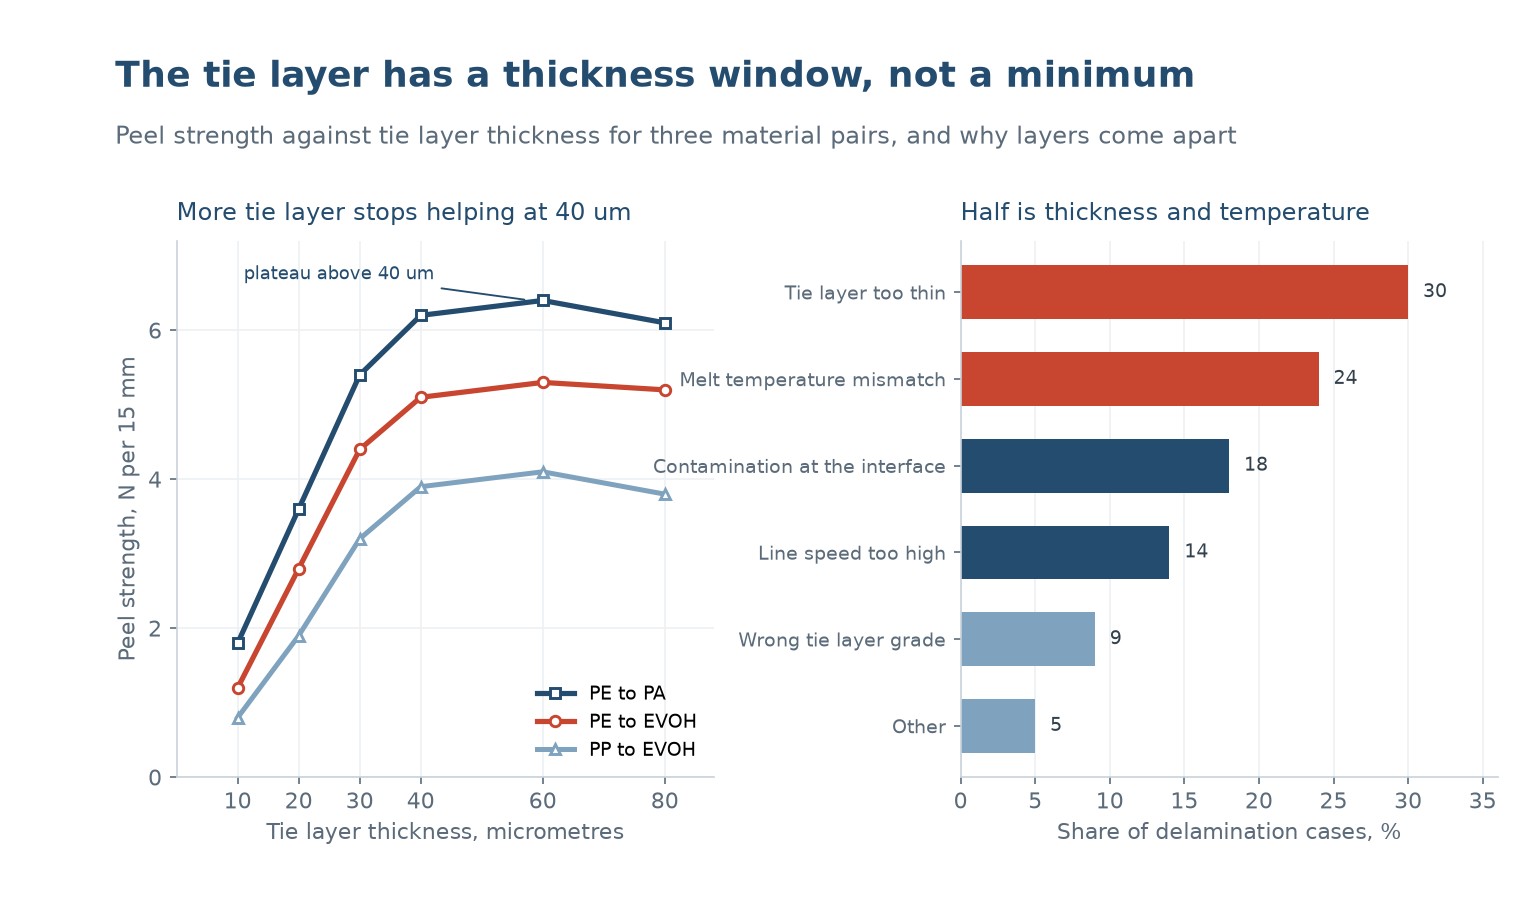
Temperature mismatch is the second cause
The interface bonds while both materials are molten. If one stream is 30 C cooler than the other, it has a higher viscosity and a skin has already formed by the time they meet, and the chains cannot entangle across that skin.
The rule is to match the melt temperatures at the die, not in the extruders. Two streams can leave their extruders at very different temperatures and arrive at the die at the same temperature, or the reverse, depending on the adapter and feed block design. The measurement has to be taken at the die, not at the barrel.
The temperature also affects the flow distribution. A cooler stream is more viscous, so it flows more slowly and occupies a thinner layer than its feed rate suggests. The layer thickness in the product is therefore a function of temperature as well as of feed rate, which is why a temperature change can cause a delamination that looks like a thickness problem.
The practical check is a cross section. Cut the product, polish the edge and measure the layers under a microscope. If the tie layer is thinner than the feed rate predicts, the temperature or the viscosity is wrong, not the metering.
Line speed and residence time
The interface needs time at temperature to develop. A line running at twice the speed has half the time between the die and the cooling rolls, and the bond has less opportunity to form. That is why a structure that bonds at 20 m per minute can delaminate at 40 on the same line with the same settings.
The interaction with temperature is direct: a hotter melt has a longer time before it solidifies, so it tolerates a higher line speed. That is why raising the die temperature sometimes fixes a delamination that appears only at high output, and why lowering it can cause one at the same speed.
The cooling rate matters as well. Fast cooling freezes the interface before it has developed, and slow cooling allows crystallisation to occur at the interface, which can either improve or weaken the bond depending on the pair. For PE to PA, slow cooling usually improves adhesion; for some EVOH structures it does not.
Testing adhesion on the line
The standard test is a peel test at 90 or 180 degrees on a strip cut across the layers, reported in newtons per 15 mm. It is destructive and slow, and it is the only way to know what the bond actually is.
For routine control, a hand peel at the end of a roll is enough to detect a gross problem. If the layers separate cleanly with no resistance, the bond has failed; if the material tears instead of peeling, the bond is stronger than the tie layer, which is the correct outcome.
The failure mode is as informative as the number. A clean interfacial failure means the bond did not form. A cohesive failure inside the tie layer means the bond is good and the tie layer is the weak link, which points to thickness or grade. A mixed failure means both are marginal.
| Failure mode | Meaning | First check |
|---|---|---|
| Clean interfacial peel | No bond formed | Temperature and thickness |
| Cohesive in the tie layer | Bond good, tie layer weak | Tie layer grade and thickness |
| Cohesive in the substrate | Bond stronger than the material | Correct, no action |
| Mixed | Both marginal | Temperature first, then thickness |
| Bond good then fails in service | Ageing or moisture | Hydrolysis resistance of the tie layer |
Table 1 — Reading the peel failure mode
Fixing a delamination
Start with the cross section, because it separates a thickness problem from a temperature problem in one observation. If the tie layer is thinner than specified, the problem is metering or viscosity. If it is the right thickness and the bond is still weak, the problem is temperature or time.
Then check the die temperatures, not the extruder temperatures. A difference of more than 10 C between the streams at the die is enough to cause a weak bond, and it is invisible on the extruder control panel.
Then check the line speed against the temperature. If the bond is good at low speed and poor at high, the interface is not getting enough time, and the answer is either more temperature or less speed.
Finally check the material. A tie layer has a shelf life, and a moisture sensitive grade that has absorbed water will not bond. Drying the tie layer resin, which is often overlooked because it is a small fraction of the structure, fixes a surprising number of cases.
| Change | Effect | Koszt | Ryzyko |
|---|---|---|---|
| Increase tie layer to 30 um | Strong improvement | Materiał | None |
| Match die temperatures within 10 C | Strong improvement | Energy | None |
| Reduce line speed 20 % | Moderate improvement | Output | None |
| Dry the tie layer resin | Fixes moisture cases | Dryer | None |
| Change tie layer grade | Depends on the pair | Material, requalification | Needs testing |
Table 2 — Options in the order they should be tried
The order matters because the first three cost almost nothing and fix most cases. Changing the tie layer grade is the last resort, and it should only follow a peel test that shows a cohesive failure in a correctly thick, correctly tempered layer.
Designing the structure around the bond
Every interface in a multilayer structure is a potential failure. A five layer film with two tie layers has four interfaces, and the weakest one decides the performance. Adding a layer to improve a property adds an interface to control.
The tie layer should be adjacent to the material it bonds to, and the two should be processed at compatible temperatures. Putting a high temperature polymer next to a low temperature tie layer forces a compromise that usually favours the high temperature side, and the bond suffers.
Regrind is the other design decision. A trim regrind that contains all the layers cannot be put back into a single layer without carrying the interface problem with it. It goes into a core layer, where its own internal interfaces are dispersed, and even then it reduces the bond strength at the adjacent interfaces.
Why do my coextruded layers separate?
Usually one of three things: the tie layer is too thin, the melt temperatures at the die do not match, or the line is running too fast for the interface to develop. Check the cross section first, then the die temperatures.
How thick should a tie layer be?
Twenty to forty micrometres for most structures. Below 20 the bond is incomplete; above 40 the extra material becomes a weak layer and the peel strength stops improving and then falls.
Can PE and PA be coextruded without a tie layer?
Not with useful adhesion. They are mutually insoluble, so no chain entanglement occurs across the interface. A maleic anhydride grafted polyolefin tie layer is the standard solution.
Does line speed affect adhesion?
Yes. The interface needs time at temperature to develop, and doubling the speed halves that time. A structure that bonds at 20 m per minute can delaminate at 40 with the same settings.
What does a cohesive failure mean?
That the bond is stronger than the tie layer itself, so the failure happened inside the material rather than at the interface. That is the correct outcome for a peel test, and it means the bond is not the weak link.
Why does the tie layer need drying?
Most tie layer grades are moisture sensitive. A resin that has absorbed water will not bond properly, and because the tie layer is a small fraction of the structure it is often the last thing anyone thinks to dry.
Layers coming apart?
Send the structure, the tie layer grade and a photograph of the peel failure. We will tell you whether it is thickness, temperature or time.




 PL
 EN
 ES
 FR
 DE
 PT
 AR
 RU
 JA
 KO
 IT
 NL
 TR
 ID
