
What a post-cure actually does
A press-cured silicone part is cured enough to be handled, not cured enough to be finished. Two things are still wrong with it. It contains volatile material, which is unreacted low-molecular-weight polymer and the fragments of any peroxide, and its network is not fully developed, so its compression set is higher than it will be after a few hours at temperature.
A post-cure is a second, longer bake in an oven without pressure. It drives off the volatiles and completes the crosslinking, and it changes three properties: the volatile content, the compression set, and the hardness, which rises slightly as the network tightens.
It is required for anything that touches food, skin or a patient, because the volatiles are the extractables that a compliance test looks for. It is also standard for optical parts, because the volatiles fog a lens, and for thick parts, because the press cure cannot reach the core.
Volatiles leave fast, then slowly
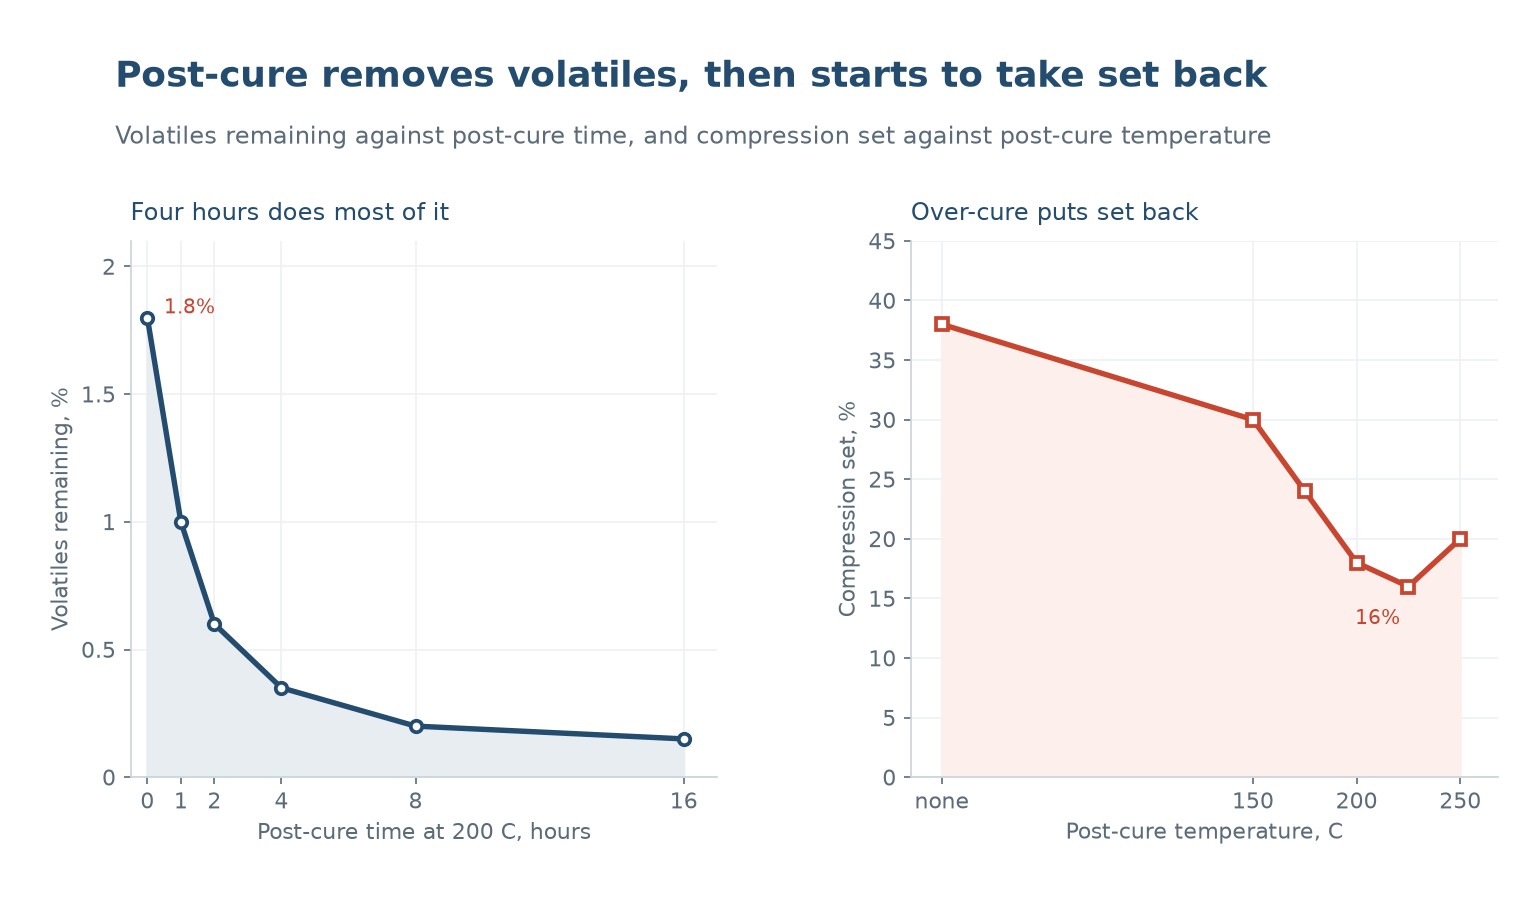
At 200 C the volatile content falls from 1.8 percent in the as-cured part to 1.0 after one hour, 0.6 after two, 0.35 after four, 0.2 after eight and 0.15 after sixteen. The first four hours remove 80 percent of what is removable, and the rest is a slow diffusion tail.
The shape of the curve is set by diffusion, not by reaction. The volatiles near the surface leave quickly and the ones in the middle have to travel out through the rubber, and that path lengthens as the concentration gradient flattens. That is why a thick part needs much longer than a thin one at the same temperature.
The practical schedule for a thin part is four hours at 200 C, which takes the volatile content below 0.5 percent, the level most compliance tests accept. A thick part of 10 mm or more needs eight to sixteen hours, or a higher temperature with the risk of over-cure on the surface.
| Post-cure at 200 C | Volatiles | Removed | Typical use |
|---|---|---|---|
| None | 1.8 percent | 0 | Mechanical parts only |
| 1 hour | 1.0 percent | 44 percent | Handling |
| 2 hours | 0.6 percent | 67 percent | General purpose |
| 4 hours | 0.35 percent | 81 percent | Food and medical |
| 8 hours | 0.20 percent | 89 percent | Thick sections |
| 16 hours | 0.15 percent | 92 percent | Optical, critical |
Table 1 — Volatile content against post-cure time at 200 C.
Set falls, then rises
Compression set improves with post-cure temperature and then gets worse. With no post-cure the set is 38 percent, at 150 C it is 30, at 175 C 24, at 200 C 18 and at 225 C 16. At 250 C it climbs back to 20.
The improvement is the network completing. The reversal is degradation: at 250 C the polymer chains start to break as fast as they crosslink, and the network that results is less able to recover. The material also discolours and its tear strength falls, which is why a post-cure above about 230 C is a specialist operation rather than a default.
The optimum is material-specific. A general-purpose HCR peaks around 200 to 225 C; a high-temperature grade can go to 250 without reversing, and a fluorosilicone is more sensitive. The compound data sheet usually gives a recommended post-cure, and it is worth following rather than inventing a schedule.
The oven and the fixture
A post-cure oven needs forced air and a uniform temperature, because a 10 C gradient across the chamber produces a 10 C difference in set across the batch. A laboratory oven with a fan and a calibrated controller is adequate; a home-made cabinet with a thermostat is not.
Ventilation matters as much as temperature. The volatiles have to leave the oven, or they re-deposit on the parts as an oily film. A through-flow oven with an extraction duct is the right arrangement, and the duct should be sized for the volatile load rather than for the oven volume.
Parts are usually post-cured loose on a perforated tray, in a single layer, because stacking traps volatiles between parts. A part that has to hold a dimension during the post-cure goes on a fixture, because the material softens at the post-cure temperature and will sag under its own weight.
What else changes
Hardness rises by 2 to 5 Shore A during a post-cure, because the network tightens and the volatiles leave. A compound specified at 50 Shore A can come out at 53, and if the tolerance is plus or minus 3 that is the whole allowance.
Dimensions shrink by 0.2 to 0.5 percent, for the same reason. On a moulded part with a tight dimension the shrinkage has to be allowed for in the tool, or the part has to be post-cured on a fixture that holds the dimension.
| Proprietà | Change after post-cure | Perché |
|---|---|---|
| Hardness | +2 to 5 Shore A | Network tightens as volatiles leave |
| Dimensioni | -0.2 to 0.5 percent | Same shrinkage |
| Compression set | Falls by 15 to 20 points | Crosslinking completes |
| Colour | Slightly darker | Thermal history |
| Tear strength | Unchanged below 230 C | Degradation above it |
Table 2 — What a post-cure changes, and by how much.
Colour changes slightly, usually a little darker or yellower. On a white or a translucent part this is visible, and it is the reason a post-cured part and an as-cured part should never be mixed in one assembly.
What to specify
A post-cure is a process specification, and it belongs on the drawing when the part has a compliance or a set requirement.
- Post-cure temperature and time, with the tolerance on both.
- Whether the part is supported during the post-cure.
- The volatile content or extractable limit the part has to meet.
- Compression set at the service temperature, after post-cure.
- Hardness after post-cure, not before, if the tolerance is tight.
- Whether the oven is through-flow and extracted.
Hardness after post-cure is the item that catches people out. A drawing that specifies 50 Shore A and a process that post-cures to 53 produces parts that fail an incoming inspection while being perfectly good parts.
Why is silicone post-cured?
To drive off volatiles and complete the crosslinking. It lowers the extractables, improves compression set and stabilises the hardness, and it is required for food, medical and optical parts.
How long should a silicone post-cure be?
Four hours at 200 C for a thin part, which takes volatiles below 0.5 percent. Thick sections need eight to sixteen hours.
Does post-cure improve compression set?
Yes, up to a point. Set falls from 38 percent with no post-cure to 16 percent at 225 C, then rises again at 250 as degradation starts.
Does post-cure change hardness?
It raises it by 2 to 5 Shore A and shrinks the part by 0.2 to 0.5 percent. Specify hardness after post-cure, not before.
Why did my parts sag in the post-cure oven?
Because they were unsupported. The material softens at the post-cure temperature, so parts that must hold a shape need a fixture.
Can a post-cure be done in any oven?
It needs forced air, a uniform temperature and extraction for the volatiles. A cabinet with a thermostat will give uneven set and re-deposit volatiles on the parts.
Need a silicone part with a set or extractable limit?
Tell us the service temperature and the compliance test. We will quote the post-cure schedule and the set and volatile figures we can certify.
Continue reading
- Vulcanisation Temperature and Time: The Cure Curve Behind Every Part
- Platinum Versus Peroxide Cure: Speed, Purity and Inhibition
- Medical Grade Silicone: What the Certification Actually Covers
- Food Grade Silicone: Compliance, Cure and Extractables
- Silicone Calendering: Sheet and Coated Fabric in One Pass




 IT
 EN
 ES
 FR
 DE
 PT
 AR
 RU
 JA
 KO
 NL
 TR
 PL
 ID
