

Twenty-three point seven seconds, itemised
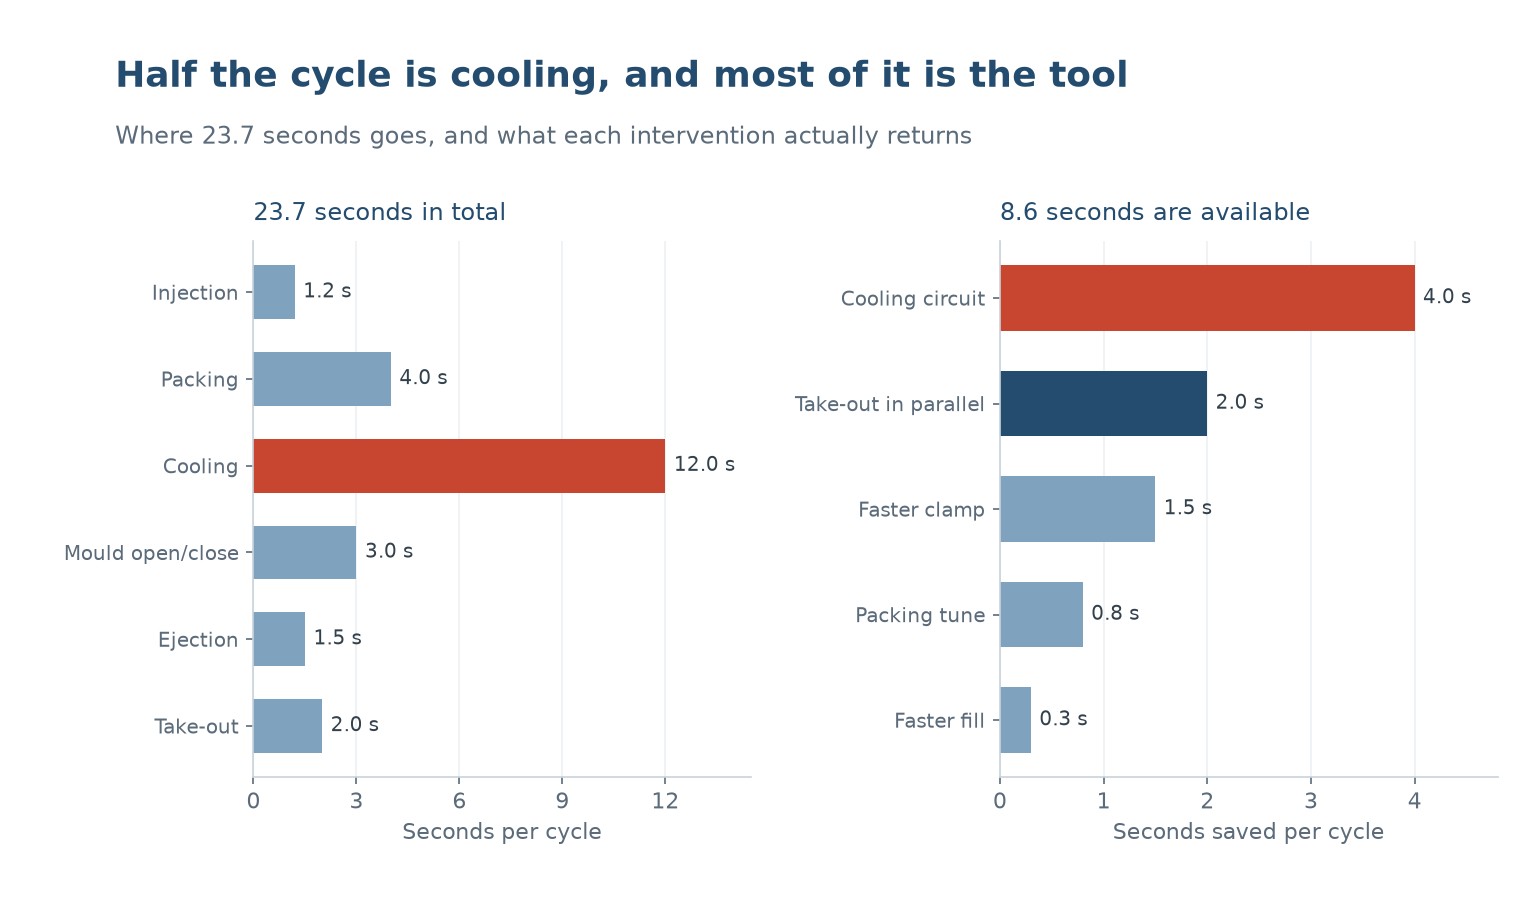
Cycle time arguments are usually won with a stopwatch and lost with a spreadsheet, because the two measure different things. A stopwatch says the cycle is 23.7 seconds. The breakdown says 12.0 of those seconds are cooling, 4.0 are packing, 3.0 are the mould opening and closing, 2.0 are take-out, 1.5 are ejection and 1.2 are injection.
That breakdown changes the whole conversation. Half the cycle is one phase, and that phase is the only one where a change of seconds is available without changing the part. Injection, the phase everyone wants to speed up, is 5 percent of the cycle.
The numbers are for a 2.5 mm wall ABS part on a mid-size machine with a robot. The absolute values move with the part, but the proportions are stubbornly similar across a very wide range of work: cooling is 40 to 60 percent of the cycle on almost everything.
Cooling is where the time is, and it is not the water
Cooling time goes with the square of the wall thickness, so a part with a 4 mm wall takes four times as long to cool as one with a 2 mm wall at the same conditions. That is why wall thickness is a cost decision made at the design stage, and why a 0.5 mm wall reduction is worth more than any process tuning.
After the wall, the limit is heat transfer out of the tool. Four things decide it, and only one of them is the chiller.
- Circuit layout: a circuit that runs at 1.5 diameters from the cavity surface removes heat; one at 4 diameters mostly removes heat from the mould base.
- Flow rate: turbulent flow is required. Below the turbulence threshold the water temperature rise across the circuit hides the problem and the tool runs hot at the far end.
- Baffles and bubblers: a long core pin with a straight-through circuit is cooled at the inlet end and hot at the tip.
- Mould material: a beryllium copper insert conducts three to four times better than steel, which matters on a hot spot but not on a flat wall.
A cooling circuit rebuild on a part like this is worth about 4.0 seconds, which is the largest single item available. It is also the most expensive, because it means pulling the tool out and re-machining water lines.
The cheapest seconds are the ones you overlap
The next largest item is not a speed increase at all, it is a sequence change. On the 23.7 second cycle, 2.0 seconds of take-out happen after the mould opens and before it closes again. Move the take-out to run while the mould is closing, or let the robot enter as soon as the part is clear, and most of those 2.0 seconds disappear without anything moving faster.
The same logic applies to ejection and take-out. If the robot is picking while the ejector is still retracting, the two overlap. If the robot waits for an ejector-forward signal and then for an ejector-back signal, they run in series and the time is additive.
Faster clamping is the third item, worth about 1.5 seconds. A toggle machine with a well-set profile can close and open in 2.2 seconds instead of 3.0 without shock, because the slow-down point is set close to the mould face and the pressure is released before the platens separate.
Packing is a quality phase that happens to cost time
Packing is 4.0 seconds here, and it is the phase where shortening the time is most likely to cost money. Packing holds pressure while the gate freezes and the part is topped up against shrinkage. Cut it too short and the part sinks, warps or shows a dimension that drifts through the run.
There is a right way to shorten it, and it is to find the gate freeze time rather than to guess. Weigh the part at increasing pack times on a series of shots. The weight rises and then plateaus, and the plateau is the gate freeze. Packing beyond that point does nothing except hold the machine.
That measurement typically returns 0.8 seconds on a cycle like this, and it also usually improves the part, because the pack time in the original setting was chosen to be safe rather than to be right.
| Intervention | Seconds returned | Costo | Il rischio |
|---|---|---|---|
| Cooling circuit rebuild | 4.0 | High, tool out of press | Low if designed properly |
| Take-out in parallel | 2.0 | Low, robot program | Basso |
| Faster clamp profile | 1.5 | Low, setting | Medium, watch for shock marks |
| Packing tuned to gate freeze | 0.8 | None | Medium, verify weight and dimension |
| Faster fill | 0.3 | None | High, cosmetic and flow defects |
Table 1 — What each intervention returns, and what it costs to get it
Savings that are not savings
Three changes look like cycle time reductions and are not, and they are the reason so many cycle time projects report a number that never reaches the accounts.
The first is raising the melt temperature to shorten cooling. It works, and it also shortens the thermal window, increases shrinkage, and moves the material closer to degradation. The seconds come back as scrap rate.
The second is opening the mould earlier, before the part is rigid enough. The part ejects with a slight warp that is inside tolerance at first and drifts as the tool wears. The cycle time is genuinely lower and the reject rate is genuinely higher.
The third is running a thinner wall on a part that was designed thicker. This is a real saving, often the largest available, but it is a design change and it has to be qualified as one: stiffness, impact and the assembly interface all move.
| Change | Tempo di ciclo | What it costs |
|---|---|---|
| Melt temperature up 15 C | 1.5 s shorter | Higher shrinkage, wider scatter, less thermal headroom |
| Mould opens 0.5 s earlier | 0.5 s shorter | Ejection warp that drifts as the tool wears |
| Wall reduced by 0.3 mm | 3.0 s shorter | Stiffness, impact strength, assembly fit |
| Fill time halved | 0.3 s shorter | Shear, flash risk, cosmetic defects at the gate |
| Packing cut below gate freeze | 0.8 s shorter | Sink, warpage, dimension that drifts through the run |
Table 2 — Changes that shorten the cycle and move the cost somewhere else
How to measure before changing anything
The measurement is a phase breakdown, not a cycle time. Most machines log it, and where they do not, a camera at 30 frames per second and a stopwatch on the playback gets within 0.1 seconds on every phase.
- Log every phase separately for 30 consecutive cycles, not one.
- Separate the machine's own movements from the robot's, since overlap is where the free seconds are.
- Measure the water temperature rise across each circuit, which shows whether the flow is turbulent.
- Weigh ten parts at increasing pack times to find the gate freeze.
- Then rank the interventions by seconds returned per euro, and do them in that order.
On the cycle in the chart the ranking is unambiguous: the cooling circuit is the big item, parallel take-out is the cheap item, and faster fill is last. Doing them in the order they appear on the machine screen instead of the order in the ranking is how a project spends three weeks to save 0.3 seconds.
What percentage of an injection moulding cycle is cooling?
Usually 40 to 60 percent. On the example here it is 12.0 of 23.7 seconds, and cooling time goes with the square of wall thickness.
How much time can a cooling circuit rebuild save?
About 4 seconds on a cycle like this, which is the largest single item available. It is also the most expensive, because the tool has to come out.
Why is faster injection the wrong first move?
Injection is about 5 percent of the cycle. Doubling the fill speed returns a fraction of a second and adds shear, flash and cosmetic risk.
What is the cheapest way to save cycle time?
Overlap the robot take-out with the mould closing, and set the clamp profile properly. Together they are worth about 3.5 seconds for a program change.
How do I find the right packing time?
Weigh parts at increasing pack times. The weight plateaus when the gate freezes, and packing beyond that point costs time and buys nothing.
Is a shorter cycle always cheaper?
No. Raising melt temperature or opening early moves the cost into scrap and rework. Count the reject rate in the saving.
A cycle that has to come down without the scrap going up?
Send the phase breakdown, the wall thickness and the tool layout. We will tell you where the seconds actually are and what each one costs to get.
Continue reading
- Cooling Time: Three Times the Wall Is Nine Times the Wait
- Mould Temperature Control: The Circuit Layout Matters More Than the Chiller
- Screw Cushion and Decompression: The Two Numbers That Explain Inconsistent Parts
- Clamp Force: You Cannot Size a Tonnage From a Table
- Custom Injection Moulding: Tooling, Materials and Tolerances




 IT
 EN
 ES
 FR
 DE
 PT
 AR
 RU
 JA
 KO
 NL
 TR
 PL
 ID
