
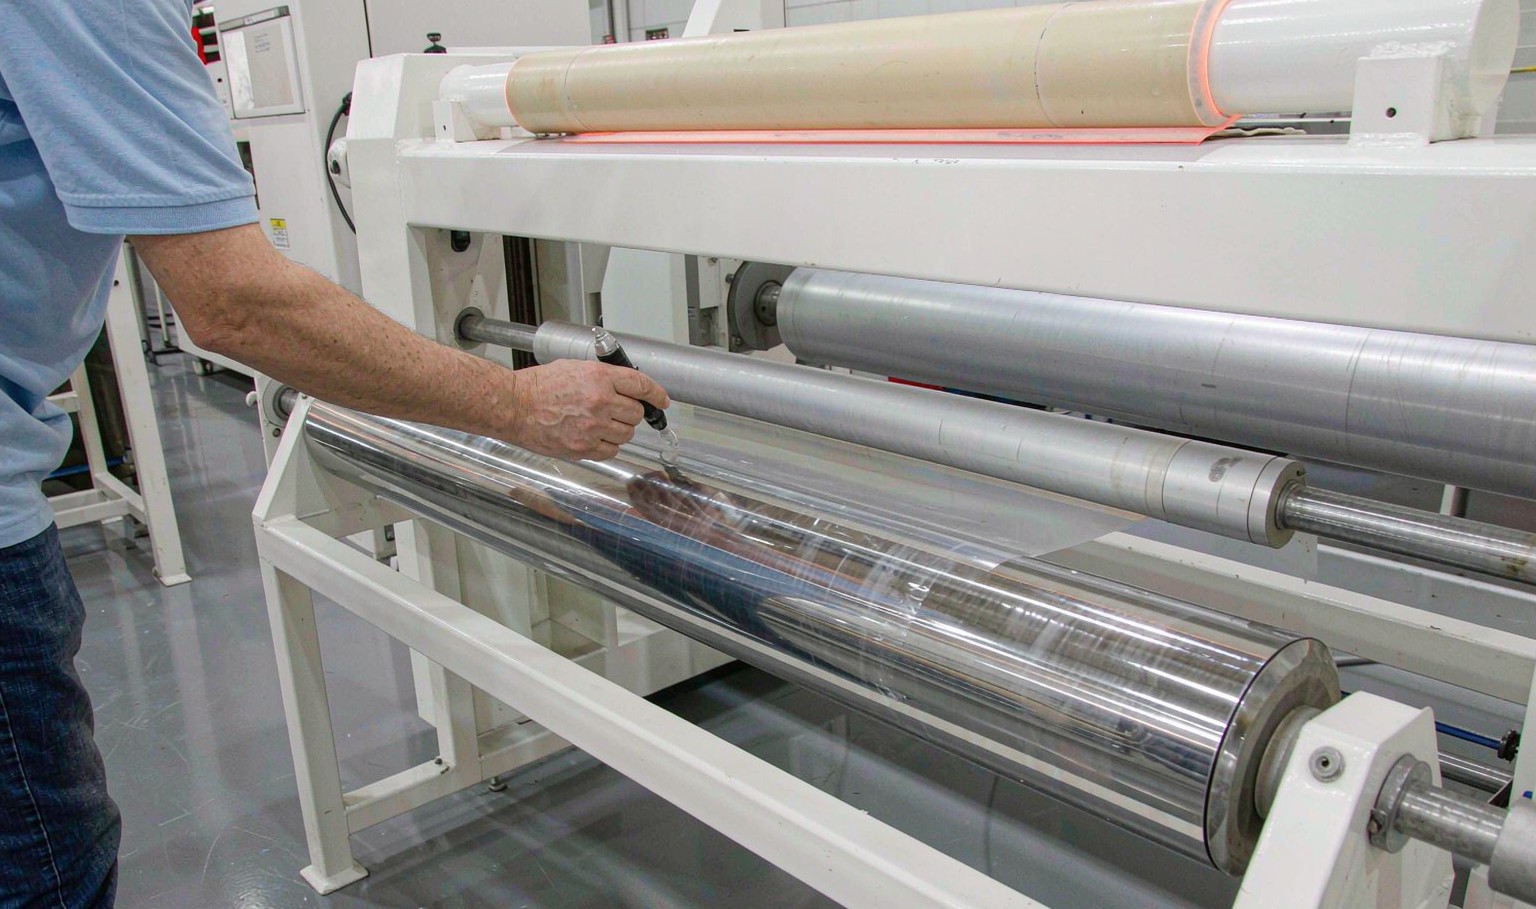
Corona changes the surface, not the sheet
Polyolefins have a low surface energy, which is another way of saying that ink and adhesive do not want to stick to them. Corona treatment raises the surface energy by oxidising the top few nanometres of the surface, creating polar groups that ink and adhesive can bond to.
The bulk of the sheet is untouched. That is the point: the treatment changes wettability without changing mechanical properties, and it is why a treated sheet can be printed and a untreated one cannot, from the same roll of polymer.
Surface energy is measured in dynes per centimetre, or equivalently in millinewtons per metre, and it is tested with a set of pens of known surface tension. A pen that wets the surface and holds its line indicates the sheet's energy is at least that value; a pen that beads up indicates it is below.
The treatment decays, and the decay sets the shelf life
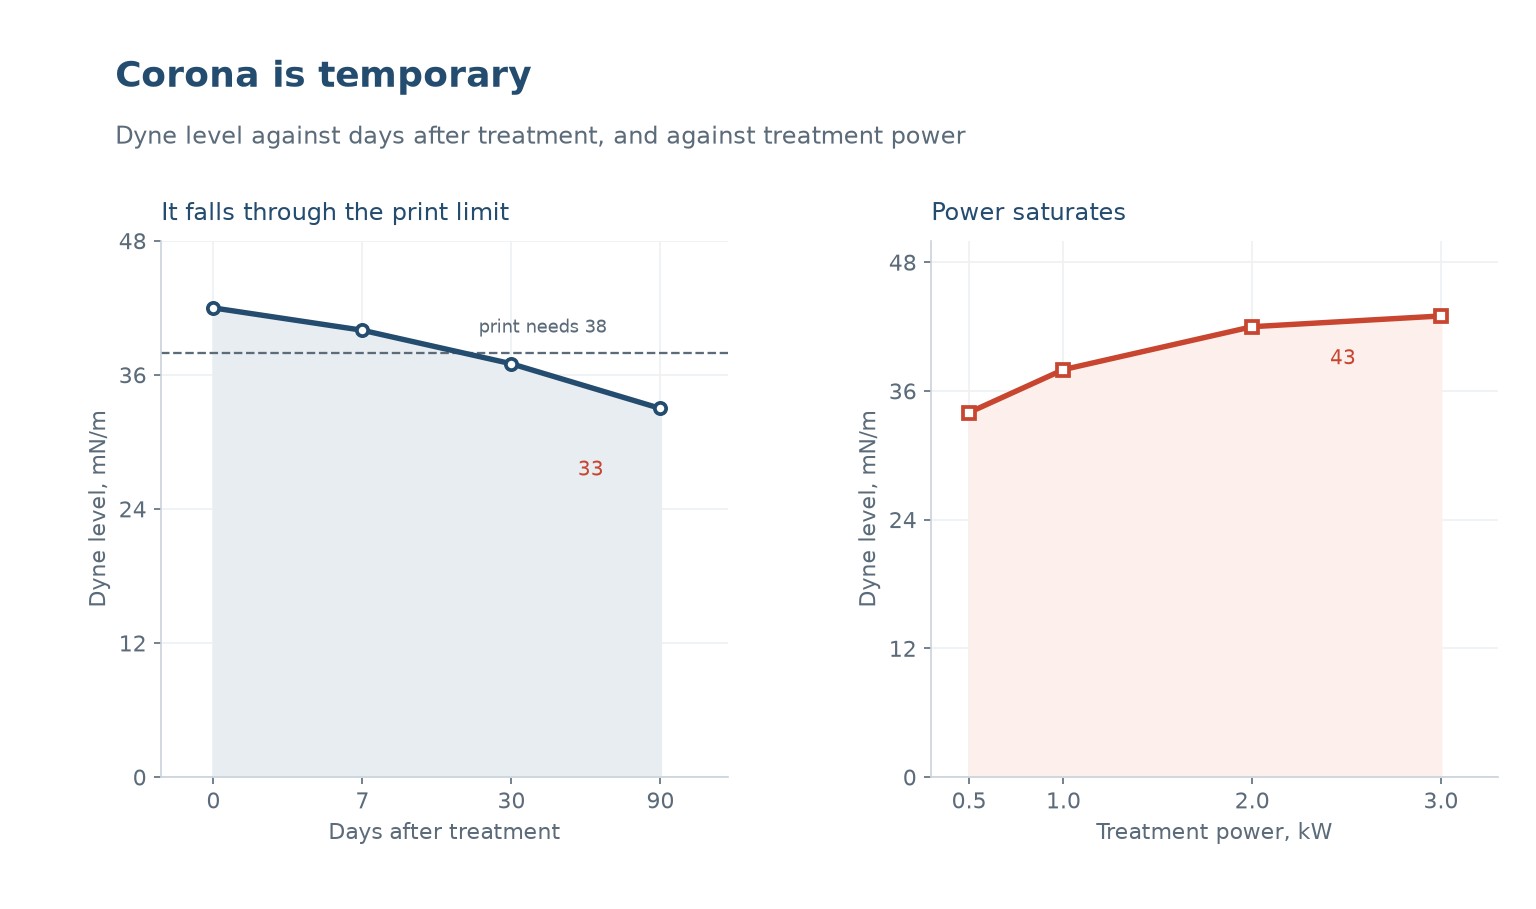
A freshly treated sheet measures about 42 dyn/cm. After a week it is 40, after a month 37, after three months 33. The decay is caused by the polar groups migrating into the bulk and by contamination from the air, and it happens whether the sheet is used or not.
Most solvent and water-based inks need about 38 dyn/cm to wet and adhere, so a sheet that starts at 42 is above the requirement for about a month and below it after three. That is the real shelf life of a treated sheet, and it is shorter than most people assume.
The practical consequence is that treatment and printing should be as close together as the process allows. A converter who treats, stores for two months and then prints is printing on a surface that has lost most of its advantage, and the failure shows up as poor adhesion that cannot be reproduced.
More power helps, up to a point
Treatment power raises the dyne level, and it saturates. At 0.5 kW the sheet reaches 34 dyn/cm, at 1.0 kW 38, at 2.0 kW 42 and at 3.0 kW 43. Doubling from 1.0 to 2.0 buys four dynes; doubling again buys one.
The saturation is why over-treating is a real risk. Beyond the point where the surface is fully oxidised, more energy starts to degrade the surface layer, which produces a low-molecular-weight residue that is weakly bound and actually reduces adhesion. A sheet that is over-treated can fail a tape test worse than one that is correctly treated.
Over-treatment also causes blocking, where the treated surfaces stick to each other in a stack, and it can produce a visible haze on a clear sheet. Both are signs that the power is above the useful range.
Line speed is the real control
The dose a sheet receives is power divided by line speed, so a line running at twice the speed with the same power delivers half the treatment. This is why a treatment setting that worked at one speed produces a sheet that fails at another, and why the setting should be recorded as a dose rather than as a power.
The practical approach is to set the power for the fastest speed the line will run and to verify the dyne level at that speed. A slower run then over-treats, which is a smaller risk than under-treating but is still a risk, and the fix is to trim the power with the speed.
The electrode gap and the condition of the electrode also matter. A worn or contaminated electrode delivers less treatment for the same power, and the symptom is a dyne level that drifts down over months without any change in settings.
| Kontrolle | Effect | Typical failure |
|---|---|---|
| Power | Raises dyne, saturates | Over-treatment, blocking |
| Line speed | Sets the dose | Drift when speed changes |
| Electrode gap | Sets the field | Worn electrode, low dyne |
| Electrode cleanliness | Uniformity | Patchy treatment |
| Sheet temperature | Minor | Condensation on cold sheet |
Table 1 — The five controls on a corona station
Measuring it so it means something
A dyne pen test is quick and it is a pass or fail at one value, which is often what is needed. A dyne test with a set of pens gives a range, which is more useful because it shows how far above the requirement the sheet is.
The measurement should be taken across the width and along the length, because treatment can be uneven. An electrode with a damaged section gives a strip of low dyne level down the sheet, and a single test in the middle will miss it.
For critical work, a tape test or a peel test after printing is the real measure. Dyne level correlates with adhesion but does not guarantee it, because adhesion also depends on the ink, the drying and the dwell.
| Dyne level | What it supports | Where you see it |
|---|---|---|
| Under 32 | Nothing adheres reliably | Untreated polyolefin |
| 33-35 | Poor solvent ink adhesion | Treated, stored three months |
| 36-38 | Marginal for water-based ink | Treated, stored one month |
| 38-42 | Good for solvent and water ink | Freshly treated |
| 42-46 | UV ink, laminating adhesive | High power, fresh |
| Over 46 | Over-treated, weak boundary | Power too high |
Table 2 — Dyne level against what the surface will actually take
Where corona is not enough
Corona treatment is a line-of-sight process on a flat surface. It does not treat the inside of a tube, the underside of a rim or a deep recess, and a sheet that will be formed into a deep part will have untreated areas where it was stretched.
It also does not survive thermoforming. The surface is stretched during forming, which thins the treated layer, and the heat relaxes the polar groups. A printed-and-formed part needs the printing after forming, or a treatment that survives the process, which corona does not.
And it does not fix a contaminated surface. A sheet with silicone oil or mould release on it will not accept treatment, because the corona acts on the polymer and not on the contamination. Cleaning before treatment is part of the process.
What dyne level does printing need?
Most solvent and water-based inks need about 38 dyn/cm. UV inks and some laminating adhesives need more, often 40 to 42, and the ink supplier's figure should be used rather than a general rule.
How long does corona treatment last?
About a month above 38 dyn/cm on a typical polyolefin, and three months to fall to 33. The decay is faster in warm, dusty conditions and slower on a well-wrapped roll.
Can over-treatment reduce adhesion?
Yes. Past the saturation point the surface layer degrades into a weakly bound residue, and a tape test can fail worse than on a correctly treated sheet. Blocking and haze are the visible signs.
Does corona treatment work on PVC?
It does, though PVC already has a higher surface energy than a polyolefin and needs less treatment. The same principles apply: measure, and do not over-treat.
Does the treatment survive thermoforming?
Not usefully. The surface is stretched and heated, which thins the treated layer and relaxes the polar groups. Print after forming rather than before.
Why is my treatment uneven across the width?
Usually a worn or contaminated electrode, or a gap that is not parallel. A strip of low dyne level down the sheet points at the electrode rather than at the power setting.
Sheet that has to take print or adhesive?
Send the sheet specification and the downstream process. We will tell you what dyne level is needed, whether it survives the process, and how the sheet should be stored.




 DE
 EN
 ES
 FR
 PT
 AR
 RU
 JA
 KO
 IT
 NL
 TR
 PL
 ID
